This is a technical decision hub built from hypothetical drawing-based cases; it does not claim confidential customer work or verified production statistics.
English: Nickel Alloy CNC Tooling Hub: Select Carbide Tools by Alloy, Feature and Failure Mode
This nickel alloy CNC tooling hub is a decision path, not a universal speed-and-feed chart. Start with alloy condition, then the drawing feature, tool access and the failure that would invalidate the part. Inconel 718 may drive notch wear at a stable depth-of-cut line; Hastelloy can combine low thermal conductivity with work hardening; Monel often adds adhesion and burr risk; Incoloy grid plates create accumulated positional and distortion error. The same coating label cannot solve all four.
1. Identify the alloy and heat-treatment condition
Record the exact grade, solution or age condition, casting/forging route and skin to remove. Treat Inconel 718, 625, 600 and X-750 as different cutting systems. A forged skin or interrupted scale calls for a stronger edge than a final sealing seat. Monel K-500 after age hardening is not interchangeable with annealed Monel 400. If material certification is unclear, stop before choosing a parameter window.
2. Convert drawing features into separate tool jobs
Separate open pocket, full slot, deep bore, angled jet hole, knife-edge seat, thin ring, groove and vane passage. Open roughing rewards constant radial engagement; a deep bore needs guided entry, coolant and a measurable chip-return route; a knife edge needs its own sharp finishing tool; a thin ring needs balanced stock and low radial force. One long general-purpose end mill is rejected because it compromises reach, stiffness and edge condition everywhere.
Feature-to-tool decision matrix
| Drawing feature | Tool, geometry and holder | Decision / rejection |
|---|---|---|
| Open pocket / scallop | 10–12 mm, 4–5 flute variable-helix radius carbide; PVD; shrink-fit | Constant radial engagement; reject full-width six-flute roughing |
| Deep bore / thermowell | Short pilot drill, through-coolant carbide drill or guided system, damped finish bar | Prove chip return and axis; reject unguided long drill |
| Angled micro hole / oil jet | Stub micrograin carbide drill, guide pad where needed, reverse chamfer | Position and breakout burr; reject hand picking |
| Knife-edge or seal seat | Dedicated sharp positive carbide form/finish tool in low-runout holder | Protect form and finish; reject worn roughing edge |
| Thin ring and groove | Ground carbide groover plus balanced low-force finish tool | Control distortion after release |
| Vane or narrow window | Tapered/relieved-neck carbide end mill with only required reach | Access without global overhang |
3. Select edge preparation, coating and holder
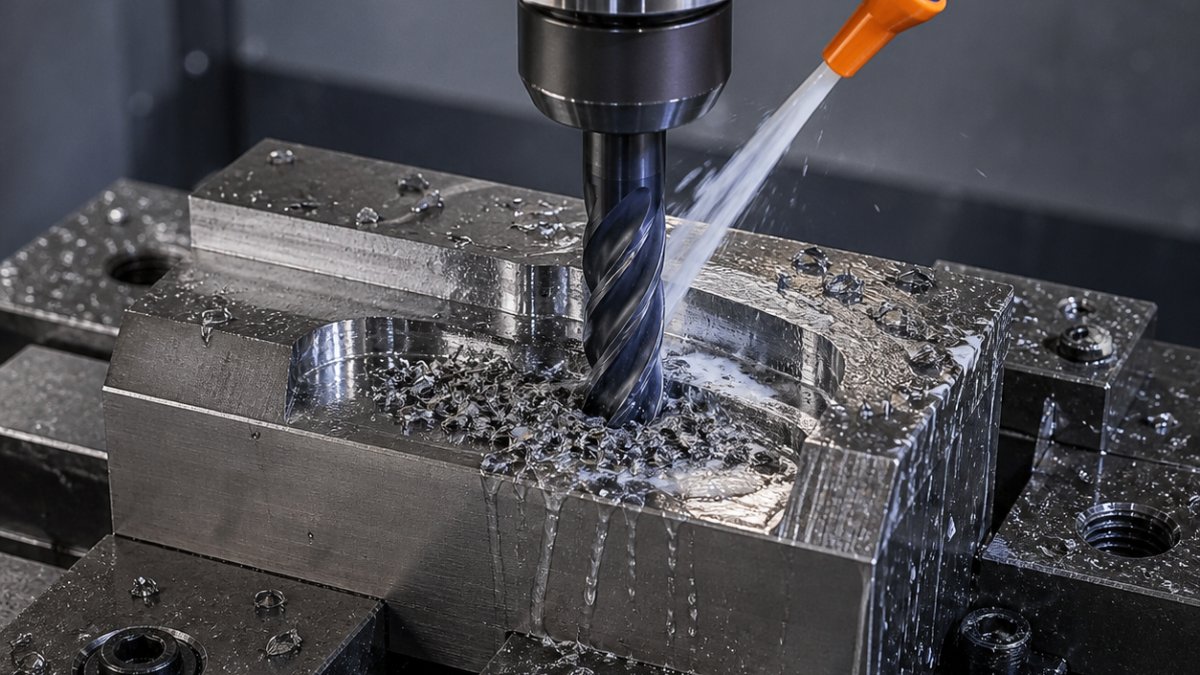
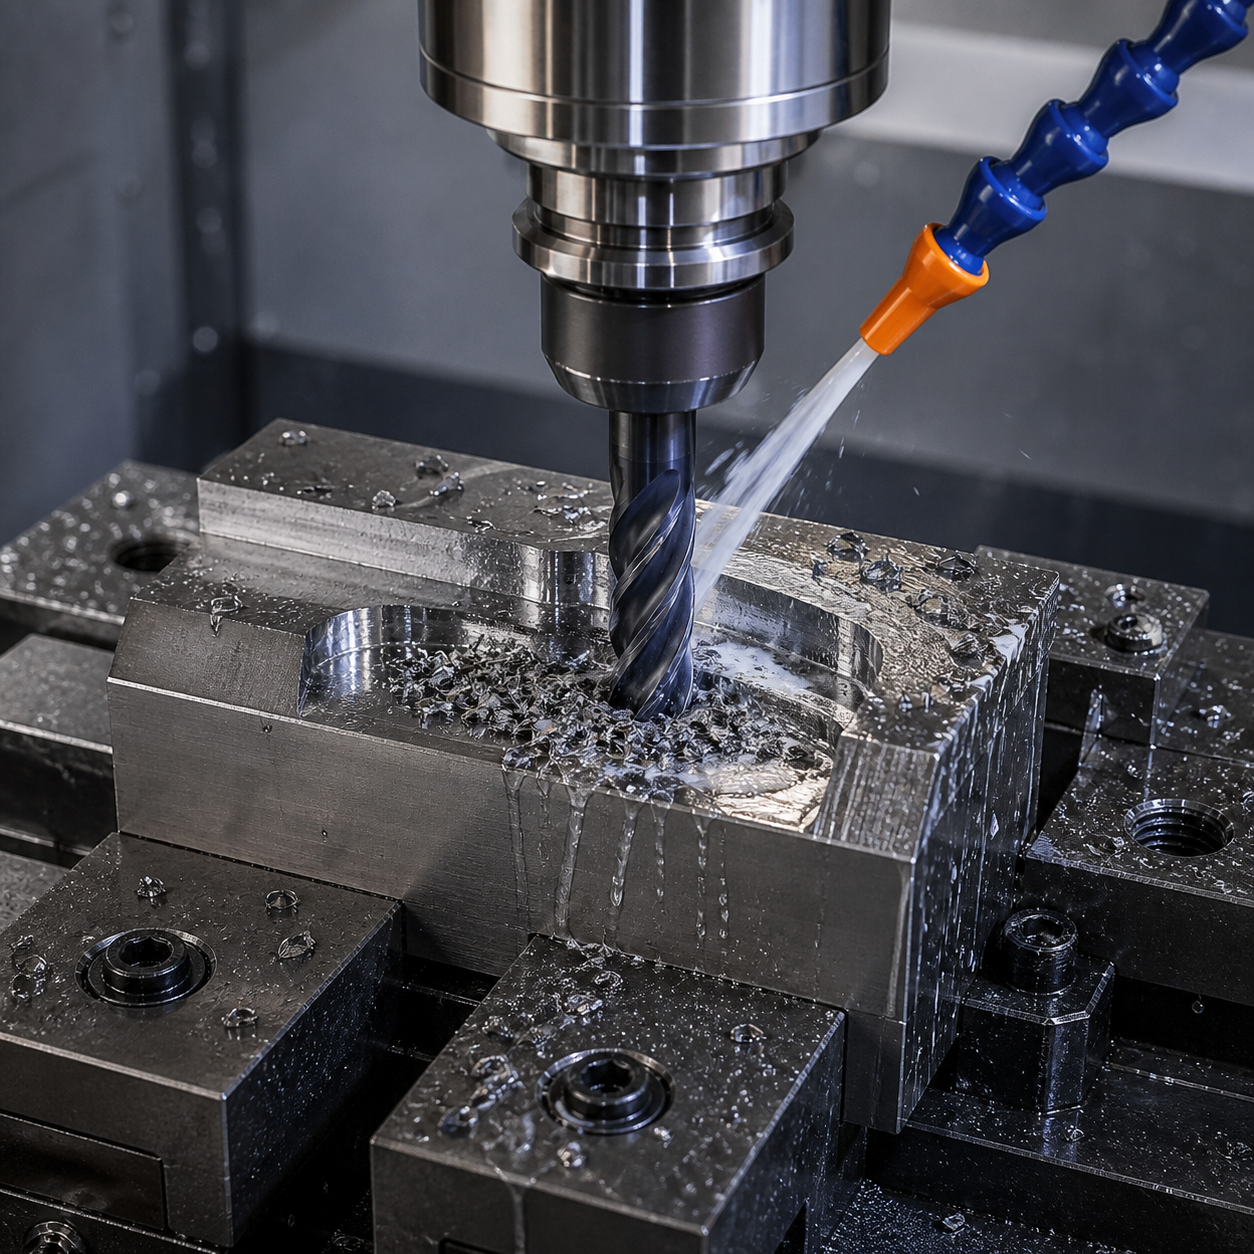
For adaptive pocketing, use a 10–12 mm four- or five-flute variable-helix micrograin carbide radius end mill with a heat-resistant AlTiN/AlCrN-family PVD layer and controlled hone. Use four flutes when chip space is tight and five when radial engagement is low. Finish sealing walls with a dedicated sharp positive tool. Choose short through-coolant carbide drills for holes, damped boring bars for deep IDs, full-profile inserts for critical threads, and ground carbide grooving tools for narrow seal grooves. Shrink-fit or hydraulic holders must be selected from reach and runout, not fashion.
4. Plan coolant, chip exit and tool-life gates
Do not reduce feed until the edge rubs. Maintain chip thickness through arcs, roll into corners and avoid dwelling at shoulders. Deliver coolant to the active edge and prove that chips leave a blind bore; pecking without return evidence only reheats one band. Tool-life triggers should combine notch depth, flank wear, spindle-load trend, diameter compensation and surface texture. Scheduled replacement is appropriate only after those signals establish a stable distribution.
5. Inspect by the failure the feature can create
Inspect from the datum chain. Deep bores need diameter, straightness and internal surface evidence; angled holes require position, breakthrough and burr inspection; sealing seats require form, runout and texture; thin rings require released-state roundness and flatness; vane passages require profile and minimum wall. Borescope and replica methods can reveal inaccessible damage, but they do not replace dimensional measurements.
Case paths by drawing risk
Choose by hole and flow feature: Inconel 600 Thermowell CNC Tool Selection for Deep Bore, Tapered Stem and Bleed Hole; Inconel 625 Heat Exchanger Header Plug CNC Tool Selection for Blind Seal Seat and Telltale Hole; Inconel 718 Turbine Oil Nozzle Ring CNC Tool Selection for Angled Jet Holes and Scalloped Pockets; Hastelloy C-276 Mixing Nozzle CNC Case: Compound-Angle Holes and Burr Control.
Choose by sealing seat and groove: Hastelloy B-3 Rupture Disc Holder CNC Tool Selection for Knife-Edge Seat and Vent Groove; Monel 400 Subsea Cable Penetrator CNC Tool Selection for Seal Grooves and Angled Leak Port; Hastelloy C-276 Diaphragm Pump Valve Plate CNC Tool Selection for Spiral Purge Slot and Knife-Edge Seat; Inconel 718 Seal Ring CNC Turning Case: Thin-Wall Grooves, Distortion and Tool-Life Control.
Choose by thin section and interrupted access: Hastelloy X Combustor Swirl Cup CNC Tool Selection for Angled Vane Windows and Thin Exit Lip; Inconel X-750 Turbine Brush Seal Carrier CNC Tool Selection for Angled Pack Slot and Pilot Bore; Inconel 718 Turbine Seal Ring: CNC Tooling and Distortion Control; Incoloy 800H Tube-Support Grid CNC Tooling for Bore Array and Expansion Slots.
Choose by five-axis passage or fork geometry: Monel K-500 Closed Impeller CNC Case: Five-Axis Vane Passages and Tool-Life Control; Monel K-500 Marine Clevis CNC Tool Selection for Fork Slot, Pin Bore and Fillet Relief.
FAQ
Which coating is best for nickel alloys? No coating wins by itself. Match a heat-resistant PVD coating to carbide grade, edge hone, engagement and coolant delivery.
Why does notch wear appear at one line? A fixed axial depth repeatedly exposes the same edge region to work-hardened material and thermal cycling; vary depth only when the drawing and stability allow it.
Should a worn rougher make the finish pass? No. A dedicated finishing edge gives a traceable surface and avoids transferring notch damage to a sealing feature.
Use the linked cases as bounded examples. Copy the decision logic—datum, feature, access, failure and inspection—not a parameter number detached from machine rigidity, holder, coolant and material condition.


