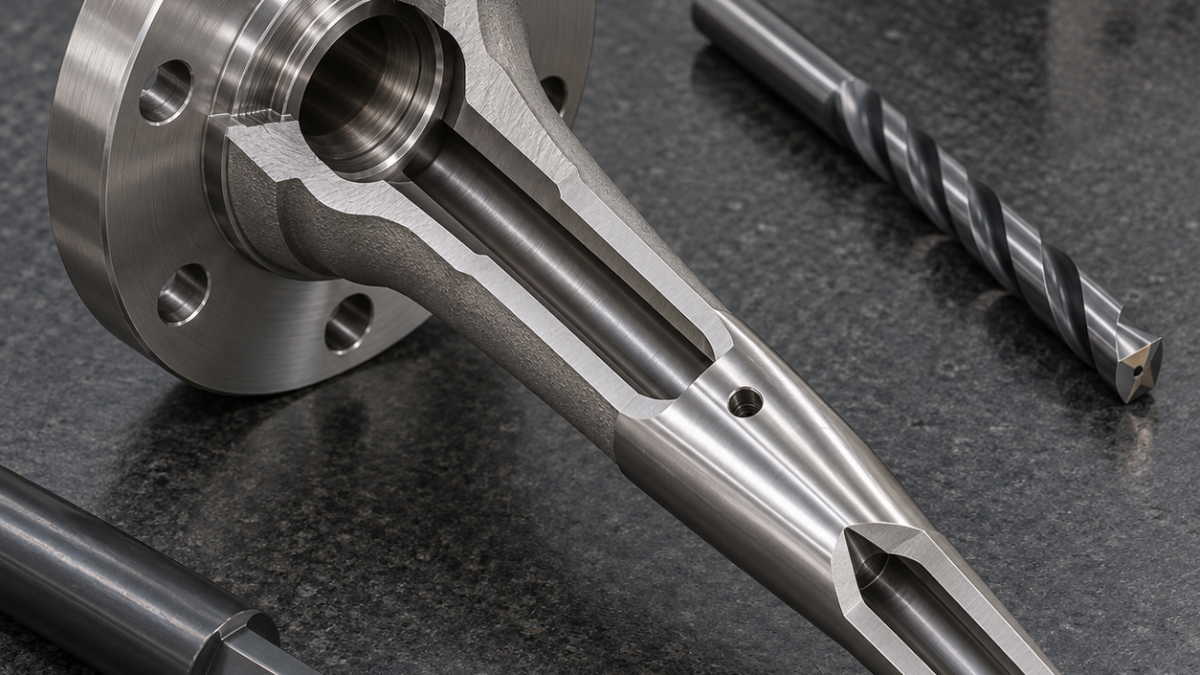
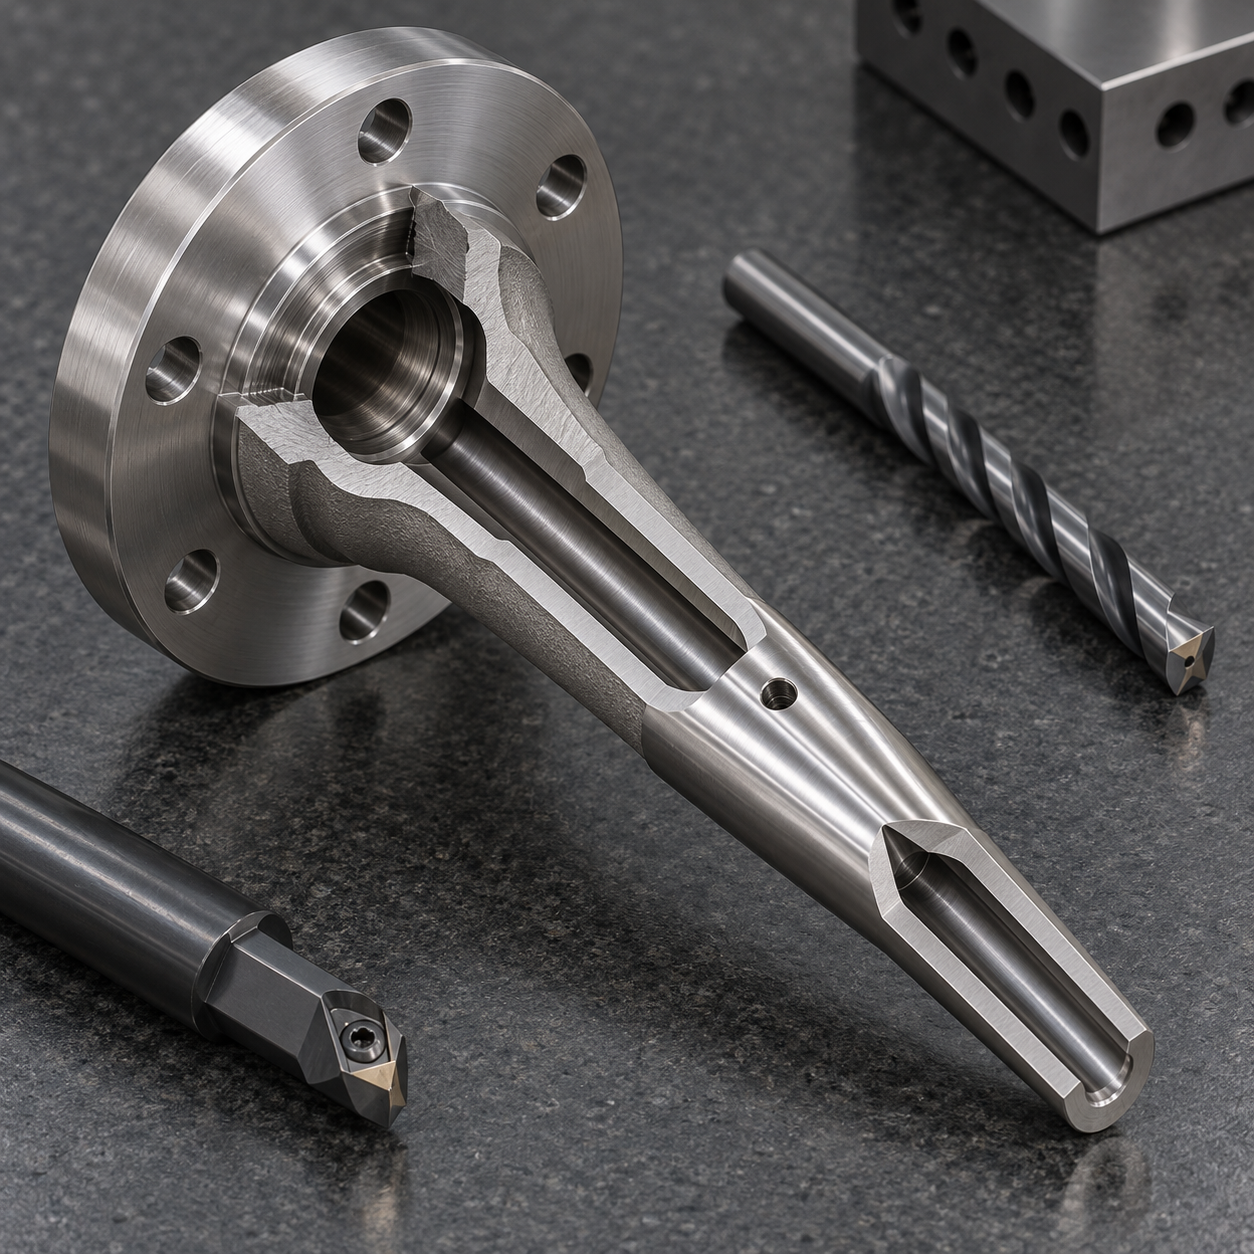
English: Inconel 600 Thermowell Tooling for a Deep Bore, Tapered Stem and Bleed Hole
The search problem is not simply how to drill Inconel 600. The drawing ties a long internal bore to the flange pilot, while wall thickness after taper turning must remain uniform and a small bleed hole must break into the bore without a retained burr. The safest plan establishes the pressure boundary from one rotational datum and postpones the cross hole until bore size and runout are known.
Read the pressure boundary before choosing the drill
Grip the forged blank on a soft-jaw pilot, face the flange and rough the outside diameter. Spot with a short 140-degree carbide drill, open a pilot, then use a through-coolant single-lip carbide gun drill sized below finish diameter. A damped micro boring bar corrects the mouth and establishes the inspection reference; the gun drill is not asked to create the final seal-related concentricity by itself.
Feature-to-tool decisions for the thermowell
| Drawing feature | Carbide tool and holder | Selection logic / rejected alternative |
|---|---|---|
| Flange datum and seal face | CNMG rougher, then sharp CCGT wiper in rigid capto holder | Separates scale removal from the low-feed seal finish; one roughing insert would smear the land. |
| Pilot and 14xD internal bore | 140-degree carbide pilot drill; single-lip through-coolant carbide gun drill | Pilot controls entry and gun drill evacuates chips; a long standard twist drill can wander and recut chips. |
| Bore mouth and transition | 6 mm damped carbide boring bar, TiAlN grade, minimum reach | Corrects mouth size and blends the transition; a reamer follows rather than repairs a drifting hole. |
| Tapered thin stem | Positive PVD-coated carbide turning insert, small nose radius | Controls radial load and work hardening; a broad wiper can deflect the stem. |
| Bleed hole and internal edge | 2 mm short carbide drill plus miniature reverse chamfer tool | Creates a measurable break at the intersection; hand picking cannot guarantee a pressure-clean edge. |
Deep bore sequence and datum transfer
Turn the taper with a tough PVD-coated carbide grade and a small honed edge, maintaining a continuous feed through the hot zone. A polished sharp insert looks attractive but chips at scale interruptions; a heavy negative insert raises radial force and can move the thin stem. High-pressure coolant must reach the cutting edge, and the gun-drill cycle must retract before chips pack rather than dwell and glaze the bore.
Heat, work hardening and chip control
After stress and temperature have stabilized, indicate the flange pilot and compare bore runout at the mouth and depth. Air gauging or a calibrated bore probe confirms taper; ultrasonic wall mapping checks minimum wall at clocked positions. Only then cross-drill the bleed hole with a short AlTiN micro drill and remove the internal feather using controlled abrasive flow or a back-chamfer tool whose reach is proven on a witness coupon.
Related tooling comparisons: deep nickel-alloy port tooling; compound-angle probe features.
FAQ for Inconel thermowell machining
Why not start with a twist drill at full depth? Its wandering and chip congestion consume the wall-thickness allowance. Which feature sets the final axis? The flange pilot and seal face establish the functional axis, not the raw forging. When is the gun drill replaced? When thrust, diameter trend or chip form changes before surface tearing appears.
For alloy-first comparison across pockets, holes, seats, grooves and thin sections, use the nickel-alloy CNC tooling decision hub.


