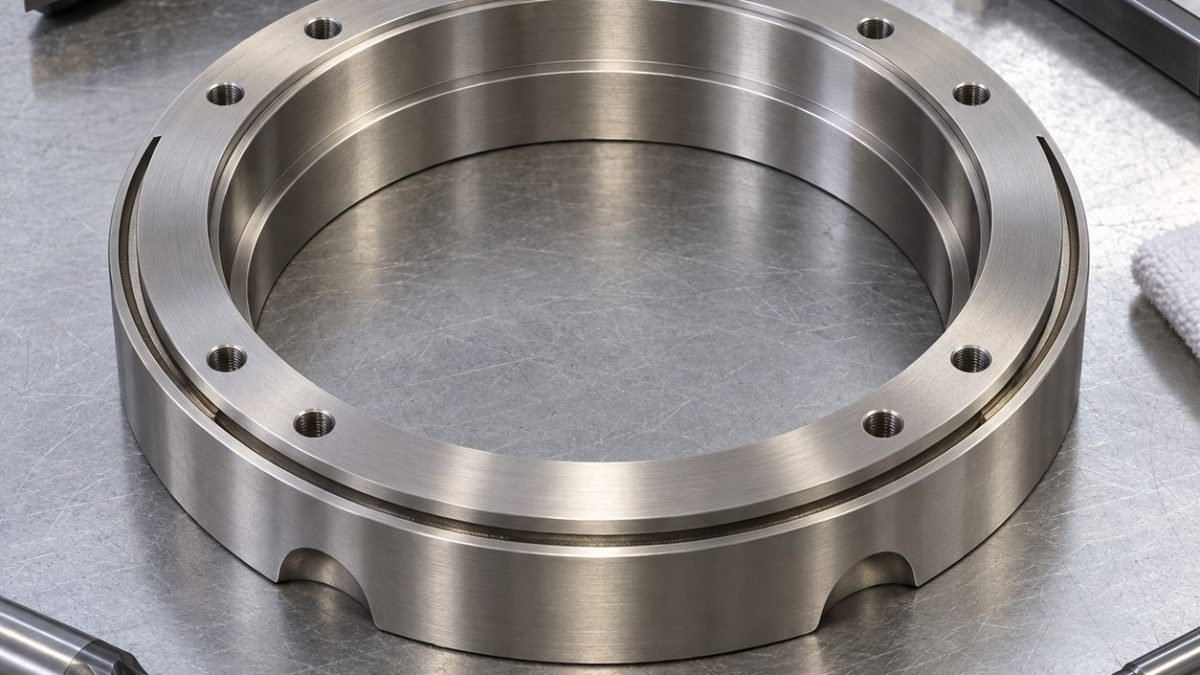
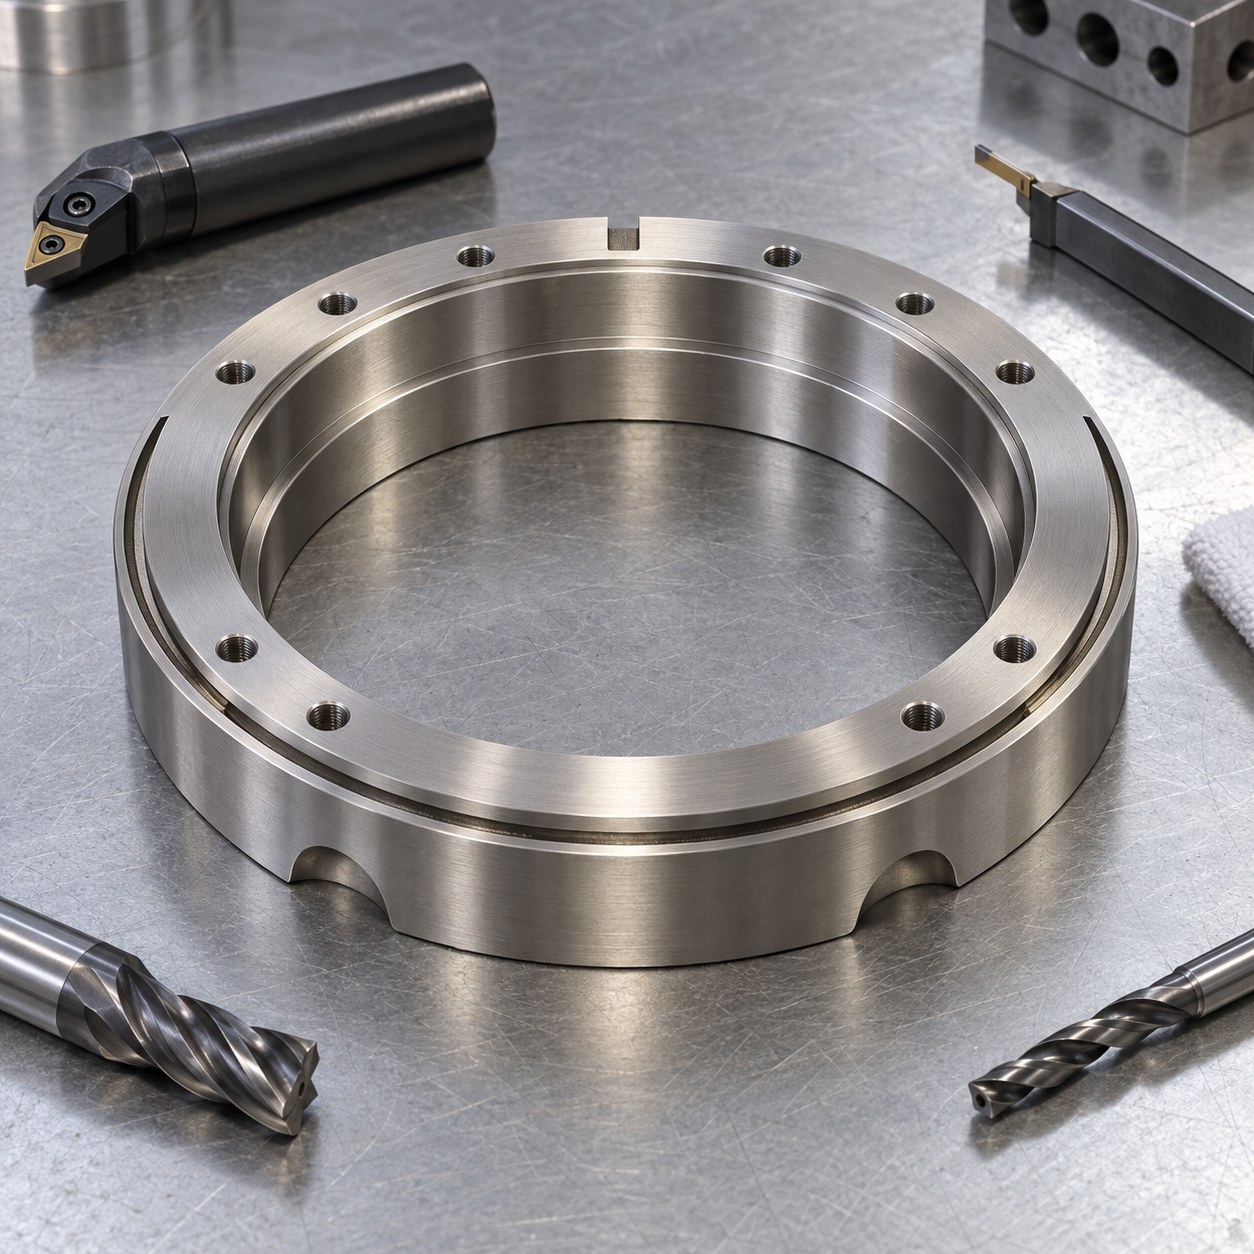
English: Inconel X-750 Brush Seal Carrier Tooling for Angled Slot and Bore
The difficult feature is a narrow slot angled to the carrier face while its floor must remain concentric with a stepped pilot bore. The hypothetical drawing uses the rear face and pilot axis as A-B; a clocking notch sets slot start. Drain scallops are clearance features, not datums.
Create the pilot before tilting the slot
Face and bore the ring on broad segmented jaws, leaving equal radial stock. Finish the stepped pilot in one spindle grip, then move to a trunnion fixture located from A-B and the clocking notch. Rough the angled slot in shallow alternating arcs, finish drain scallops and bolt holes, release for roundness check, then take one light slot-floor pass at the verified angle.
Control radial force on a narrow ring
X-750 hardens under rubbing and notches a groove blade at constant depth. Keep feed active through slot entry, direct coolant into the narrow chip path and index or replace the blade before the floor turns shiny. Ring springback is a fixture problem before it is an offset problem.
Manage notch wear in X-750
| Drawing feature | Carbide tool and holder | Why selected / alternative rejected |
|---|---|---|
| Rear face and pilot bore | Indexable carbide drill then short anti-vibration boring bar with tough PVD insert, Capto holder | One grip preserves axis; separate reamers can follow different stock. |
| Stepped bore finish | 0.4 mm-radius PVD wiper insert with controlled light depth | Stable finish without rubbing; repeated spring passes work-harden X-750. |
| Angled brush-pack slot | 1.2 mm PVD carbide groover with reinforced blade, 0.04 mm hone, minimum reach | Narrow positive edge limits radial force; a full-profile wide tool chatters. |
| Clocking notch and scallops | 4 mm 4-flute AlTiN radius end mill, shrink holder | Ramp entry controls cast-skin interruption; a slitting saw leaves a hidden lip. |
| Bolt arc and edge breaks | Carbide spot drill, coolant-through drills and single-flute chamfer mill | Common rotary datum holds clocking; hand deburring risks the slot mouth. |
Verify slot floor after release
Measure released pilot roundness and face runout before mapping slot angle, width and floor radius around the circumference. Inspect notch and scallop exits under magnification and verify bolt clocking from the slot start. Brush-pack retention, thermal growth and engine performance require separate assembly validation.
Practical tooling FAQ
Why finish the pilot before tilting the slot?
The pilot supplies the rotary center used to generate a constant slot radius and angle.
Why avoid spring passes in X-750?
A rubbing pass can harden the floor without removing useful stock, accelerating notch wear.
seal-groove and keyway tooling · superalloy interrupted-hole choices


