Related tooling references: Invar 36 Optical Spacer Frame CNC Tool Selection for Flexure Slots and Kinematic Pads and 410 Stainless Pump Impeller CNC Tool Selection for Thin Blades, Shroud Lip and Balance Pads.
English: Monel K-500 Marine Clevis Tooling for Fork Slot and Pin Bore
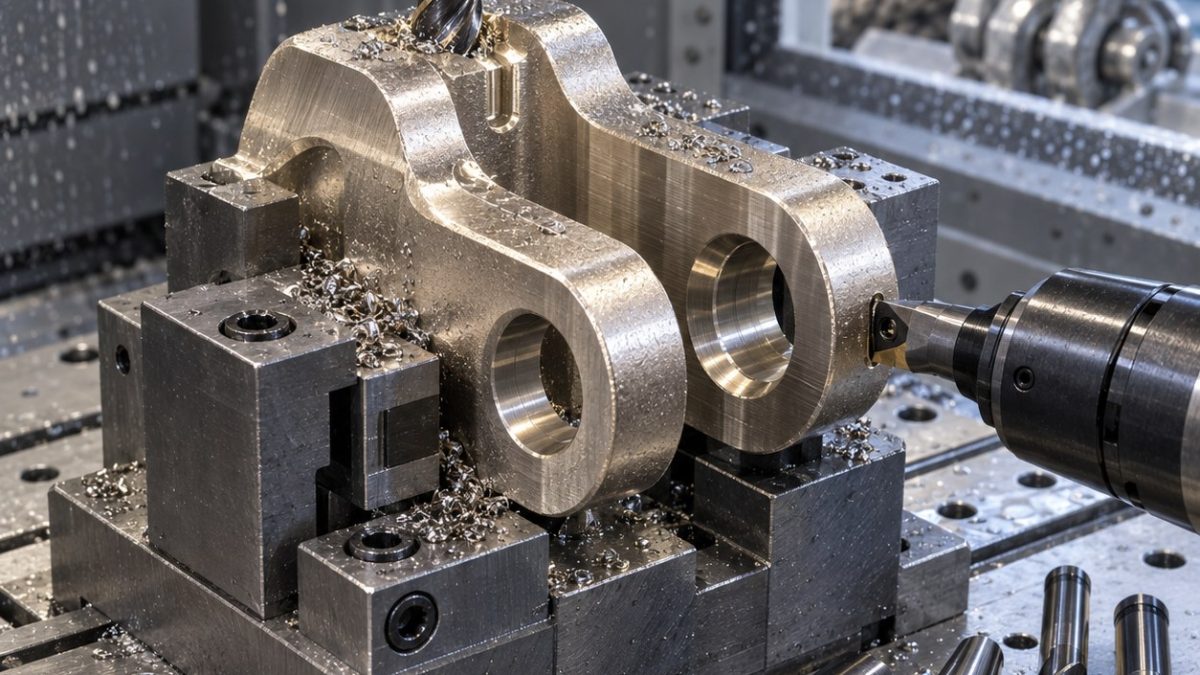
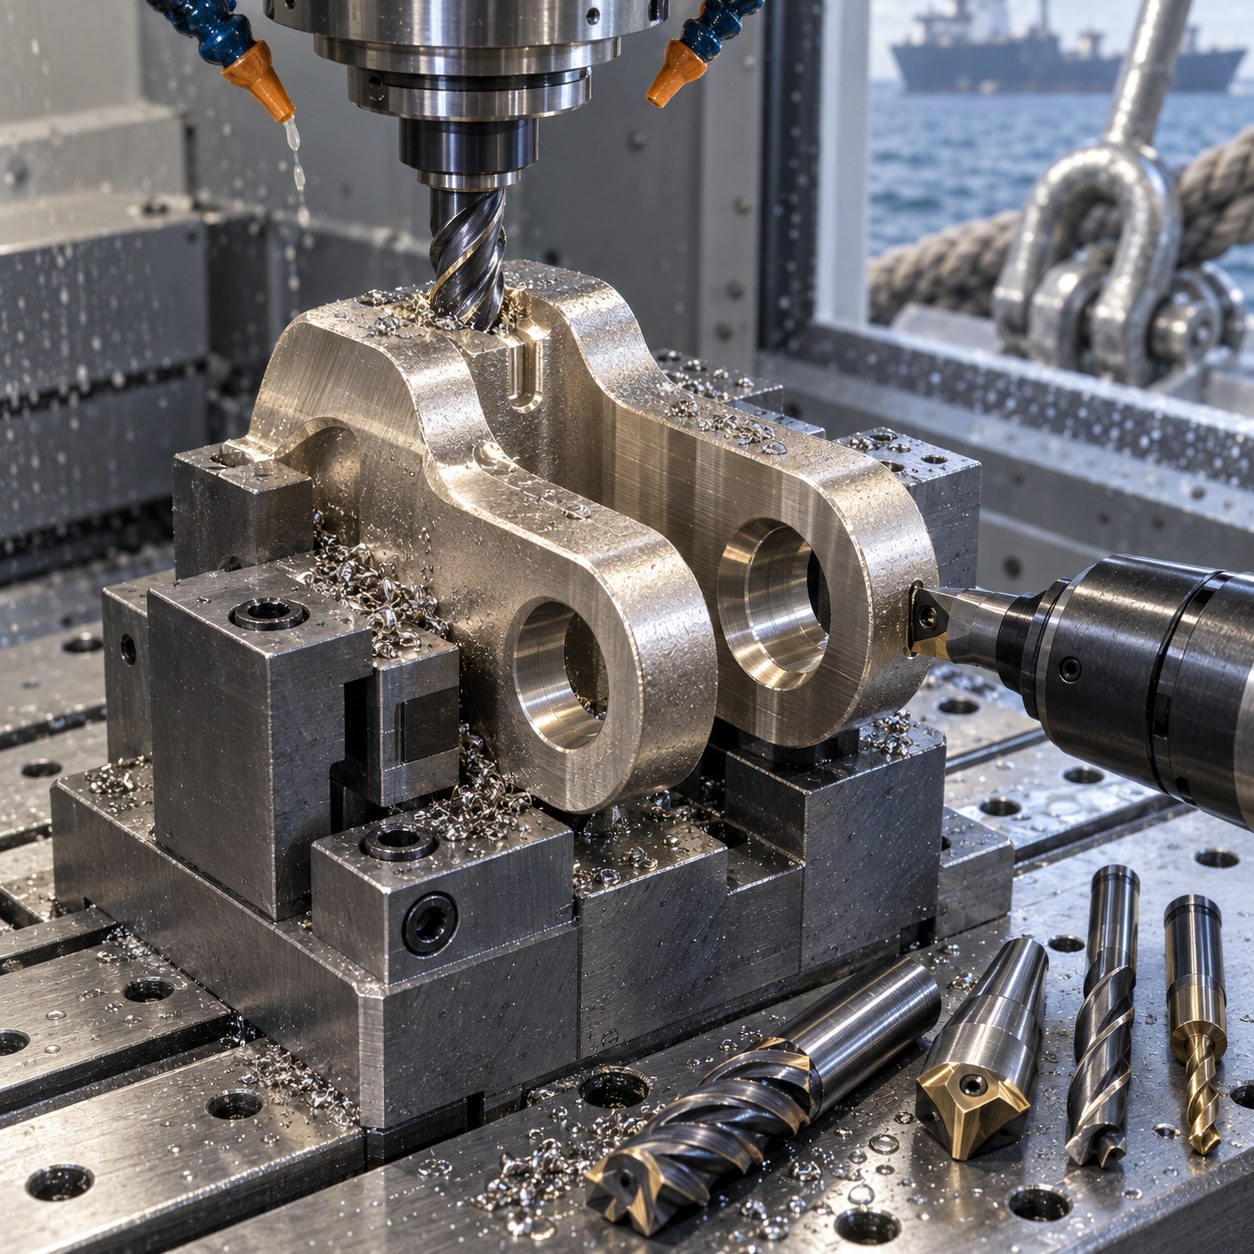
For a Monel K-500 marine clevis, the search problem is how to pick carbide tools when the fork slot removes stiffness before the pin bore is final. The drawing combines bearing contact, fatigue radius and corrosion-service edges, so tool choice has to prevent work hardening instead of simply chasing metal removal rate.
Fork-slot drawing features mapped to carbide tools
| Clevis feature | Carbide tool package | Rejected shortcut |
|---|---|---|
| Deep fork slot | 12 mm variable-helix carbide rougher, AlTiN, trochoidal entry | A full-slot HSS cutter would rub and harden Monel before reaching depth. |
| Pin bore pair | Pilot, indexable drill, semi-bore, then carbide fine boring bar | Line-bored correction is needed after fork-slot stress release. |
| Fillet relief | 6 mm corner-radius carbide end mill, short flute, relieved neck | Matches fatigue radius; a sharp square end mill leaves a crack starter. |
| Grease groove | Formed carbide keyseat cutter with polished rake | Cuts the cross groove without hand-digging burrs into the bore. |
| Mouth chamfers | 90° coated carbide chamfer mill with limited land | Controls assembly lead-in while preserving lug thickness. |
Order of operations around the pin bore
Machine the outside stock on sacrificial tabs, rough the fork slot symmetrically, rest the part, then line-bore the pin holes from a supported orientation. The fillet relief and grease groove follow the bore so burr direction can be controlled toward accessible faces.
Work-hardening, chip load and burr control
Monel K-500 punishes rubbing. The rougher must keep chip thickness real, coolant must reach the slot bottom, and the fine boring bar is changed on bore finish trend rather than catastrophic wear. Any dwell in the grease groove is treated as a burr generator.
Inspection gates for a loaded clevis
Inspection begins with fork spacing and lug parallelism, then checks pin-bore size, coaxiality and surface finish. A flexible brush pass is accepted only after borescope review confirms the grease groove did not fold a burr into the bearing track.
Tooling FAQ
Why line-bore the clevis after roughing the fork slot?
The slot changes lug stiffness, so final bore coaxiality should be corrected after that movement.
Which tool fails first in Monel K-500?
The rougher usually loses edge honesty by rubbing; the sign is heat, curled burrs and rising spindle load.
Can the grease groove be hand cleaned?
Only after borescope confirmation; blind scraping can fold a burr into the bearing bore.
中文: Monel K-500船用叉耳开口槽与销孔配刀
Monel K-500船用叉耳的关键问题是:开口槽先削弱刚性,销孔又要承载配合,硬质合金刀具怎样选才不会加工硬化。图纸同时包含轴承接触、疲劳圆角和耐腐蚀边缘。
叉耳图纸特征到硬质合金刀具映射
| 叉耳特征 | 硬质合金刀具组合 | 淘汰的捷径 |
|---|---|---|
| 深开口槽 | 12 mm变螺旋AlTiN硬质合金粗铣刀,摆线切入 | 整体HSS开槽会摩擦并提前加工硬化。 |
| 成对销孔 | 引导钻、可转位钻、半精镗、硬质合金精镗杆 | 开槽释放后必须通过线镗修正同轴。 |
| 圆角避让 | 6 mm圆角硬质合金立铣刀,短刃避空颈 | 满足疲劳圆角;方肩刀会留下裂纹源。 |
| 润滑槽 | 成形硬质合金键槽刀,抛光前角 | 切出交叉槽,不把毛刺手工刮入孔内。 |
| 入口倒角 | 90度涂层硬质合金倒角刀,小刃带 | 给装配导入,同时保留叉耳厚度。 |
围绕销孔的加工顺序
外形先留牺牲耳,开口槽左右对称粗加工并静置,再从受支撑方向线镗销孔。圆角避让和润滑槽在孔加工后执行,使毛刺方向朝向可检查表面。
加工硬化、切屑负荷和毛刺控制
Monel K-500最怕摩擦。粗铣刀要保持真实切屑厚度,冷却必须到达槽底;精镗杆按孔表面趋势换刀,而不是等到磨损失控。润滑槽内任何停顿都视为毛刺风险。
承载叉耳的检测关口
检测从叉口宽度和平行度开始,再查销孔尺寸、同轴度和粗糙度。柔性刷只在内窥镜确认润滑槽没有折入孔内毛刺后使用。
配刀问答
为什么开口槽粗加工后再线镗销孔?
开槽改变叉耳刚性,最终同轴度应在变形释放后修正。
Monel K-500哪把刀最容易先失效?
通常是粗铣刀因摩擦失去锋利,表现为发热、卷毛刺和主轴负载上升。
润滑槽能手工清理吗?
必须先内窥镜确认;盲目刮削可能把毛刺折进承载孔。
Español: Herramientas para horquilla marina Monel K-500
En una horquilla marina Monel K-500, la pregunta es elegir carburo cuando la ranura reduce rigidez antes de terminar el pasador. El plano une contacto, radio de fatiga y borde anticorrosión.
Plano de horquilla convertido en herramientas
| Elemento de chape | Paquete de carburo | Atajo descartado |
|---|---|---|
| Ranura de horquilla | Fresa carburo 12 mm hélice variable AlTiN | HSS ranurando endurece el Monel. |
| Agujero de pasador | Piloto, broca indexable, semi-mandrinado y barra fina | Corrige coaxialidad tras liberar la ranura. |
| Radio de alivio | Fresa carburo 6 mm de radio | Evita iniciador de grieta. |
| Ranura de engrase | Fresa tipo chavetero de carburo pulido | No arrastra rebaba al agujero. |
| Chaflanes | Chaflanador 90° de carburo recubierto | Da entrada sin adelgazar orejas. |
Secuencia alrededor del pasador
Se deja material en pestañas, se desbasta la ranura de forma simétrica, se deja reposar y después se mandrina la pareja de agujeros. Radios y engrase se hacen cuando la rebaba puede verse.
Endurecimiento, viruta y rebaba
Monel K-500 endurece si roza. La viruta debe ser real, el refrigerante debe llegar al fondo y la barra fina se cambia por tendencia de acabado.
Controles para pieza cargada
Se miden apertura, paralelismo, diámetro, coaxialidad y rugosidad. El cepillo flexible solo entra después del boroscopio.
FAQ de herramientas
¿Por qué mandrinar después de la ranura?
La ranura cambia la rigidez de las orejas.
¿Qué herramienta falla antes?
La fresa de desbaste cuando empieza a rozar.
¿Limpiar a mano?
Solo tras boroscopio.
Français: Outils pour chape marine Monel K-500
Pour une chape marine Monel K-500, le choix carbure dépend du fait que la fente retire la rigidité avant l’alésage de pion. Le plan lie contact, rayon de fatigue et bord anticorrosion.
Du plan de chape au choix carbure
| Élément de chape | Ensemble carbure | Raccourci écarté |
|---|---|---|
| Fente de chape | Fraise carbure 12 mm hélice variable AlTiN | HSS en pleine fente écrouit le Monel. |
| Alésage de pion | Pilote, foret indexable, semi-alésage puis barre fine | Rattrape la coaxialité après détente. |
| Rayon de congé | Fraise carbure 6 mm à rayon | Supprime l’amorce de fissure. |
| Rainure de graisse | Fraise à clavette carbure polie | N’envoie pas la bavure dans l’alésage. |
| Chanfreins | Chanfreineur carbure 90° revêtu | Guide l’assemblage sans amincir. |
Ordre autour de l’alésage
Les onglets sacrificiels restent en place, la fente est ébauchée symétriquement, puis la paire d’alésages est reprise après repos. Congés et rainure de graisse suivent pour orienter les bavures.
Écrouissage, copeau et bavure
Le Monel K-500 s’écrouit au frottement. Il faut une vraie épaisseur de copeau, l’arrosage au fond et un changement de barre selon l’état de surface.
Contrôles d’une chape chargée
On vérifie écartement, parallélisme, diamètre, coaxialité et rugosité. La brosse flexible est autorisée après endoscope seulement.
FAQ outil
Pourquoi aléser après la fente ?
La fente change la rigidité des oreilles.
Quel outil fatigue d’abord ?
La fraise d’ébauche si elle frotte.
Nettoyage manuel ?
Seulement après endoscope.
Русский: Инструмент для серьги Monel K-500
Для морской серьги Monel K-500 инструмент выбирают с учетом того, что паз вилки снимает жесткость до финиша отверстия пальца. Чертеж связывает контакт, радиус усталости и антикоррозионные кромки.
Чертеж серьги и карбидный инструмент
| Элемент серьги | Пакет инструмента | Что отклонено |
|---|---|---|
| Глубокий паз | Карбидная фреза 12 мм AlTiN с переменной спиралью | HSS быстро натирает и наклепывает Monel. |
| Отверстие пальца | Пилот, сверло, получистовая и тонкая расточка | После паза нужна коррекция соосности. |
| Радиус разгрузки | Карбидная радиусная фреза 6 мм | Не оставляет острый концентратор. |
| Смазочная канавка | Полированная карбидная шпоночная фреза | Не заталкивает заусенец в отверстие. |
| Фаски входа | Карбидная фасочная фреза 90° | Сохраняет толщину ушей. |
Порядок вокруг отверстия пальца
Сначала оставляют технологические уши, симметрично чернят паз, дают детали отстояться и затем растачивают пару отверстий. Радиусы и смазочную канавку делают после отверстия.
Наклеп, стружка и заусенцы
Monel K-500 наклепывается от трения. Нужна реальная стружка, СОЖ на дне паза и замена расточной оправки по ухудшению поверхности.
Контроль нагруженной детали
Проверяют ширину вилки, параллельность, размер, соосность и шероховатость отверстия. Щетку применяют только после эндоскопа.
Вопросы по инструменту
Почему расточка после паза?
Паз меняет жесткость ушей.
Какой инструмент устает первым?
Черновая фреза при трении.
Можно чистить вручную?
Только после эндоскопа.