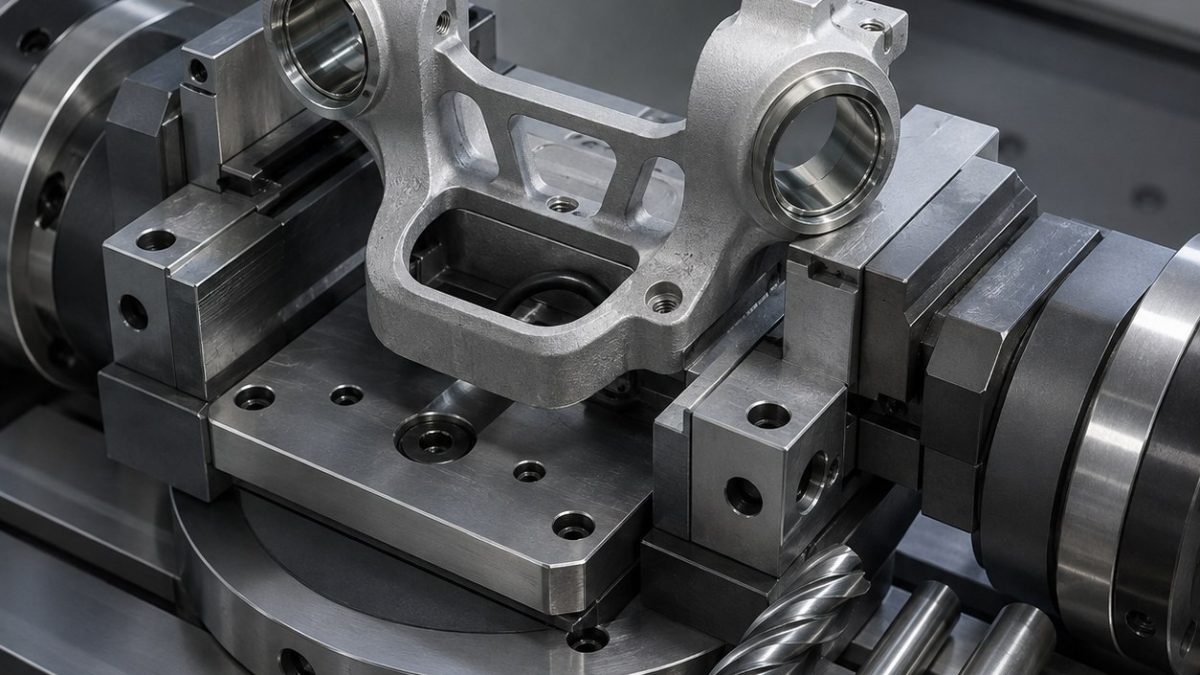
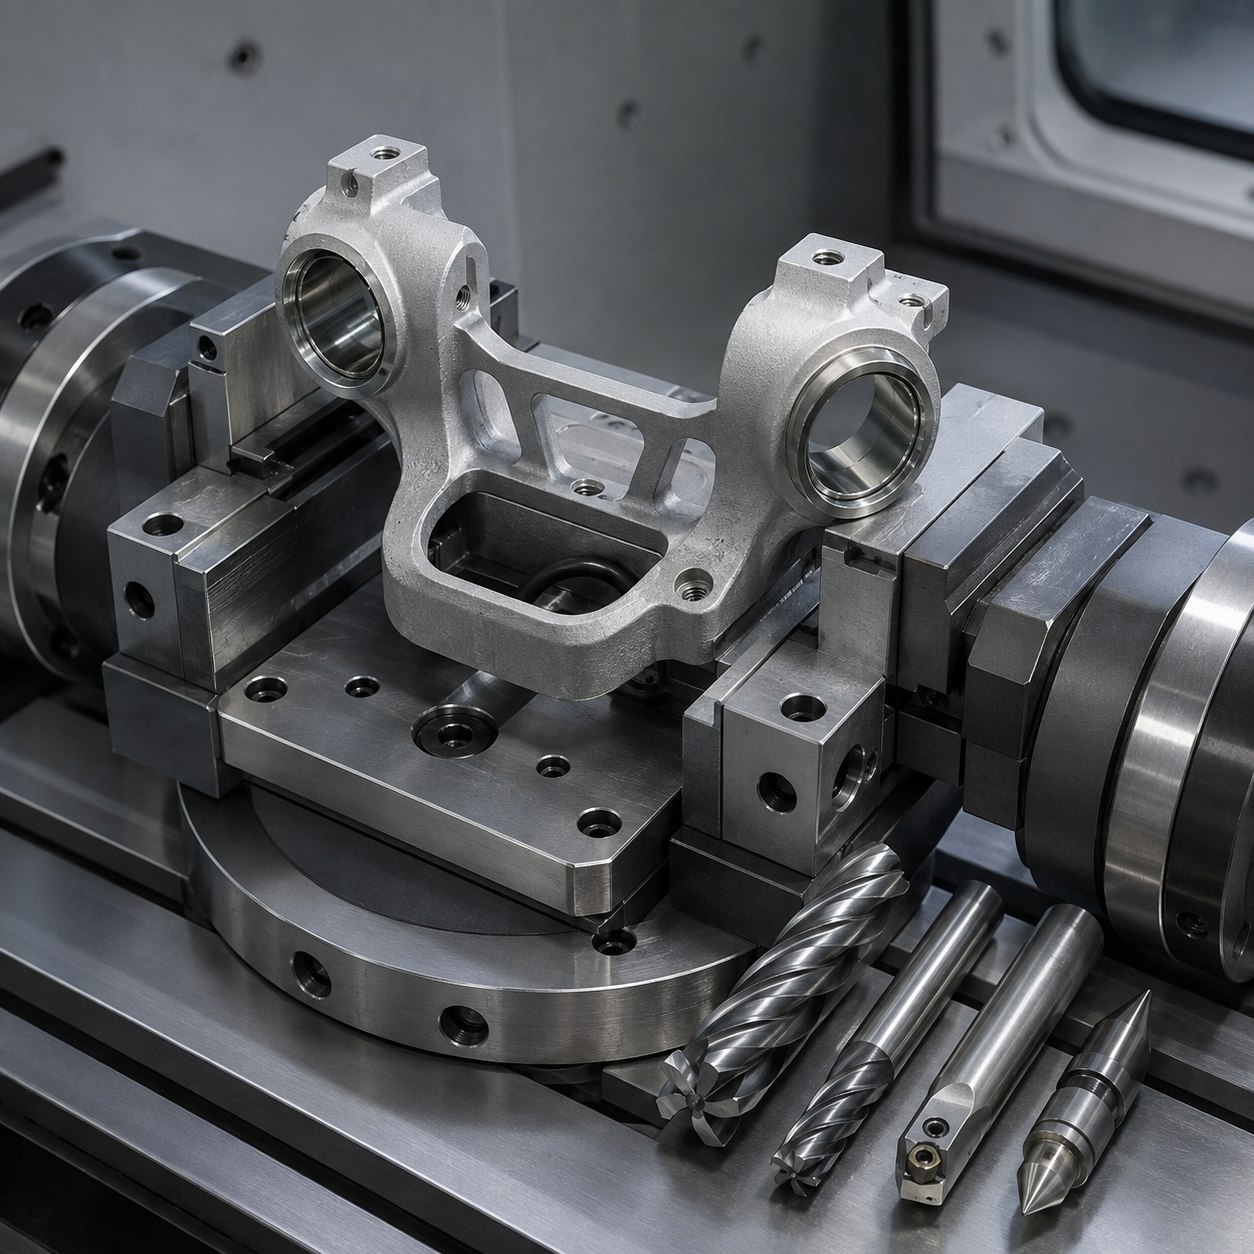
中文: ZA-27云台壳体对置轴承孔与薄过线桥配刀
该案例通过软爪转台夹具保持两侧轴承孔同轴,并控制薄过线桥的变形和翻边。
图纸特征配刀表
| 图纸区域 | 选择刀具 | 原因与替代方案 |
|---|---|---|
| Datum face and casting skin | Ø32 high-positive PCD face mill | Cleanly cuts zinc-rich alloy; a heavy honed steel insert is rejected because it smears. |
| Opposed bearing bores | Ø12 carbide pilot, modular fine boring head, balanced short holder | Boring corrects cast-core position and controls coaxiality. |
| Cable pocket | Ø8 3-flute polished carbide rougher plus Ø4 corner-radius finisher | Large flute space prevents chip welding and preserves the thin bridge. |
| Thin bridge edges | Ø3 2-flute polished carbide, alternating side passes | Balanced stock release limits bridge pull and burr rollover. |
| Threaded mounts | Carbide drill, thread mill and compact back-chamfer tool | Thread milling reduces tap breakage in a thin, irregular wall. |
工艺、粗精加工与排屑
Use cast pads for the first location, probe both bore bosses, rough the pocket in a symmetric sequence, and finish bores from a trunnion setup without releasing the soft jaws. Alternate bridge-side passes, use air-rich coolant for chip evacuation, and keep PCD away from interrupted steel fixture contact. Related reading: tool-overhang control and precision bore finishing.
检验与刀具寿命
Check each bearing bore for size and roundness, then measure their common-axis error without unclamping. CMM checks threaded-hole position to the bore axis; an optical edge check grades bridge burrs. Release from the fixture and repeat bridge flatness to expose clamp distortion.
常见问题
为什么不能一把刀加工全部特征?
大刀负责稳定去除,小刀只用于受限区域,可减少挠曲和异常磨损。
什么时候能改刀补?
只有误差方向和大小稳定时才改;持续变化说明挠曲、热漂移或磨损。
最终放行看什么?
尺寸、基准关系、粗糙度、毛刺和通道清洁度必须同时合格。


