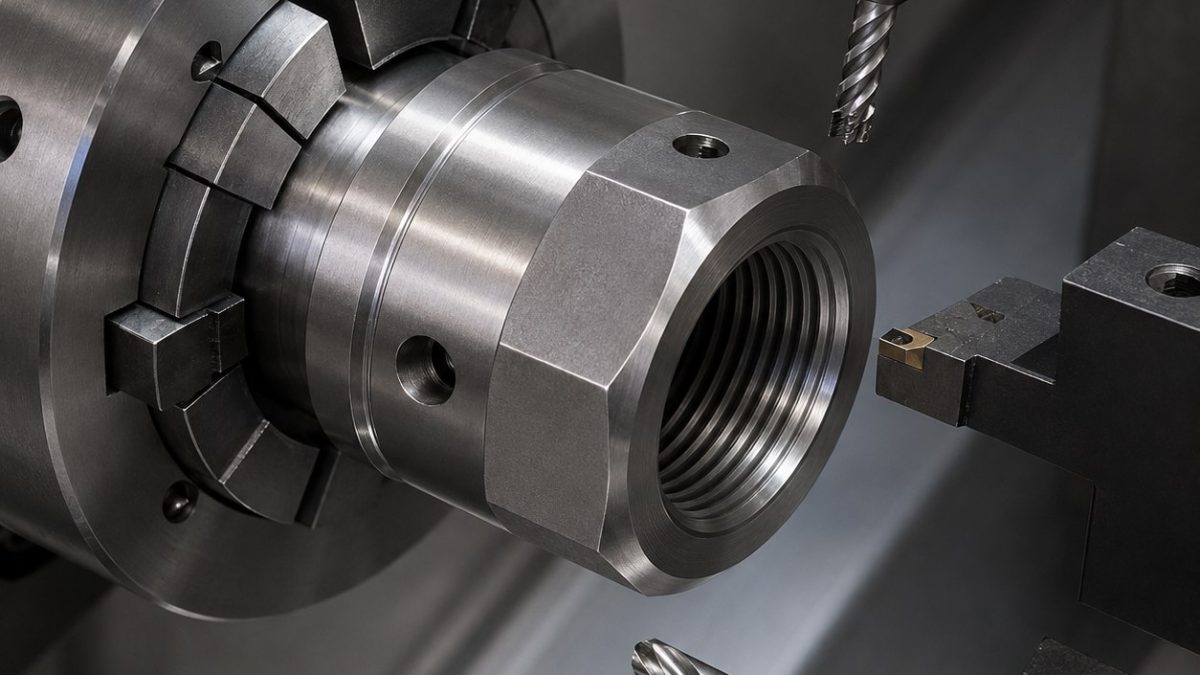
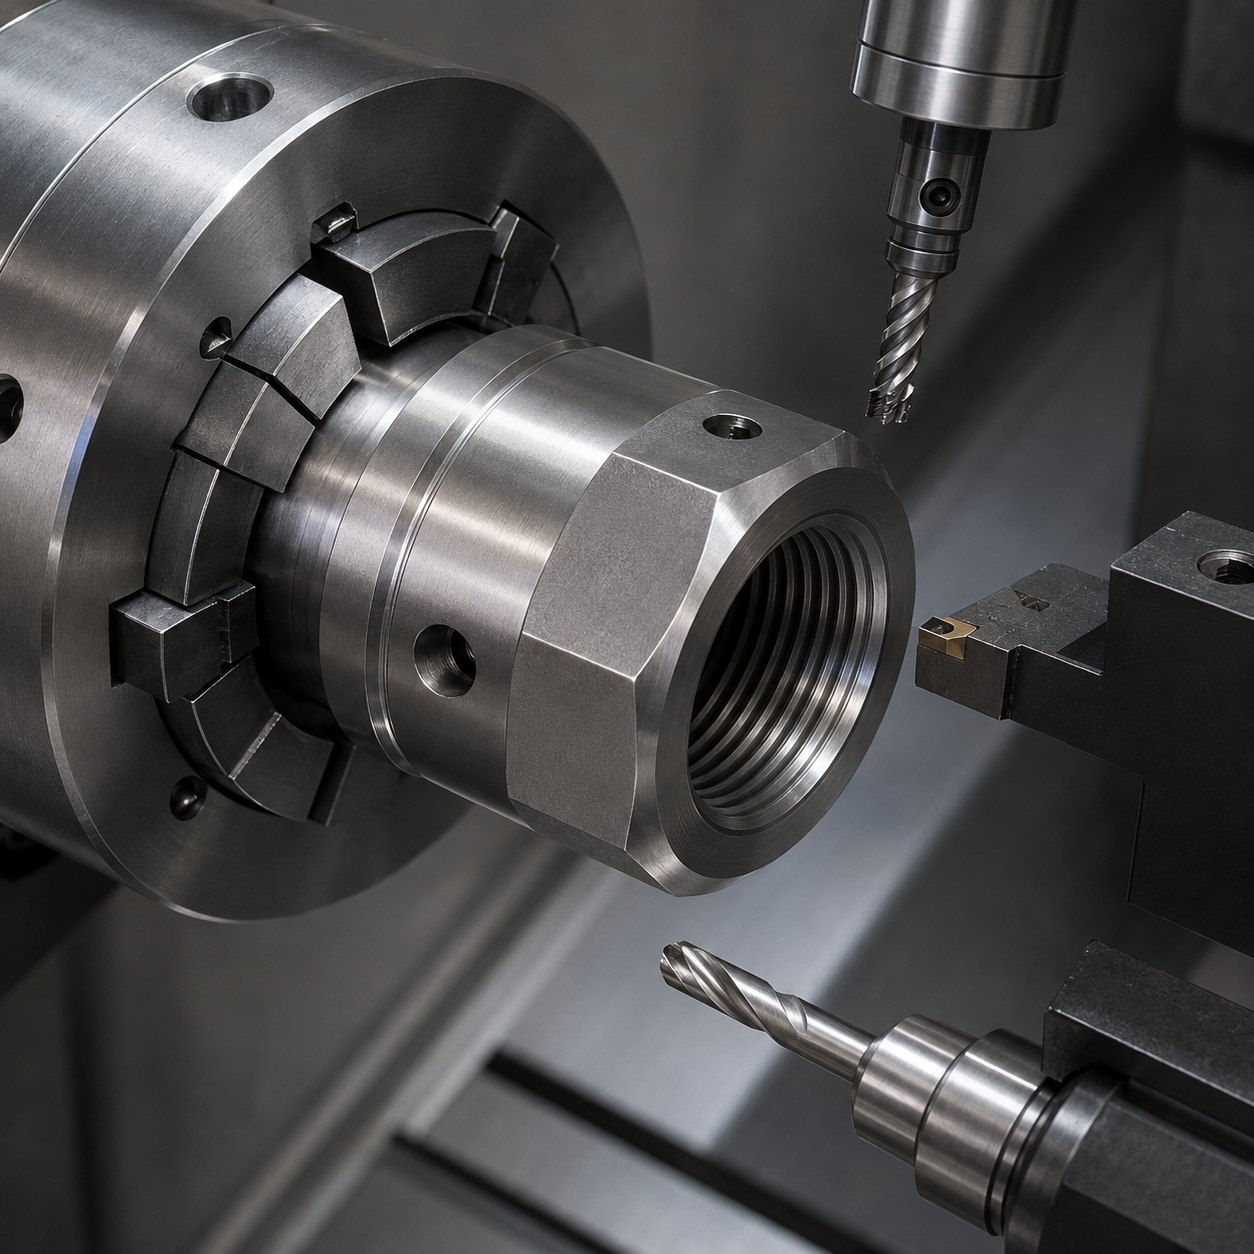
中文: Nitronic 60阀杆螺母深梯形螺纹与交叉油孔配刀
该案例重点解决深螺纹、润滑槽与交叉油孔的配刀,防止加工硬化、粘刀和孔口毛刺。
图纸特征配刀表
| 图纸区域 | 选择刀具 | 原因与替代方案 |
|---|---|---|
| Blank and flats | Ø12 5-flute AlTiN variable-pitch carbide end mill, small hone | Resists work hardening while avoiding the rubbing of a dull general-purpose cutter. |
| Deep ACME thread | Single-profile carbide thread mill, TiAlN, hydraulic holder, radial passes | Lower torque and adjustable pitch diameter; a form tap is rejected for seizure risk. |
| Lubricant groove | 2 mm carbide grooving insert with sharp positive geometry | Controls groove width without smearing the sidewalls. |
| Cross grease holes | Carbide stub drill plus through-coolant long drill and back-chamfer tool | Pilot stability and intersection deburring prevent a blocked oil path. |
| Entry chamfer | 90° 3-flute carbide chamfer mill, short reach | Separates lead geometry from thread tool wear. |
工艺、粗精加工与排屑
Turn the reference face and OD in one collet setup, mill flats only after the bore axis is established, interpolate the ACME thread from bottom outward, then drill grease holes from supported faces. Use high-pressure coolant and no dwell at reversals; inspect chips for blue rubbing before allowing offset correction. Related reading: tool-overhang control and precision bore finishing.
检验与刀具寿命
Verify major and pitch diameters with a functional ACME gauge and CMM flank points, measure lead over the working length, pin-check cross-hole breakthrough, borescope the groove intersections and record Ra 1.6 µm on loaded flanks. A stable size shift may be corrected; changing taper signals tool deflection or wear.
常见问题
为什么不能一把刀加工全部特征?
大刀负责稳定去除,小刀只用于受限区域,可减少挠曲和异常磨损。
什么时候能改刀补?
只有误差方向和大小稳定时才改;持续变化说明挠曲、热漂移或磨损。
最终放行看什么?
尺寸、基准关系、粗糙度、毛刺和通道清洁度必须同时合格。


