Related tooling references: C360 Brass Microfluidic Valve Seat CNC Tool Selection for Conical Seat and Tiny Cross Holes and Maraging 300 Aerospace Latch Hook CNC Tool Selection for Thin Hook Profile and Reamed Pivot Bore.
English: Ti-6Al-4V Wrist Clamp Tooling for Split Bore and Flexure Slots
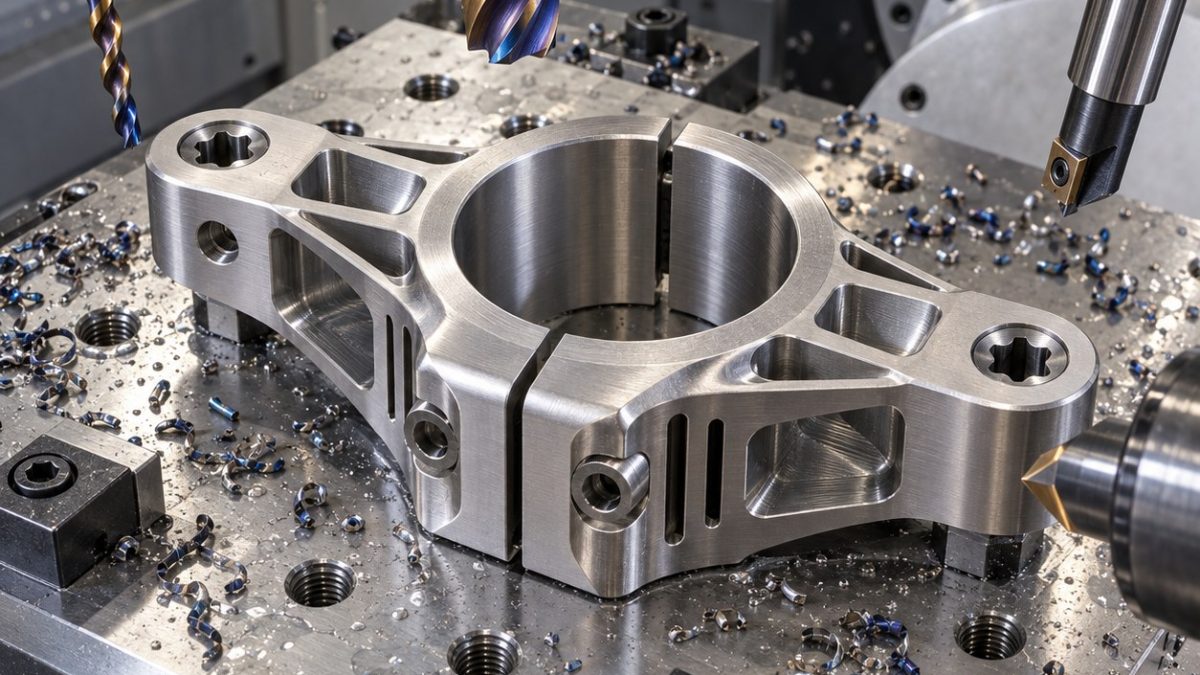
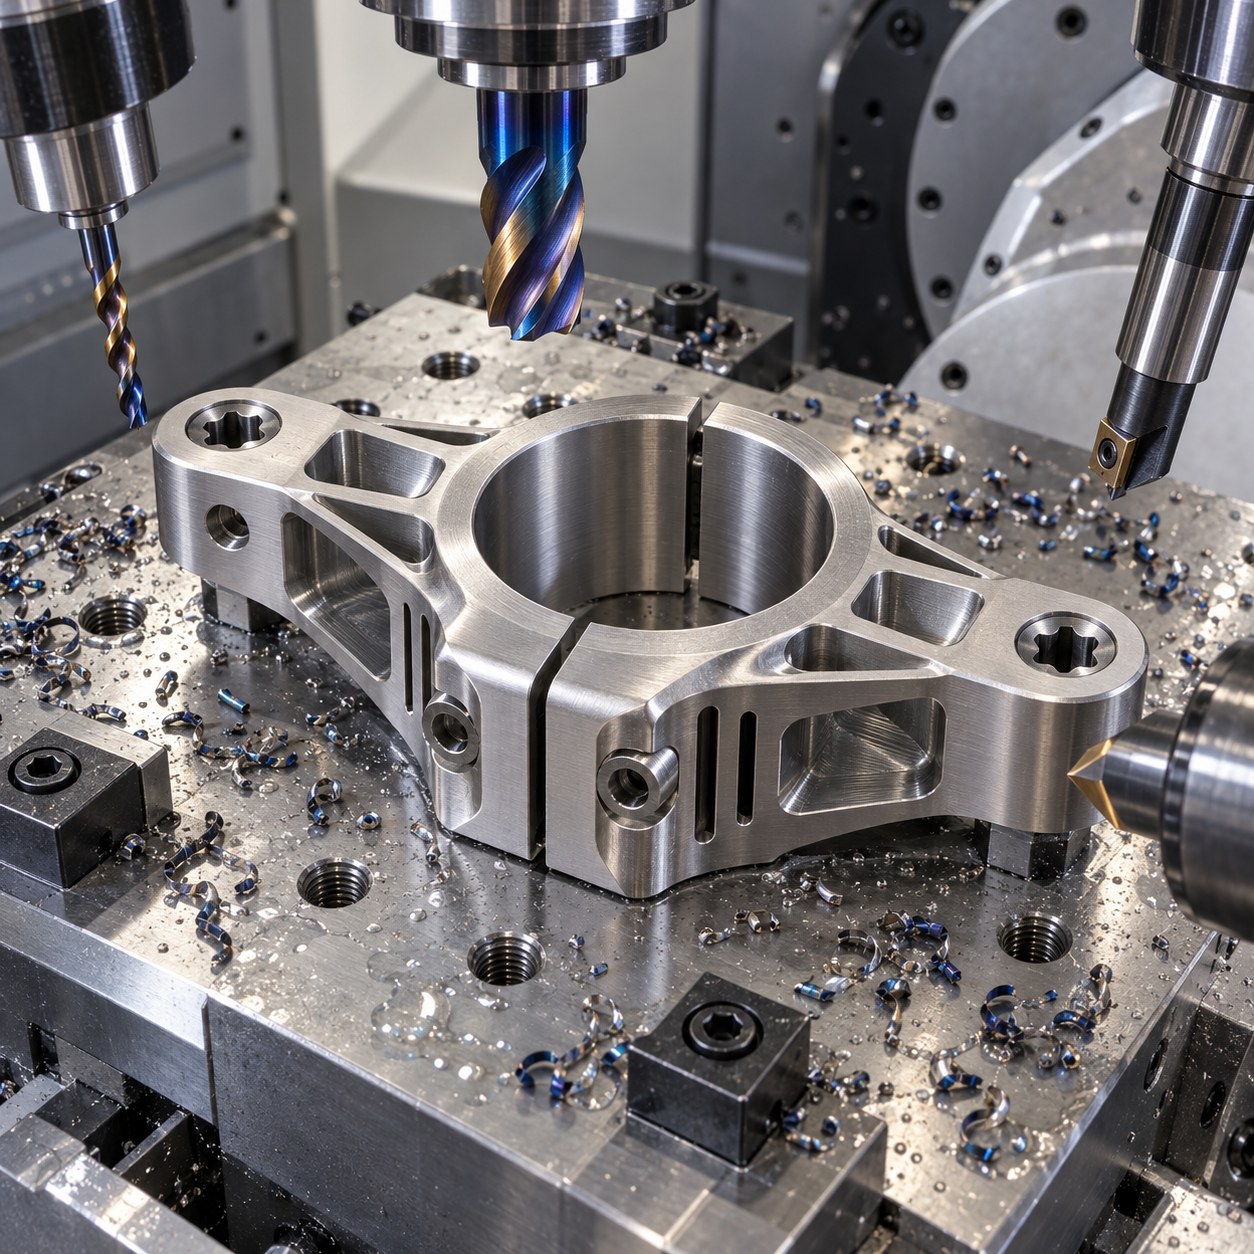
This case answers how to tool a titanium split clamp when the bore, flexure slots and screw counterbores all influence final clamping. The drawing is governed by elastic movement, not simple pocket removal.
Split-clamp features converted into titanium tooling
| Drawing feature | Carbide tool and holder | Why the alternative is rejected |
|---|---|---|
| Split bore | 12 mm variable-helix carbide semi-finisher plus fine boring head in hydraulic holder | Interpolation alone is rejected because the split gap lets the bore breathe. |
| Flexure slots | 2.5 mm 4-flute AlTiN carbide, necked, high-pressure coolant | Wire EDM is too slow and leaves a corner condition that still needs milling. |
| Clamp ears | 6 mm trochoidal rougher with corner radius | Keeps heat out of the ear root. |
| Torx counterbores | Carbide pilot drill, piloted counterbore and small chamfer mill | Separates screw seating from pilot drift. |
| Strain-relief radii | 3 mm ball end mill, short flute | Avoids a sharp crack starter at the slot end. |
Sequence that protects bore roundness
Machine the outside with the split still bridged, semi-finish the bore, cut relief radii, then open the flexure slots symmetrically. Final boring happens after a relaxation dwell so the measured bore reflects the working clamp.
Titanium heat, burr and slot-life control
Titanium heat is controlled by real chip thickness, sharp AlTiN edges and coolant aimed into the narrow slots. Tool life is stopped by burr color and slot-wall rubbing, not only by flank wear.
Inspection of clamp function
Inspection checks free bore size, clamped bore size with a torque simulator, slot width, ear parallelism and counterbore seating. The article passes when the bore repeats after three clamp cycles.
Tooling FAQ
Why not finish the split bore before slotting?
Slotting changes clamp stiffness, so final boring must wait until the split feature is functional.
What ruins titanium slot finish first?
Rubbing at the exit and coolant starvation, not always visible flank wear.
How is clamp repeatability checked?
By measuring the bore free and under repeated simulated screw torque.
中文: Ti-6Al-4V机器人腕部夹环开口孔与柔性槽配刀
本案例回答钛合金开口夹环如何配刀:开口孔、柔性槽和螺钉沉孔都会影响最终夹紧。图纸控制的是弹性运动,不是简单开腔去料。
开口夹环特征到钛合金配刀
| 图纸特征 | 硬质合金刀具与刀柄 | 淘汰原因 |
|---|---|---|
| 开口孔 | 12 mm变螺旋硬质合金半精刀加液压刀柄精镗头 | 单纯插补会因开口缝让孔形呼吸。 |
| 柔性槽 | 2.5 mm四刃AlTiN缩颈硬质合金刀,高压冷却 | 线切割太慢,角部状态仍需铣削修正。 |
| 夹紧耳 | 6 mm圆角摆线粗铣刀 | 降低耳根热输入。 |
| Torx沉孔 | 硬质合金引导钻、导向沉孔刀、小倒角刀 | 把螺钉座面和底孔偏移分开。 |
| 减应力圆角 | 3 mm短刃球刀 | 避免槽端尖角成为裂纹源。 |
保护孔圆度的加工顺序
外形加工时先保留开口桥,孔半精加工后切减应力圆角,再对称打开柔性槽。最终精镗在静置释放后完成,使检测到的孔径符合实际夹紧状态。
钛合金热量、毛刺和槽刀寿命控制
钛合金热量靠真实切屑厚度、锋利AlTiN刃口和指向窄槽的冷却控制。换刀依据是毛刺颜色和槽壁摩擦趋势,不只看后刀面磨损。
夹紧功能检测
检测自由孔径、模拟扭矩夹紧后的孔径、槽宽、夹紧耳平行度和沉孔座面。三次夹紧循环后孔径仍重复才算合格。
配刀问答
为什么不开槽前就精修开口孔?
开槽会改变夹环刚性,最终镗孔必须等开口结构成形后再做。
钛合金槽面最先被什么破坏?
通常是出口摩擦和冷却不足,不一定是明显后刀面磨损。
夹紧重复性怎么查?
测自由孔径,并在模拟螺钉扭矩下重复测孔径。
Español: Herramientas para abrazadera Ti-6Al-4V con ranuras
La abrazadera Ti-6Al-4V se rige por movimiento elástico: alésage, ranuras y avellanados cambian el cierre.
Abrazadera partida convertida en herramientas
| Elemento del plano | Herramienta y porta | Alternativa rechazada |
|---|---|---|
| Alésage partido | Carburo 12 mm y mandrinado fino | La interpolación respira en la ranura. |
| Ranuras flexibles | Carburo 2,5 mm AlTiN con cuello | EDM deja esquina a corregir. |
| Orejas | Desbaste trocoidal 6 mm | Reduce calor. |
| Avellanados | Broca piloto, lamador y chaflán | Separa asiento y deriva. |
| Radios | Bola 3 mm | Evita grieta. |
Secuencia para redondez
Se mecaniza con el puente, se semiacaba el agujero, se cortan radios y luego ranuras simétricas. El mandrinado final espera relajación.
Calor, rebaba y vida en titanio
El titanio requiere viruta real, filo AlTiN y refrigerante dentro de la ranura. La vida se decide por rebaba y roce.
Inspección de función
Se revisa agujero libre, agujero apretado, ranura, paralelismo y asiento.
FAQ
¿Por qué no acabar el agujero antes?
La ranura cambia la rigidez.
¿Qué daña la ranura?
Roce y falta de refrigerante.
¿Cómo medir repetición?
Libre y con par simulado.
Français: Outils pour collier Ti-6Al-4V à alésage fendu
Le collier Ti-6Al-4V dépend du mouvement élastique: alésage, fentes et lamages changent le serrage.
Collier fendu et choix titane
| Élément du plan | Outil et attachement | Option écartée |
|---|---|---|
| Alésage fendu | Carbure 12 mm puis alésage fin | L’interpolation respire avec la fente. |
| Fentes flexibles | Carbure 2,5 mm AlTiN à col | EDM laisse l’angle à reprendre. |
| Oreilles | Ébauche trochoïdale 6 mm | Réduit la chaleur. |
| Lamages | Foret, lamoir et chanfrein | Sépare assise et dérive. |
| Rayons | Boule 3 mm | Évite l’amorce. |
Séquence pour rondeur
On garde un pont, on semi-finit l’alésage, on coupe les rayons puis les fentes symétriques. L’alésage final attend la détente.
Chaleur, bavure et durée
Le titane exige une vraie coupe, arête AlTiN et arrosage dans la fente. Bavure et frottement guident la vie outil.
Contrôle fonctionnel
Contrôle alésage libre, alésage serré, fente, parallélisme et assise.
FAQ
Pourquoi attendre pour l’alésage ?
La fente change la rigidité.
Défaut de fente ?
Frottement et manque d’arrosage.
Répétabilité ?
Mesure libre et serrée.
Русский: Инструмент для зажима Ti-6Al-4V
Зажим Ti-6Al-4V управляется упругим движением: отверстие, пазы и цековки меняют зажим.
Разрезной зажим и инструмент
| Элемент | Инструмент | Что отклонено |
|---|---|---|
| Разрезное отверстие | Карбид 12 мм и тонкая расточка | Интерполяция дышит в прорези. |
| Гибкие пазы | Карбид 2,5 мм AlTiN | EDM требует доработки угла. |
| Уши | Трохоид 6 мм | Меньше тепла. |
| Цековки | Пилот, цековка, фаска | Отделяет посадку. |
| Радиусы | Шаровая 3 мм | Нет трещины. |
Порядок для круглости
Сначала оставляют мост, получистят отверстие, режут радиусы и симметрично открывают пазы. Финишная расточка после выдержки.
Тепло, заусенец и ресурс
Титан требует реальной стружки, AlTiN кромки и СОЖ в паз. Ресурс задают заусенец и трение.
Контроль зажима
Контроль свободного и зажатого отверстия, пазов, параллельности и посадок.
Вопросы
Почему отверстие не сразу?
Паз меняет жесткость.
Что портит паз?
Трение и нехватка СОЖ.
Как проверить повтор?
Свободно и под моментом.