中文:图纸解读与配刀方案
本文围绕 6061-T6 thin-wall instrument enclosure CNC datum pocket thread milling 展开。零件特征包括thin walls, a deep electronics pocket, a gasket land, corner radii, countersunk mounting holes and small threaded bosses。文章重点不是泛泛介绍 CNC 加工,而是把图纸要求转化为夹具、配刀、参数、工序和检测方案。
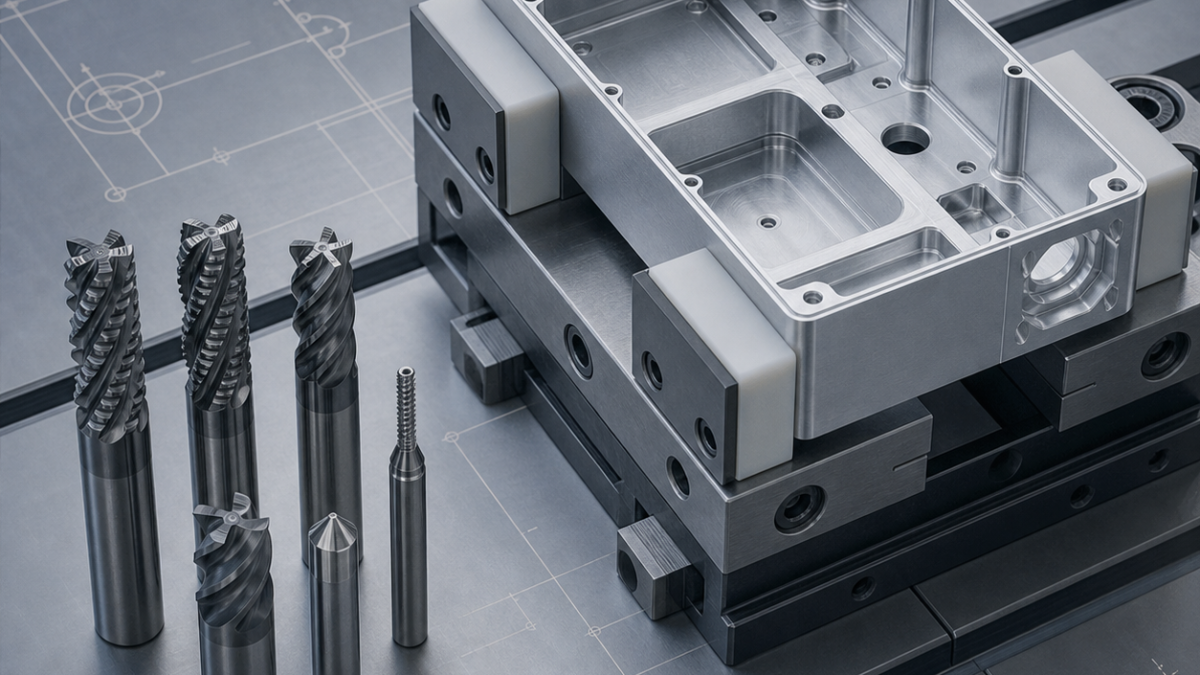
建议以the machined datum face, gasket land and protected locating holes作为核心基准,夹具方案为:machine the datum face first, then locate the part in contour-matched aluminum soft jaws with broad support beneath the floor。配刀可采用:a 10 mm three-flute polished carbide end mill, a 6 mm reduced-neck finisher, a corner-radius tool, a chamfer mill and a carbide thread mill。粗加工、半精加工和精加工应分开,关键尺寸在零件刚性最稳定的状态下完成。检测应确认wall position at several heights, gasket-land flatness, thread quality, pocket floor finish and open-rim distortion,并重点关注毛刺、变形、刀具磨损和重复装夹误差。