Related tooling references: Hardened D2 Trim Die Stripper Plate CNC Tool Selection for Slug Windows and Guided Punch Bores and Aluminum Nitride Power Module Carrier CNC Tool Selection for Isolation Pockets and Fragile Ribs.
English: GG25 Vacuum Pump Cover Tooling for Spiral Groove and Dowel Bores
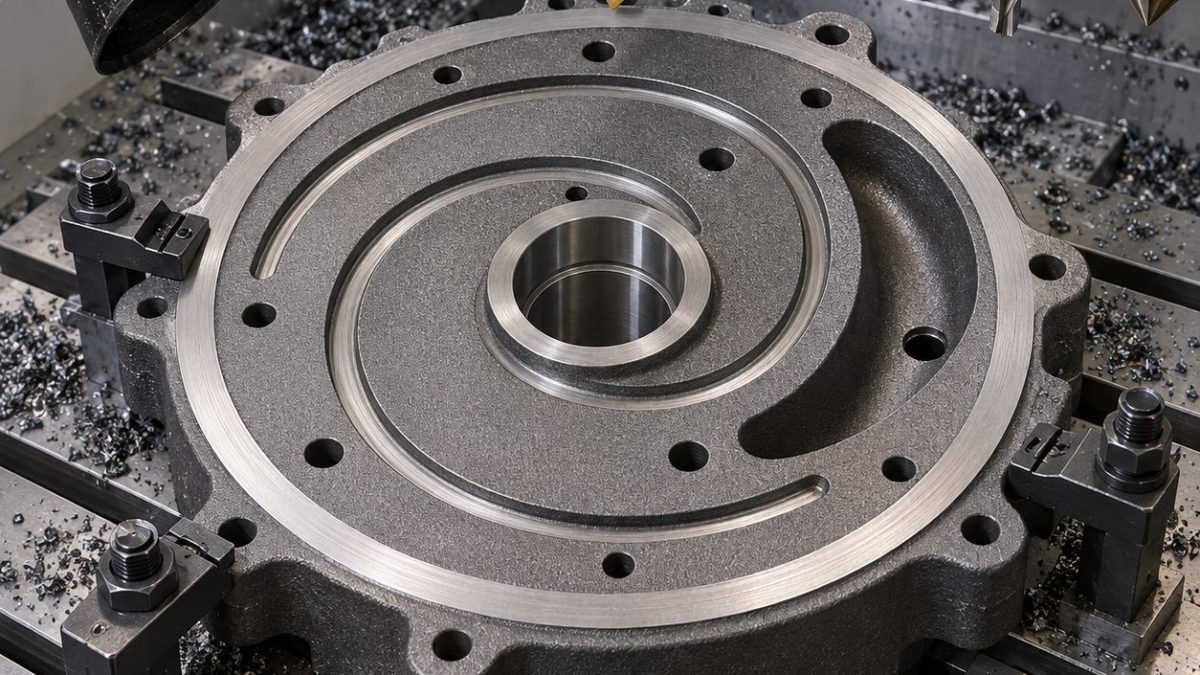
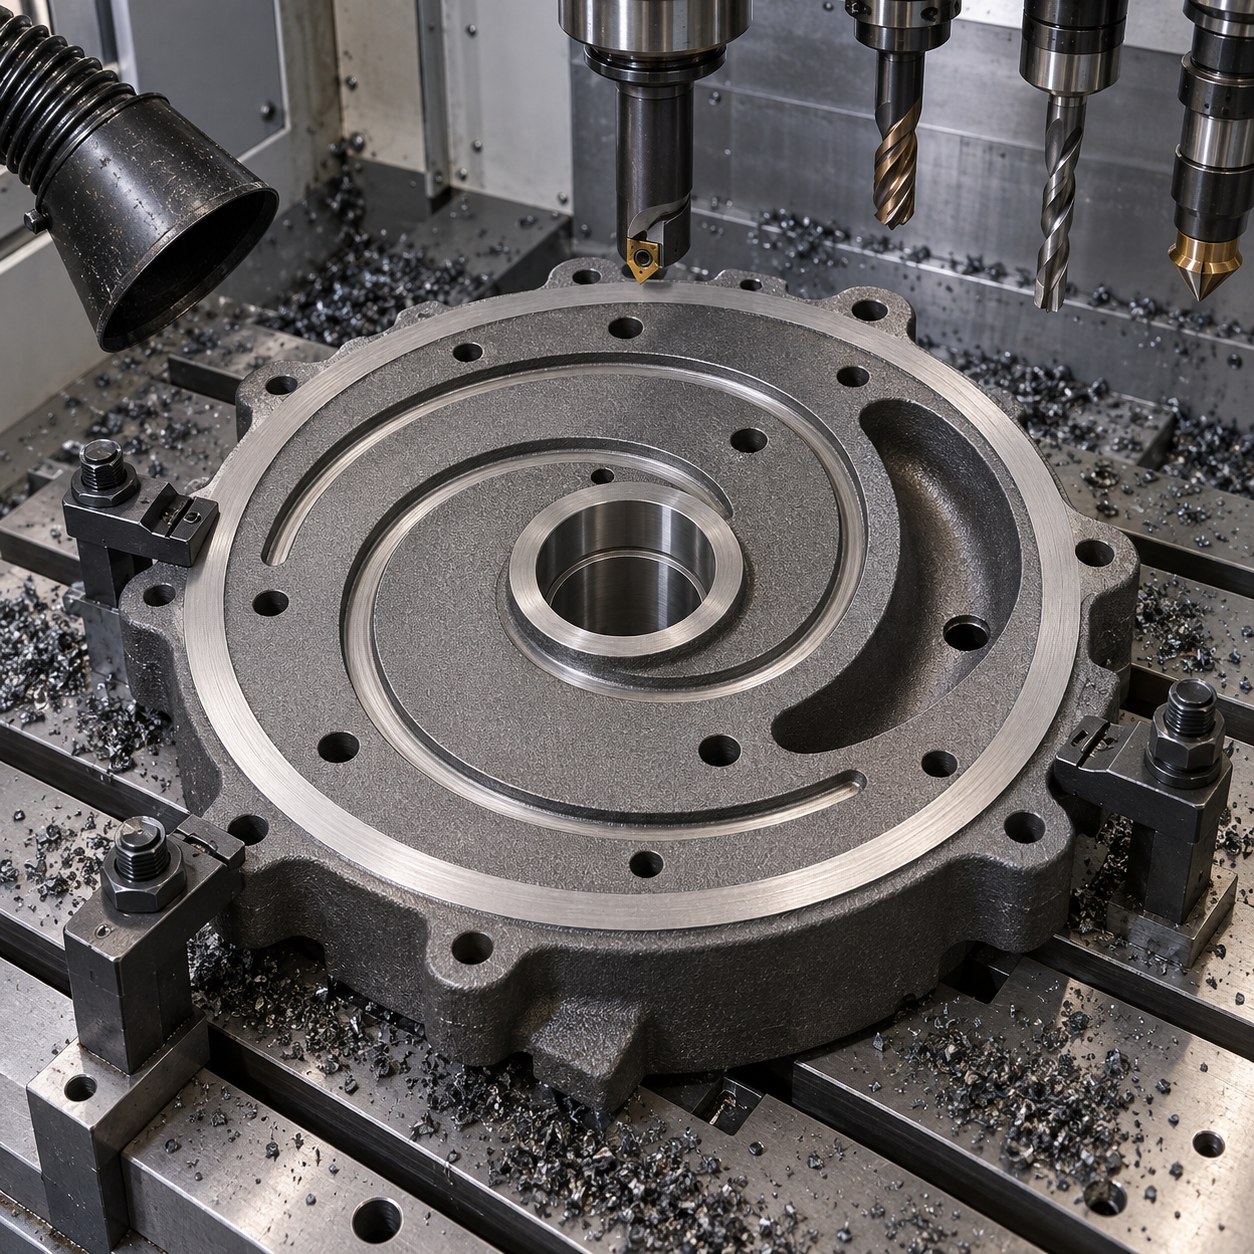
This GG25 vacuum pump end cover case answers how to select carbide tooling when the drawing mixes a spiral seal groove, dowel bore grid, bearing register and gasket land. The part looks simple, but the sealing path forces the machining plan to protect flatness and groove continuity.
Pump-cover print callouts converted to carbide tools
| Drawing feature | Carbide tool package | Control reason |
|---|---|---|
| Spiral seal groove | 2.5 mm TiCN carbide keyseat end mill with controlled radial step | A form tool is rejected because groove width changes along the spiral. |
| Dowel bore grid | Carbide drill, reamer, then adjustable fine boring on datum holes | Interpolation alone is too slow and risks graphite dust recutting. |
| Bearing register | Fine boring head with wiper insert and rigid boring holder | End-mill circular milling is rejected for roundness on abrasive iron. |
| Crescent oil pocket | 6 mm carbide rougher and 4 mm radius finisher | Avoids tearing the pocket edge into the gasket land. |
| Gasket land | Positive carbide face mill with dry dust extraction | Coolant mud is rejected because graphite slurry hides scratches. |
Machining order for sealing stability
Face the gasket land first, rough the oil pocket without touching the land edge, finish the bearing register, then cut the spiral groove with a dedicated small cutter. Dowel holes are made from the same datum setup so the cover locates repeatably before final deburring.
Cast iron dust, groove and bore-life controls
GG25 gray iron cuts freely but graphite dust recuts grooves and hides scratches. The process uses dry extraction, positive carbide, short tool overhang and replacement based on register size drift rather than sound. Coolant is avoided on the sealing face because slurry can mask damaged lands.
Flatness, bore and leak-path inspection
Inspection includes CMM dowel grid position, air-gauge or bore-gauge register size, surface plate blue check on the gasket land and optical review of the spiral groove. The cover is acceptable only if no chipped groove lip crosses the intended leak barrier.
Pump cover tooling FAQ
Why machine the spiral groove after the bearing register?
The register stabilizes datum control, while a late groove avoids recutting graphite across the seal path.
Is coolant useful on GG25 sealing faces?
Usually not here; dry extraction avoids graphite slurry hiding scratches.
What rejects the end cover?
A chipped groove lip, register roundness error or gasket-land scratch crossing the leak barrier.
中文: GG25真空泵端盖螺旋密封槽与定位孔配刀
这个GG25真空泵端盖案例回答图纸同时有螺旋密封槽、定位孔阵列、轴承止口和垫片面时怎样配刀。零件看似普通,但密封路径要求加工计划保护平面度和槽的连续性。
泵盖图纸标注到硬质合金刀具
| 图纸特征 | 硬质合金刀具组合 | 控制原因 |
|---|---|---|
| 螺旋密封槽 | 2.5 mm TiCN硬质合金键槽刀,受控径向步距 | 成形刀无法适应螺旋槽宽沿路径变化。 |
| 定位孔阵列 | 硬质合金钻、铰刀,再对基准孔精镗 | 单纯插补太慢且易让石墨粉二次切削。 |
| 轴承止口 | 带修光刃精镗头和刚性镗刀柄 | 立铣圆插补在磨蚀铸铁上圆度风险高。 |
| 月牙油腔 | 6 mm硬质合金粗刀加4 mm圆角精刀 | 避免腔边撕裂到垫片面。 |
| 垫片密封面 | 正前角硬质合金面铣刀,干式吸尘 | 冷却液泥浆会遮盖划伤。 |
保持密封稳定的加工顺序
先精修垫片面,再粗加工月牙油腔且不碰垫片边,随后精镗轴承止口,最后用专用小刀加工螺旋槽。定位孔从同一基准装夹完成,让端盖在最终去毛刺前就能重复定位。
铸铁粉尘、槽形和孔刀寿命控制
GG25灰铸铁好切,但石墨粉会二次划伤槽并掩盖刮痕。流程采用干式吸尘、正前角硬质合金、短伸出,并按止口尺寸漂移换刀,而不是只听声音。密封面避免用冷却液,因为泥浆会遮住损伤。
平面度、孔位和泄漏路径检测
检测包括CMM测定位孔阵列、气动量仪或孔表测止口、平板蓝油查垫片面,以及光学检查螺旋槽。只要有崩边跨过预定泄漏屏障,就不能接受。
泵盖配刀问答
为什么轴承止口后再加工螺旋槽?
止口先稳定基准,后加工槽可避免石墨粉反复划过密封路径。
GG25密封面适合用冷却液吗?
本案例不适合;干式吸尘避免石墨泥浆遮住划伤。
端盖什么情况拒收?
槽唇崩边、止口圆度错误,或垫片面划伤跨过泄漏屏障。
Español: Herramientas para tapa GG25 con ranura espiral
La tapa GG25 exige proteger planitud y continuidad de ranura aunque el hierro corte fácil.
Plano de tapa a carburo
| Elemento | Paquete de carburo | Control |
|---|---|---|
| Ranura espiral | Fresa chavetero TiCN 2,5 mm | La forma fija no sigue la espiral. |
| Pasadores | Broca, escariador y mandrinado fino | Evita recorte de polvo. |
| Registro | Mandrinado fino con wiper | Mejor redondez. |
| Bolsa aceite | Desbaste 6 mm y radio 4 mm | No rompe junta. |
| Plano junta | Fresa positiva seca | Sin lodo de grafito. |
Orden para estabilidad de sello
Primero plano de junta, luego bolsa de aceite, registro, ranura espiral y agujeros desde el mismo datum.
Polvo, ranura y vida de bore
El polvo de grafito recorta y oculta rayas; se usa extracción seca, carburo positivo y poco voladizo.
Planitud y fugas
MMT, calibre de bore, azul en plano y revisión óptica de ranura validan la pieza.
FAQ
¿Por qué ranura tarde?
Evita recortar polvo en el sello.
¿Refrigerante?
No, forma lodo de grafito.
¿Qué rechaza la tapa?
Labio astillado o raya de fuga.
Français: Outils pour couvercle GG25 à rainure spirale
Le couvercle GG25 protège planéité et rainure malgré une fonte facile à couper.
Plan de couvercle vers carbure
| Élément | Ensemble carbure | Contrôle |
|---|---|---|
| Rainure spirale | Fraise TiCN 2,5 mm | La forme fixe ne suit pas. |
| Pions | Foret, alésoir, alésage fin | Moins de recoupe poudre. |
| Portée | Alésage fin wiper | Rondeur. |
| Poche huile | Ébauche 6 mm et rayon 4 mm | Protège joint. |
| Plan joint | Fraise positive à sec | Pas de boue graphite. |
Ordre pour étanchéité stable
Plan de joint, poche d’huile, portée, rainure spirale puis trous du même datum.
Poussière, rainure et durée
La poussière graphite recoupe et cache les rayures; aspiration sèche, carbure positif et faible porte-à-faux.
Planéité et fuite
MMT, jauge d’alésage, bleu de contact et optique de rainure valident.
FAQ
Pourquoi rainure tard ?
Pour éviter la recoupe du graphite.
Arrosage ?
Non, boue graphite.
Rejet ?
Lèvre ébréchée ou rayure de fuite.
Русский: Инструмент для крышки насоса GG25
Крышка GG25 требует плоскости и непрерывной канавки, хотя чугун режется легко.
Крышка насоса и карбид
| Элемент | Пакет карбида | Контроль |
|---|---|---|
| Спиральная канавка | TiCN фреза 2,5 мм | Форма не следует спирали. |
| Сетка штифтов | Сверло, развертка, тонкая расточка | Меньше повторного резания пыли. |
| Посадка | Тонкая расточка wiper | Круглость. |
| Масляный карман | 6 мм черн. и R4 финиш | Не рвет плоскость. |
| Плоскость прокладки | Позитивная сухая фреза | Без графитовой грязи. |
Порядок для уплотнения
Сначала плоскость прокладки, затем масляный карман, посадка, спиральная канавка и отверстия от одной базы.
Пыль, канавка и ресурс
Графитовая пыль повторно режет и скрывает царапины; применяют сухую вытяжку и позитивный карбид.
Плоскость и утечка
КИМ, нутромер, синька и оптика канавки подтверждают годность.
Вопросы
Почему канавка поздно?
Меньше повторного резания графита.
СОЖ нужна?
Нет, будет графитовая грязь.
Когда брак?
Скол кромки или царапина утечки.