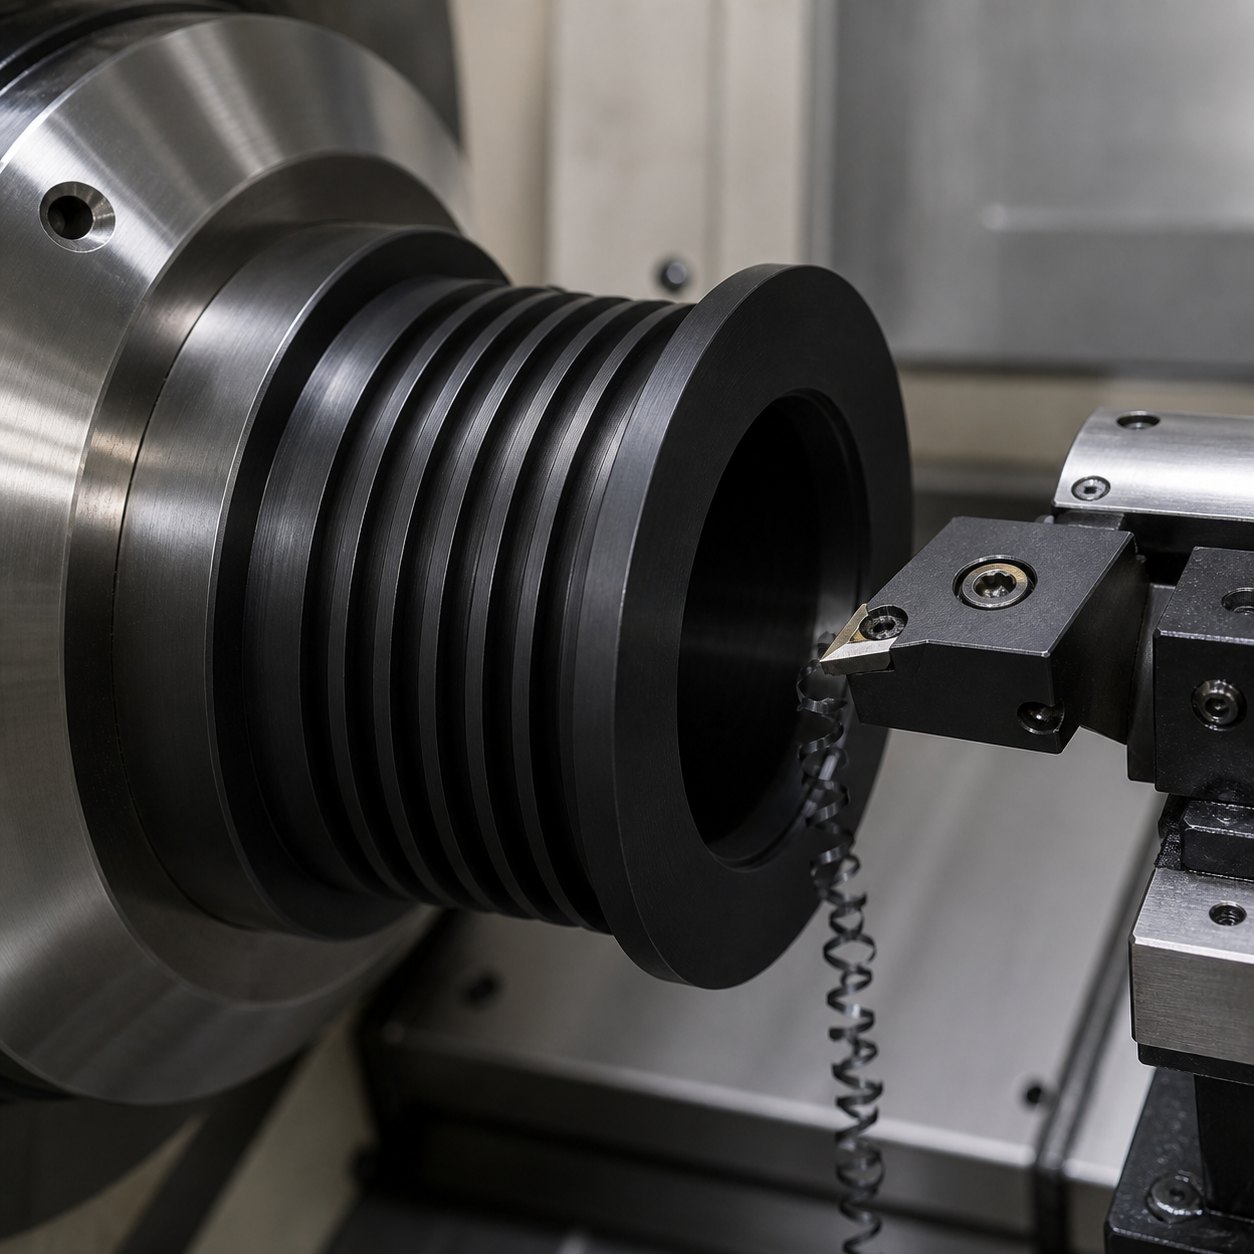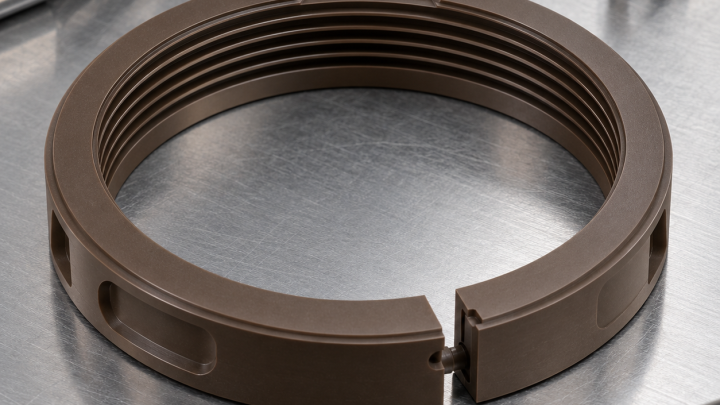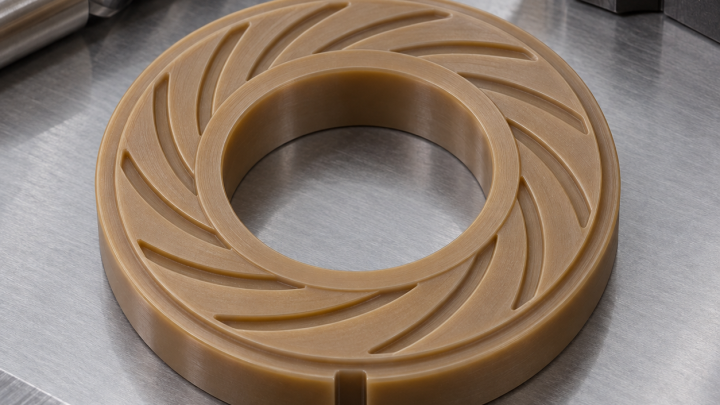
English: POM Cable Drum CNC Tooling Case: Helical Groove, Thin Flange and Burr-Free Cross Bore
This hypothetical case treats a molybdenum heat-shield cup as a bore-stiffness problem: the deep blind bore, 0.8 mm lip and radial cooling holes must all reference the mounting face.
Feature-to-tool selection
| Feature | Tool | Decision |
|---|---|---|
| Blind bore | Ø16 carbide boring bar, 3×D reach, anti-vibration holder | Stiffness prevents taper; long HSS bar chatters. |
| Thin lip | PCD-tipped finish tool, R0.2 | Low force; broad insert rolls the edge. |
| Radial holes | Ø2.5 through-coolant carbide drill | Short chips and position control. |
Face datum A first, rough the bore with constant engagement, then finish the lip while an expanding mandrel supports the wall. Inspect bore axis, lip thickness, burrs and Ra after thermal stabilization.
FAQ
Which grooving tool avoids melting POM?
A polished sharp carbide insert with generous clearance and air cooling, not a dull coated insert.
deep-bore axis control · tool overhang control