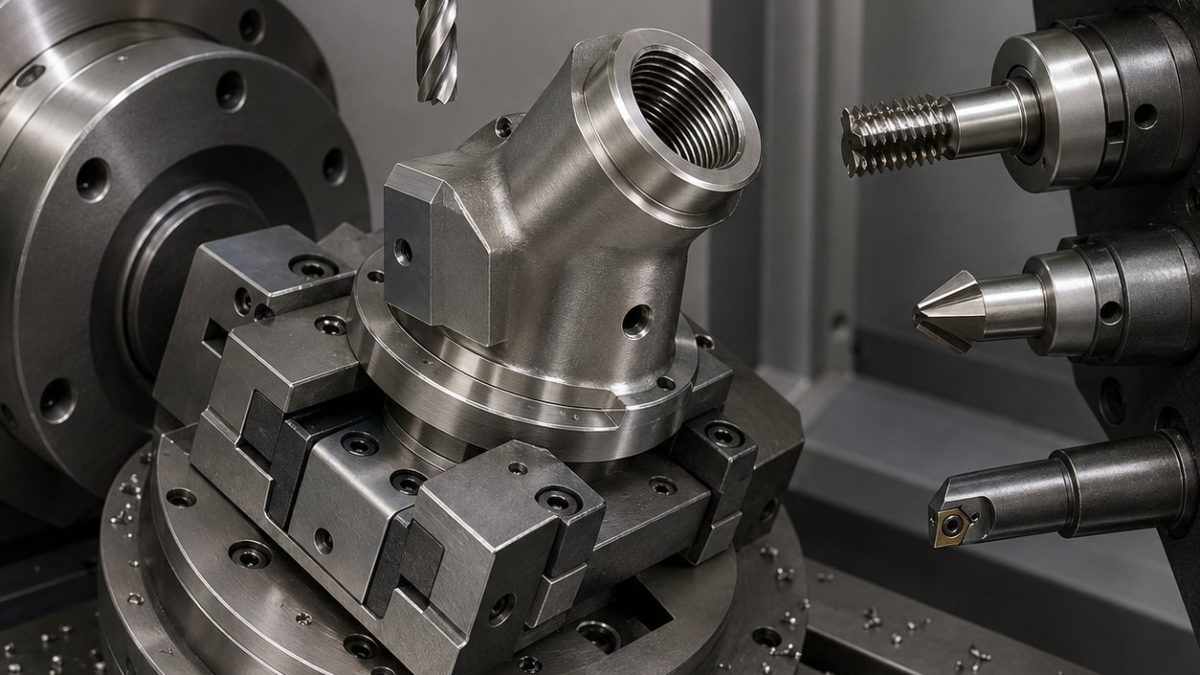
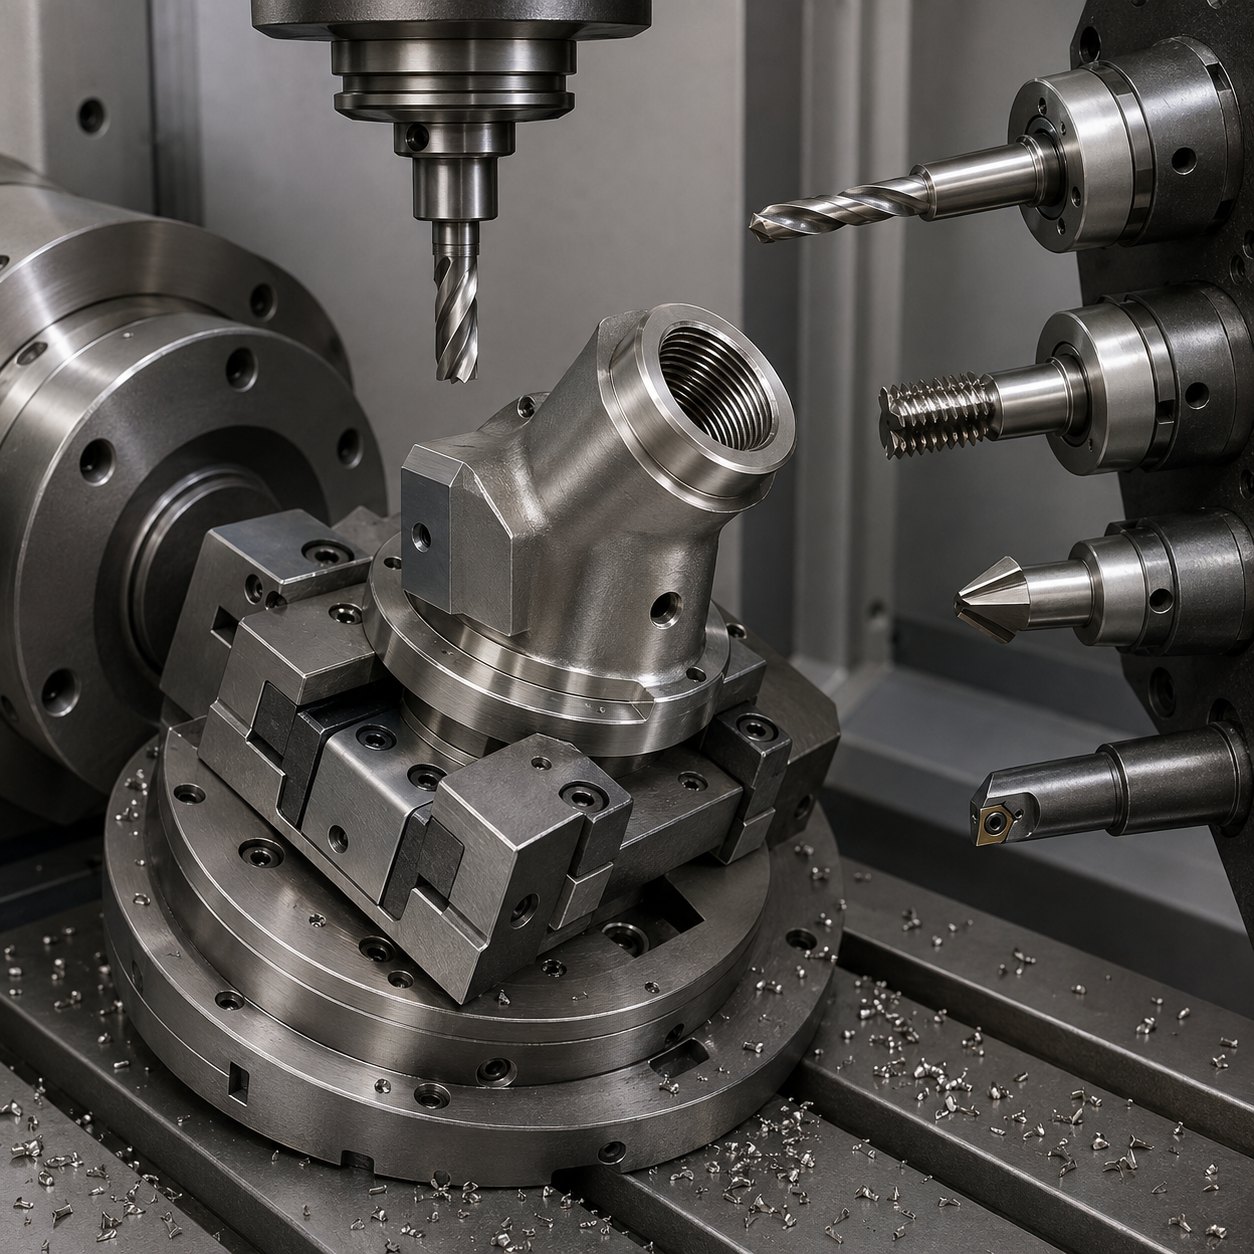
English: A286 Exhaust Sensor Boss CNC Tool Selection for Angled M18 Thread and Washer Land
This case answers a narrow tooling question: how to choose carbide tools for an A286 exhaust gas sensor boss when the drawing combines an angled M18 thread, a crush-washer sealing land, wrench flats and a small cross sampling hole. The process is built around keeping the angled port coaxial while preventing heat-resistant stainless work hardening at the thread start.
Drawing interpretation and process order
Datum A is the mounting flange, datum B is the angled port axis and datum C is one wrench flat. Rough the flange and body first, finish the washer land before thread milling, then drill the cross hole only after the port bore is stable. For related nickel-alloy tool-life logic, see Hastelloy C-276 valve plate tooling and Inconel 718 seal ring distortion control.
Feature-to-tool selection
| Feature | Tool choice | Rationale |
|---|---|---|
| Forged boss skin and flange face | High-positive carbide face mill, AlTiN, medium hone | Positive geometry limits rubbing; a heavy negative rougher is rejected because A286 hardens when it slides. |
| Angled pilot bore | Short carbide drill then indexable micro-boring head in a 5-axis tilted setup | Boring corrects drill walk; a long drill-only process is rejected for thread-axis error. |
| M18 internal thread | Single-profile carbide thread mill, TiAlN, shrink-fit holder | Pitch diameter can be compensated; a tap is rejected because chip packing and torque risk are high. |
| Crush-washer land | Small PCD or polished-carbide circular finisher | Produces a flat bright land; a chamfer tool alone cannot control sealing width. |
| Cross sampling hole and burr break | Carbide stub drill plus back-chamfer tool | Controls intersection burr; hand deburring is rejected inside the hot-gas passage. |
Inspection plan
CMM checks the angled axis to the flange, a thread plug verifies pitch diameter, a height probe checks the washer land, borescope inspection confirms the cross-hole breakout, and surface finish is measured on the sealing land.


