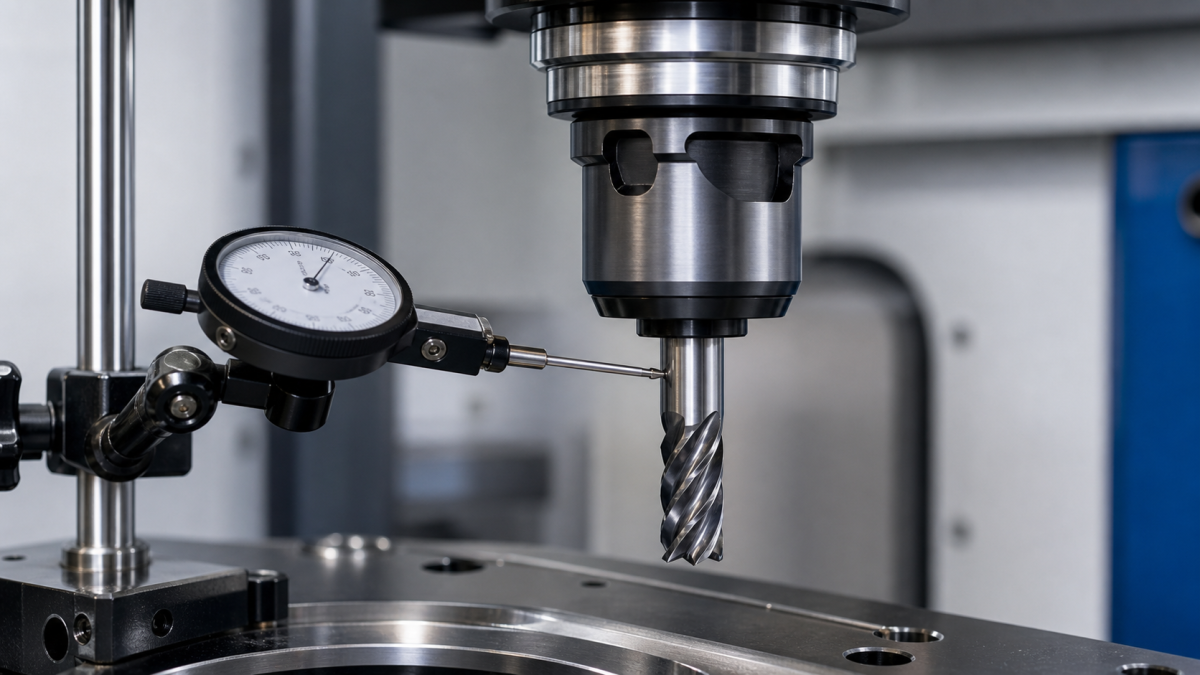
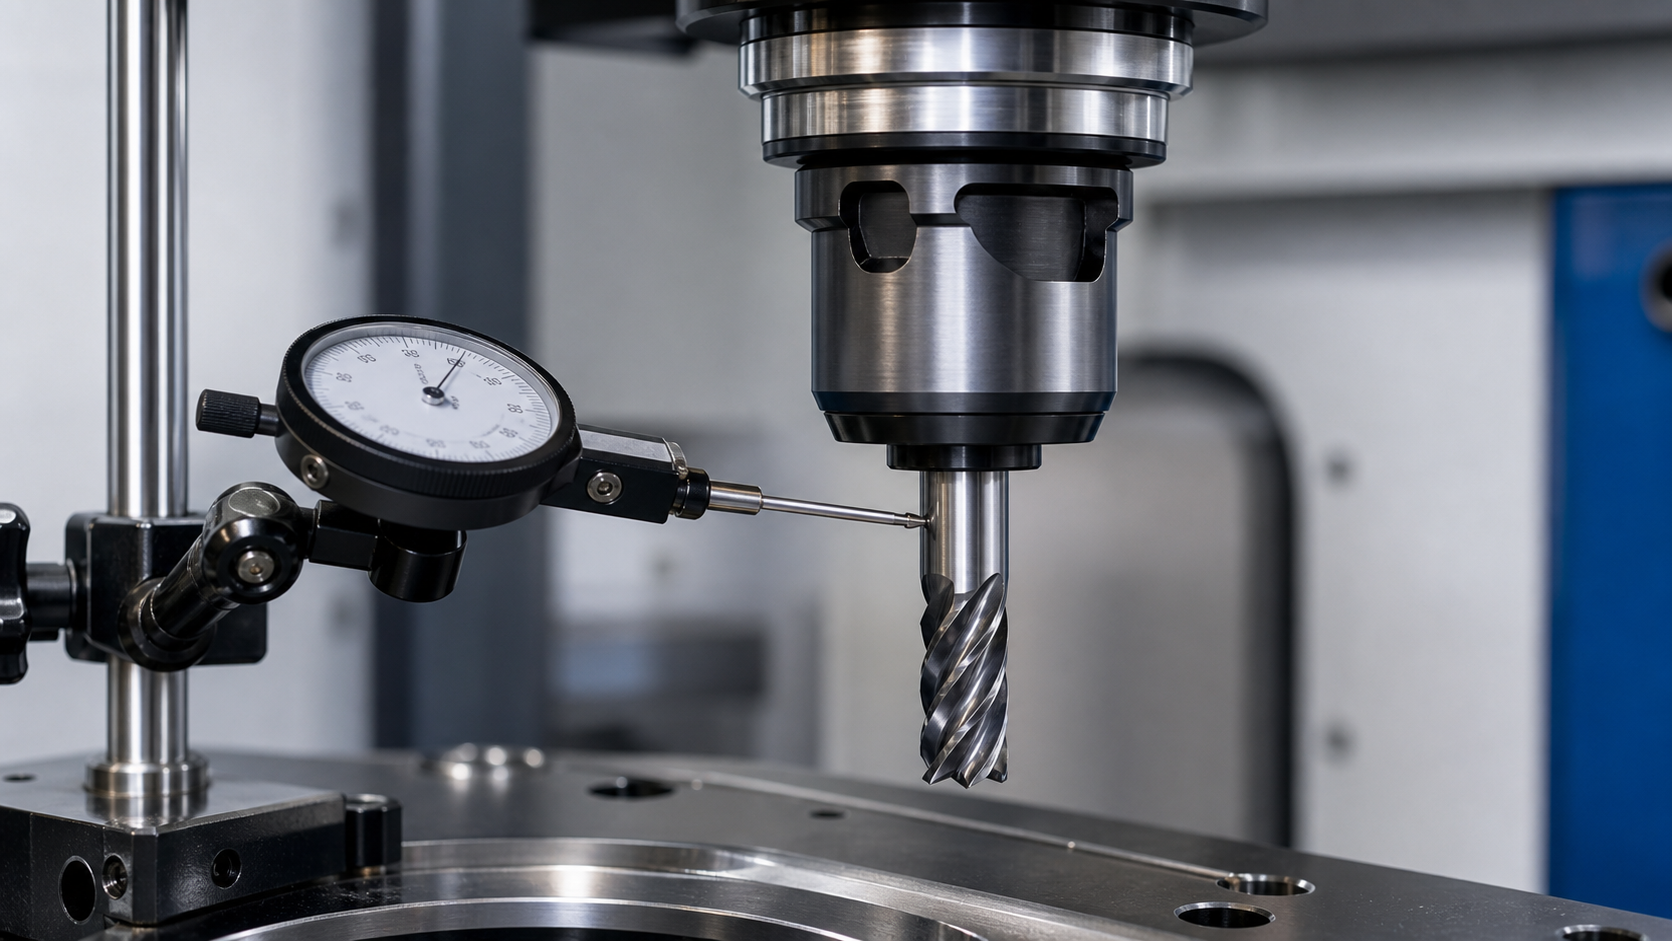
English: High-Speed Aluminum Milling Needs Clean Chip Control
High-speed aluminum CNC milling can deliver excellent productivity, but only when chips leave the cutting zone quickly. Aluminum transfers heat into the chip, so poor evacuation can create built-up edge, surface scratches and unstable tool load. A sharp carbide end mill, polished flute geometry and balanced feed per tooth help maintain a clean cutting action.
Two-flute and three-flute tools are common for aluminum because they provide more flute space for chip removal. Air blast, mist coolant or flood coolant should be selected according to machine enclosure, part geometry and surface finish target. For pocketing, ramping and wall finishing, the programmer should avoid chip recutting and keep tool engagement predictable.
Parameter guidance
Stable workholding, short tool overhang and proper spindle speed matter as much as the tool itself. If the surface becomes smeared, the edge may be dull or the feed may be too low. If vibration appears, reduce stick-out, check holder runout and adjust radial engagement.


