Related tooling references: GG25 Cast Iron Vacuum Pump End Cover CNC Tool Selection for Spiral Seal Groove and Dowel Bore Grid and Delrin AF Rotary Indexing Star Wheel CNC Tool Selection for Ratchet Teeth and Spring Detent Pockets.
English: PPSU Latch Rail Tooling for Snap Hooks and Drain Slots
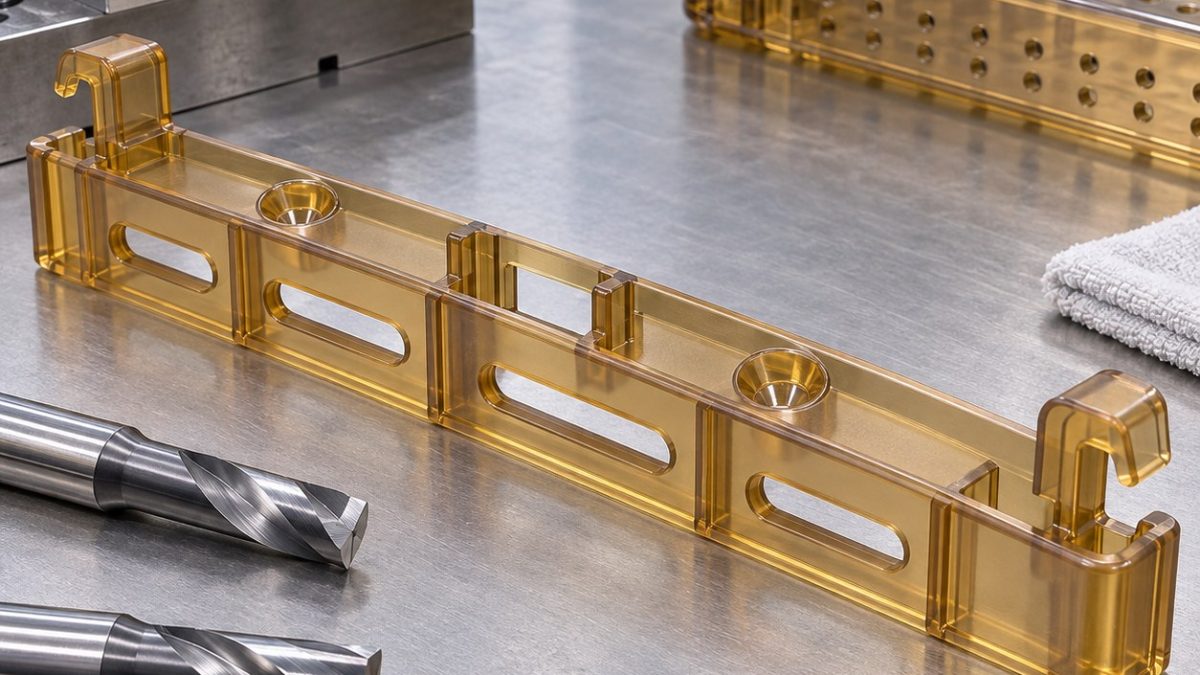
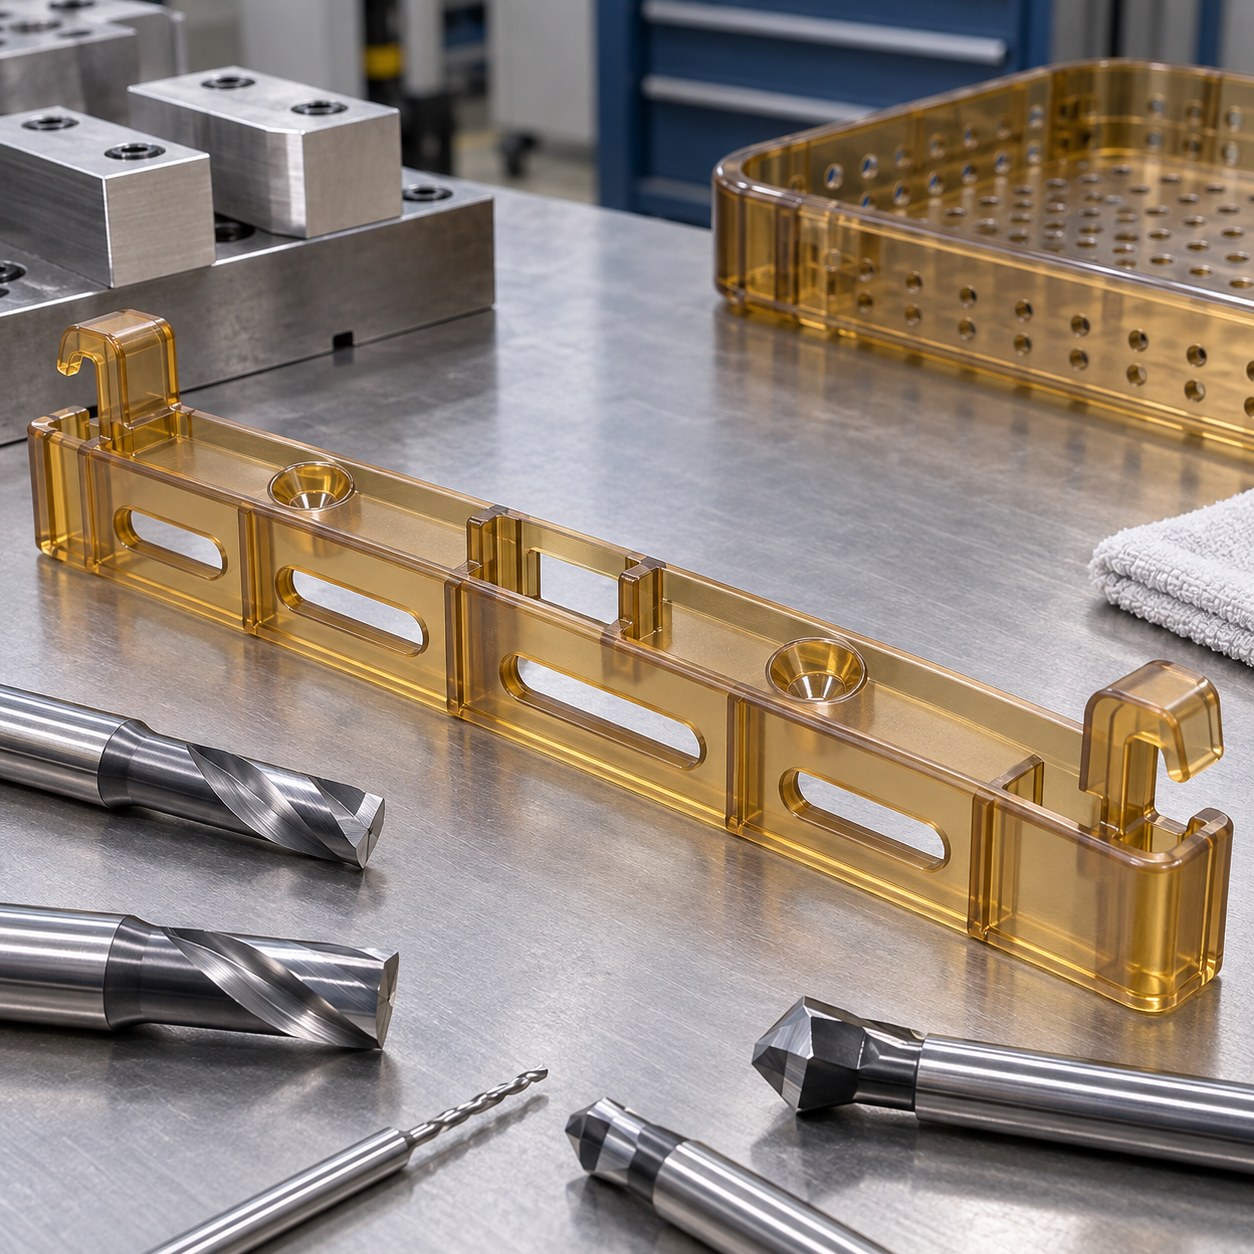
This PPSU sterilization tray latch rail case targets plastic medical-fixture machining: how to choose tools for snap hooks, drain slots and countersunk bosses without whitening transparent amber PPSU. The correct answer is high-rake polished tooling and a fixture that supports the rail before it is released.
PPSU latch rail features mapped to tools
| Plastic feature | Tool choice | Why it protects the part |
|---|---|---|
| Snap hooks | 4 mm polished single-flute carbide end mill with high rake | Shears PPSU cleanly; coated metal roughers create heat and stress whitening. |
| Long drain slots | 3 mm O-flute carbide slot mill and PCD edge pass | Open flute clears warm chips before they weld back to the transparent edge. |
| Countersunk bosses | Carbide drill, piloted countersink, low-friction PCD chamfer | Separate tools hold screw seating without squeezing the boss wall. |
| Latch window | 2 mm polished carbide finisher in balanced holder | Corner radius is protected; punching or aggressive plunging would craze the window edge. |
| Thin ribs and outside rail | 6 mm polished finishing end mill with vacuum support fixture | Finishes after slots while soft support prevents bowing. |
Stable sequence for thin polymer geometry
Machine datum pads and screw bosses first, then open drain slots while the rail still has outside support. Snap hooks and latch windows are finished with small radial cuts, and the outside rail profile is the last cut so the long part cannot bow before final sizing.
PPSU burr, whitening and heat controls
PPSU is tough and heat resistant, but machining heat can create stress marks. Large flute space, air blast, vacuum support and polished edges are used instead of aggressive coated metal cutters. Burr control is a cutting decision, not a scraping step after the part has relaxed.
Sterilization tray rail inspection
Inspection checks slot width, hook flex feel with a reference pin, countersink seating, transparent-edge whitening under light, and rail straightness after unclamping. A part with clean dimensions but visible stress crazing near a hook is not accepted.
PPSU machining FAQ
Why use single-flute tools on PPSU?
They provide chip space and a sharp shearing edge with less heat.
What is the main reject sign?
White stress marks or crazing near snap hooks, even if dimensions are correct.
Can burrs be scraped after machining?
Only minimally; the main burr control must come from tool geometry and support.


