CNC CNC Precision Hub
  • Home
  • Capabilities
  • Articles
  • Contact
Home / Articles / RPMT10T3 Round Inserts for Die-Cavity Roughing and Blends
2026年10月29日 / Carbide Cutting Tools, CNC Tool Selection

RPMT10T3 Round Inserts for Die-Cavity Roughing and Blends

Published: 2026年10月29日 Updated: 2026年10月29日

When RPMT10T3 round inserts suit a die cavity, how depth changes engagement, and why a separate ball-nose cutter still finishes small blends.

RPMT10T3 Round Inserts for Die-Cavity Roughing and Blends

English: RPMT10T3 Round Inserts for Die-Cavity Roughing and Blends
RPMT10T3 Round Inserts for Die-Cavity Roughing and Blends

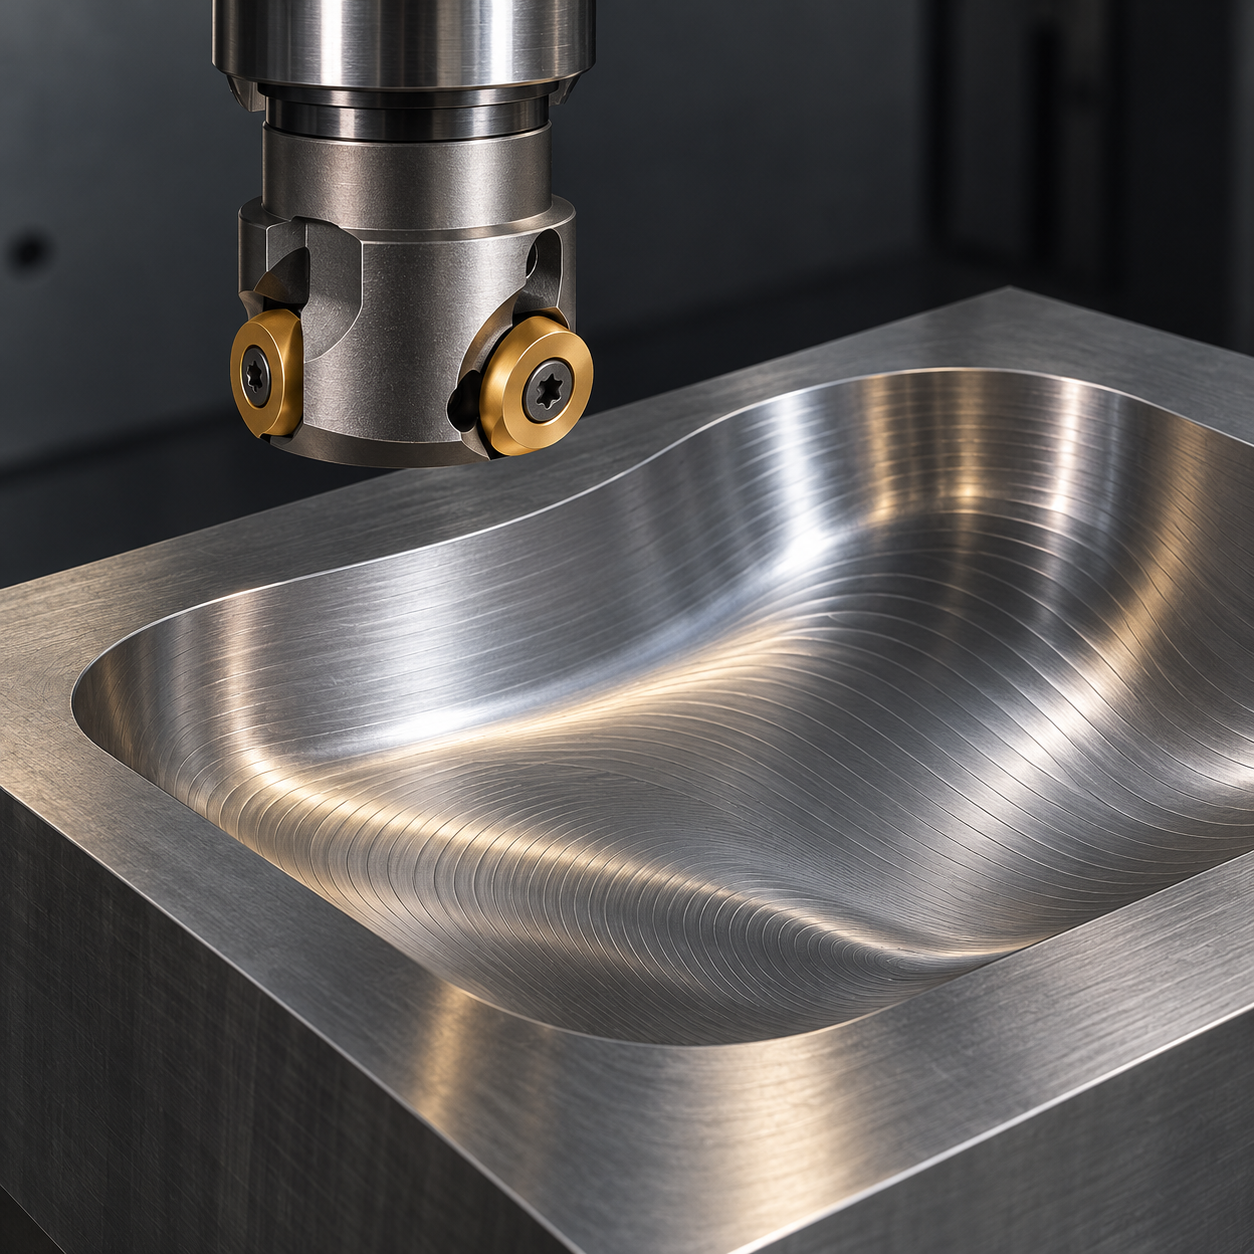
RPMT10T3 round inserts are worth considering when a cavity has generous blends and needs a strong, indexable roughing edge. They are not a shortcut to sharp shoulders or an automatically finished 3D surface. Our hypothetical prehardened P20 die support, 30–34 HRC, contains a shallow basin 14 mm deep with broad R12 transitions and a local R3 blend. The round-insert cutter removes the open volume; a smaller ball-nose tool owns the R3 area.

Depth changes the edge that is actually cutting

A round edge presents a changing effective entering angle as axial depth and surface slope change. Consequently a feed that behaves well on the shallow basin can overload an ascending wall. The insert diameter is not the tool’s cutting diameter, and neither number alone gives the effective diameter at contact. Use the actual assembled tool in CAM, including the body, screw envelope and permitted ramp angle. Check the precise RPMT10T3 variant, seat and clamping details; similar-looking round inserts need not have identical locating features.

A tool map based on accessible curvature

Area Proposed tool Why this division matters
Broad basin roughing Ø25, two-tooth round-insert copy mill for RPMT10T3; tough PVD-coated carbide for prehardened steel, medium positive geometry and controlled hone. Short rigid holder and open chip pockets take priority over adding teeth.
R12 transition semifinish Same verified round tool with fresh edge sectors, shallow controlled levels and consistent normal stock. Increasing depth to save passes increases engaged arc and load.
R3 local blend Ø6, two-flute coated carbide ball nose, fine-grain substrate, short reach in precision collet or shrink holder rated for the shank. A Ø10 round insert is not a Ø6 ball; rough-tool compensation cannot create the small concavity.
Top edge break Ø8, two-flute 90° carbide chamfer mill. Remove exposed burrs without touching the designed basin blend.

Plan for uniform finishing stock, not the fewest Z levels

Support the die block on ground parallels and clamp outside the cavity. Start from open stock or a manufacturer-approved entry; do not assume a button cutter can drill. Rough with modest engagement, leave a trial 0.30 mm normal allowance and simulate remaining stock. Semifinish the steep-to-shallow transition before ball-nose finishing so the small tool never encounters a hidden ridge.

Determine speed and tooth feed from the exact insert grade and effective contact geometry. Chip thinning compensation must stop where engagement rises; a blanket feed multiplier is unsafe. Consistent chip removal prevents hard fragments from being rolled into the basin. Inspect the round edge by marked sectors and index only to an undamaged sector as the maker permits. Never assume an unlimited number of usable positions or rotate across a locating feature.

Inspect shape before polishing

The example calls for profile deviation within 0.05 mm and Ra 1.6 μm on the final basin. Measure sections through the transition and the R3 blend, not only the easy floor. Set ball-nose stepover from acceptable cusp height and verify the actual texture; a theoretical cusp value is not a roughness certificate. Polishing must not erase evidence of a gouge. Compare ball-nose stepover planning and corner-radius strength tradeoffs.

Round-insert FAQ

Does a round insert make a flat floor? It can machine a floor with the appropriate toolpath and assembly, but finish and residual geometry must be checked; it is not a universal face-finishing substitute.

Should feed increase whenever depth becomes shallow? Only within verified grade, engagement, spindle and machine limits. Entry, corners and rising slopes require separate evaluation.

Manufacturer reference: dimensions and system compatibility.

Turn this technical topic into a project solution

If you have a similar CNC machining, material, tolerance, surface finish, fixture, tool-life or batch stability problem, send the project details for a practical review.

Send Project Details
Tags: Copy Milling Die Cavity Roughing Radial Engagement Round Insert Milling RPMT10T3 Inserts
Previous: R390 11T3 Inserts: Corner Radius for Square-Shoulder Finishing
Next: SEKT1204 Inserts for 45-Degree Face Milling: Pads and Flatness

Need a CNC technical solution?

Send drawings, material, current machining issue and production target. We can review process, tooling, fixtures, inspection and delivery control.

Request Solution Review

Article Topics

CNC milling, turning, tool life, fixture design, inspection standards, surface finishing and supply-chain support.

近期文章

  • TPKN2204 Triangular Inserts: Match the Shoulder-Mill Body
  • APGT1604 Aluminum Inserts for Thin Ribs and Clean Chip Flow
  • LNMU0303 High-Feed Inserts: CAM Radius and Finishing Stock
  • SEKT1204 Inserts for 45-Degree Face Milling: Pads and Flatness
  • RPMT10T3 Round Inserts for Die-Cavity Roughing and Blends

近期评论

  1. Ti-6Al-4V Aerospace Bracket Tooling for Thin Ribs and Heat Control - CNC Precision Hub 发表在 Drawing-Based Tool Selection Case: Aluminum Bracket CNC Machining Plan
  2. Zirconium 702 Pump Wear Plate CNC Tooling Case: Kidney Ports and Seal Grooves - CNC Precision Hub 发表在 Carbide End Mill Cutting Parameters by Material, Geometry and Engagement
  3. Carbide End Mill Cutting Parameters by Material, Geometry and Engagement - CNC Precision Hub 发表在 Carbide End Mill Edge Preparation: Micro Honing for Longer Tool Life
  4. Deep Pocket Milling Tooling Hub: Reach, Chip Evacuation and Stock Control - CNC Precision Hub 发表在 RPMT10T3 Round Inserts for Die-Cavity Roughing and Blends
  5. Feed per Tooth in CNC Milling: Chip Load, Radial Thinning and Runout - CNC Precision Hub 发表在 APMT1135 Insert Selection for Small-Diameter Pocket Milling

归档

  • 2026 年 10 月
  • 2026 年 9 月
  • 2026 年 8 月
  • 2026 年 7 月

分类

  • 13-8Mo Stainless Machining
  • 17-4PH Stainless Machining
  • 410 Stainless Steel Machining
  • 42CrMo4 Machining
  • 440C Stainless Machining
  • 6061 Aluminum Machining
  • A286 Stainless Machining
  • ADI Ductile Iron Machining
  • Aerospace Machining
  • AL-6XN Machining
  • Alloy 20 Machining
  • Alloy Steel Machining
  • Alumina Ceramic Machining
  • Aluminum Machining
  • Aluminum Nitride Machining
  • AM 316L Stainless Machining
  • Automotive Machining
  • Bearing Machining
  • Bronze Machining
  • C11000 OFE Copper Machining
  • C14500 Tellurium Copper Machining
  • C26000 Cartridge Brass Machining
  • C360 Brass Machining
  • C63000 Nickel Aluminum Bronze Machining
  • C65500 Silicon Bronze Machining
  • C70600 Copper Nickel Machining
  • C71500 Copper-Nickel Machining
  • Carbide Cutting Tools
  • Case Studies
  • Cast Iron Machining
  • Ceramic Machining
  • CNC Case Studies
  • CNC Cutting Tools
  • CNC Machining
  • CNC Machining Case Studies
  • CNC Machining Guides
  • CNC Tool Selection
  • CNC Tooling Case Studies
  • CNC Tooling Cases
  • CoCrMo Machining
  • Composite Machining
  • Compressor Machining
  • Copper Alloy Machining
  • CuCrZr Machining
  • Cutting Tools
  • Delrin AF Machining
  • Drawing-Based Tool Selection
  • Engineering Plastic Machining
  • Engineering Plastics Machining
  • ETFE Machining
  • FR4 Laminate Machining
  • Free-Machining Steel
  • G10 Epoxy Glass Machining
  • GG25 Cast Iron Machining
  • Graphite Machining
  • H13 Tool Steel Machining
  • Hardened D2 Machining
  • Hardfacing Machining
  • Hastelloy B-3 Machining
  • Hastelloy C-276 Machining
  • Haynes 230 Machining
  • Heavy Equipment Machining
  • High-Temperature Alloy Machining
  • Hydraulic Machining
  • Inconel 625 Machining
  • Inconel 718 Machining
  • Inconel X-750 Machining
  • Invar 36 Machining
  • Kovar Machining
  • Machining Case Studies
  • Magnesium Machining
  • Magnetic Component Machining
  • MAR-M247 Machining
  • Maraging Steel Machining
  • Medical Machining
  • Metal Matrix Composite Machining
  • Molybdenum Copper Machining
  • Molybdenum Machining
  • Monel 400 Machining
  • Monel K-500 Machining
  • NAK80 Mold Steel Machining
  • Nickel 200 Machining
  • Nickel Alloy Machining
  • Nickel Silver Machining
  • Nitronic 60 Machining
  • Noryl PPO Machining
  • PA66-GF30 Machining
  • PCTFE Machining
  • PEEK-CF30 Machining
  • PEEK-GF30 Machining
  • PEI Ultem Machining
  • PEKK Machining
  • Plastic Machining
  • Polycarbonate Machining
  • PPS-GF40 Machining
  • PPSU Machining
  • Precision Machining
  • Precision Micromachining
  • PVDF Machining
  • Rene 41 Machining
  • S32760 Super Duplex Machining
  • Shape Memory Alloy Machining
  • Stainless Steel Machining
  • Tantalum Machining
  • Ti-6Al-7Nb Machining
  • Titanium CNC Machining
  • Titanium Machining
  • Tool Steel Machining
  • Tooling Case Studies
  • Torlon 4203 Machining
  • Tungsten Alloy Machining
  • UHMWPE Machining
  • Vacuum and RF Machining
  • Valve Body Machining
  • ZA-27 Zinc Alloy Machining
  • Zerodur Machining
  • Zirconium Machining
  • 未分类

Related Articles

Continue reading CNC machining technology, tooling configuration and supporting solutions.

TPKN2204 Triangular Inserts: Match the Shoulder-Mill Body
2026年10月29日 / CNC Tool Selection, Drawing-Based Tool Selection

TPKN2204 Triangular Inserts: Match the Shoulder-Mill Body

TPKN2204三角铣刀片怎么配刀:刀盘压板、刀座与台阶加工

Select TPKN2204 triangul…

APGT1604 Aluminum Inserts for Thin Ribs and Clean Chip Flow
2026年10月29日 / Aluminum Machining, CNC Tool Selection

APGT1604 Aluminum Inserts for Thin Ribs and Clean Chip Flow

APGT1604铝用刀片怎么选:薄筋铣削、锋利刃口与排屑

Choose polished APGT1604…

LNMU0303 High-Feed Inserts: CAM Radius and Finishing Stock
2026年10月29日 / Carbide Cutting Tools, CNC Tool Selection

LNMU0303 High-Feed Inserts: CAM Radius and Finishing Stock

LNMU0303高进给刀片配刀:虚拟圆角、浅切深和精加工余量

Select LNMU0303 high-fee…

Manufacturing Support

Need CNC machining and support planning?

Send drawings, material, and quantity requirements. We can help review process, tooling, fixtures, inspection, and delivery options.

Get Machining Advice
CNC CNC Precision Hub

Focused on precision CNC machining, tooling systems, fixtures, quality inspection, and finishing support to make prototypes and production more stable.

Capabilities

CNC milling and turning Tool holders, tools, and fixtures Inspection, heat treatment, finishing

Article Topics

CNC machining technology Tool life and cutting data Supporting solutions

© 2026 CNC Precision Hub. CNC machining technology and tooling support.

