Related tooling references: GG25 Cast Iron Vacuum Pump End Cover CNC Tool Selection for Spiral Seal Groove and Dowel Bore Grid and Delrin AF Rotary Indexing Star Wheel CNC Tool Selection for Ratchet Teeth and Spring Detent Pockets.
English: PPSU Latch Rail Tooling for Snap Hooks and Drain Slots
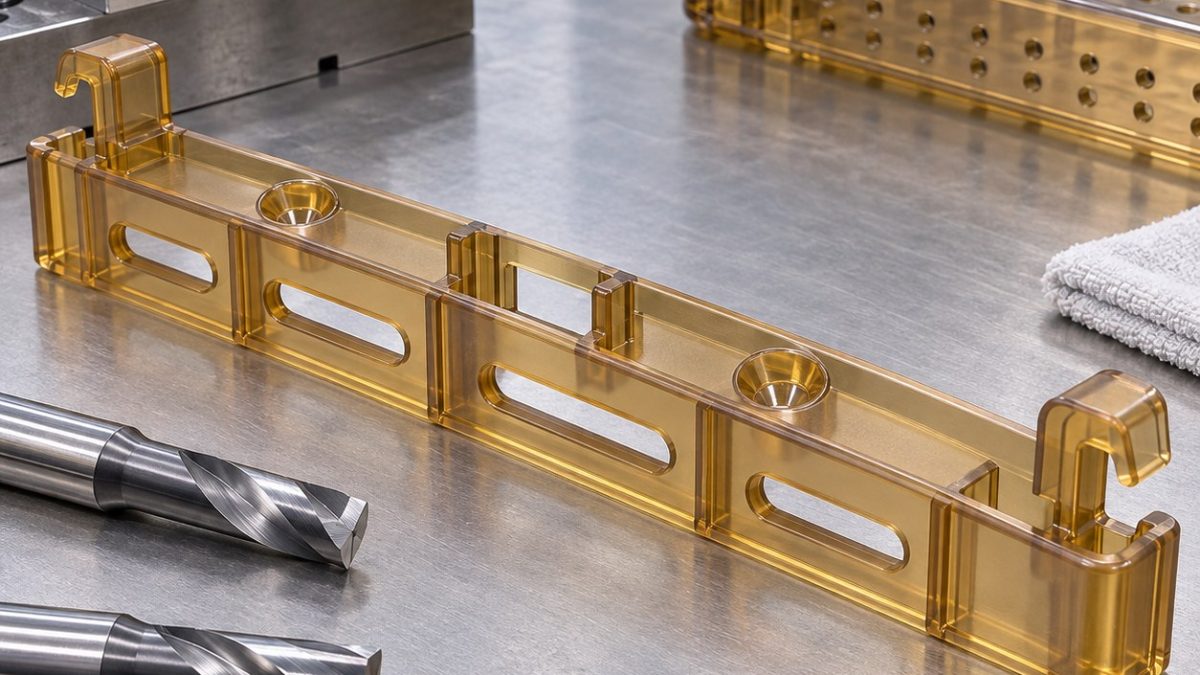
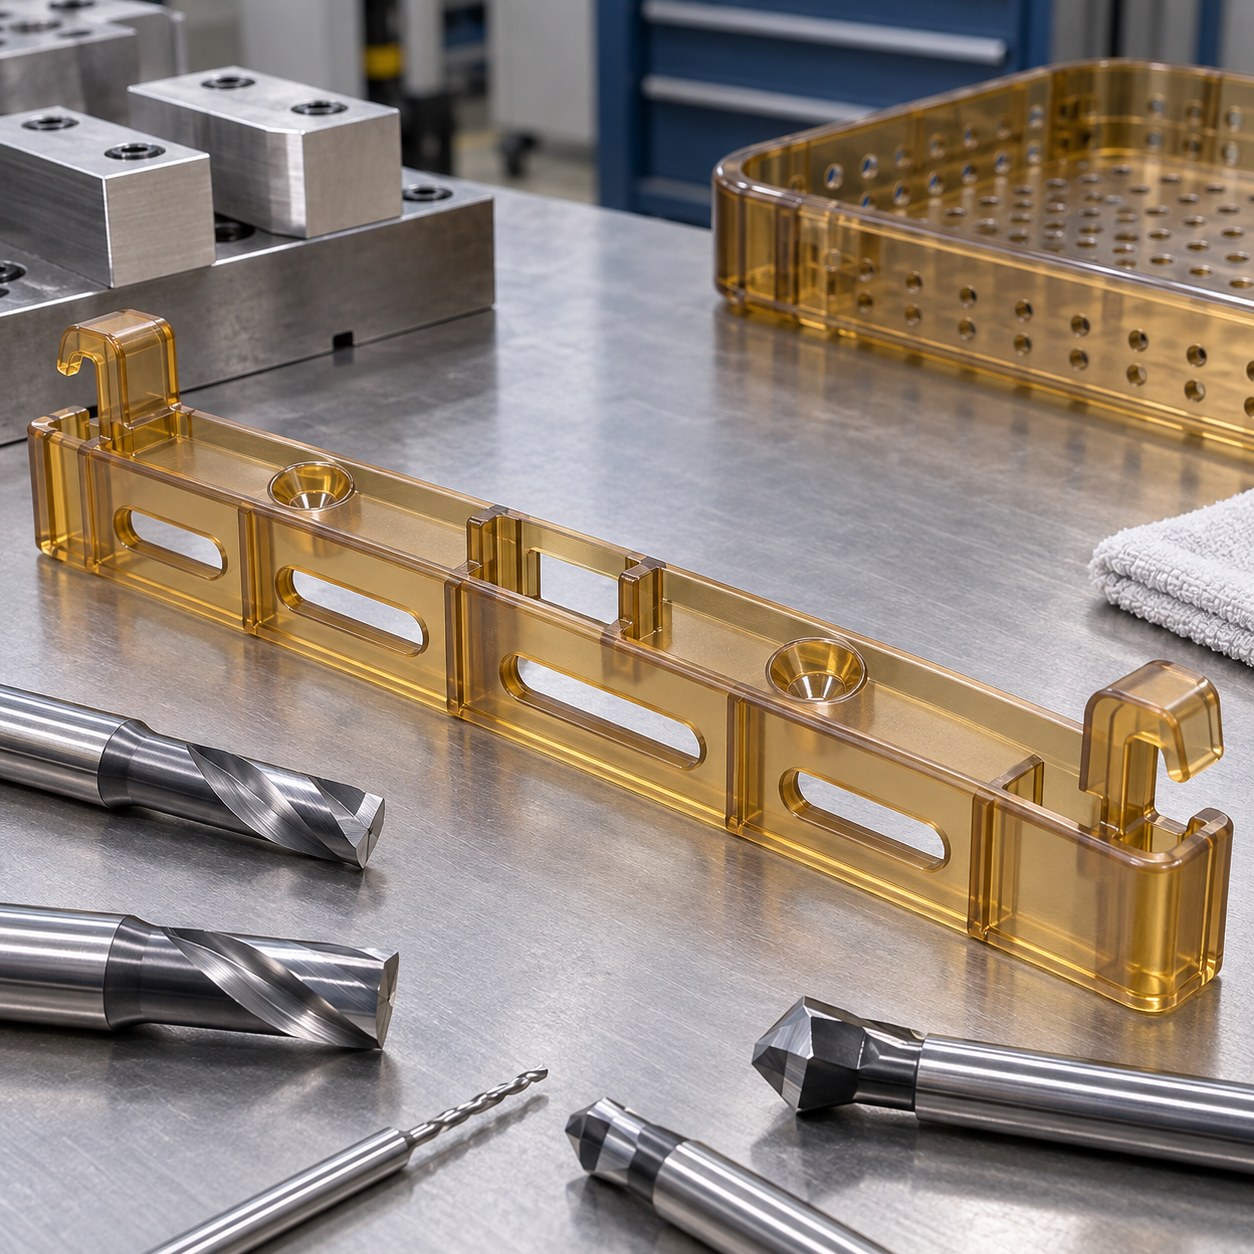
This PPSU sterilization tray latch rail case targets plastic medical-fixture machining: how to choose tools for snap hooks, drain slots and countersunk bosses without whitening transparent amber PPSU. The correct answer is high-rake polished tooling and a fixture that supports the rail before it is released.
PPSU latch rail features mapped to tools
| Plastic feature | Tool choice | Why it protects the part |
|---|---|---|
| Snap hooks | 4 mm polished single-flute carbide end mill with high rake | Shears PPSU cleanly; coated metal roughers create heat and stress whitening. |
| Long drain slots | 3 mm O-flute carbide slot mill and PCD edge pass | Open flute clears warm chips before they weld back to the transparent edge. |
| Countersunk bosses | Carbide drill, piloted countersink, low-friction PCD chamfer | Separate tools hold screw seating without squeezing the boss wall. |
| Latch window | 2 mm polished carbide finisher in balanced holder | Corner radius is protected; punching or aggressive plunging would craze the window edge. |
| Thin ribs and outside rail | 6 mm polished finishing end mill with vacuum support fixture | Finishes after slots while soft support prevents bowing. |
Stable sequence for thin polymer geometry
Machine datum pads and screw bosses first, then open drain slots while the rail still has outside support. Snap hooks and latch windows are finished with small radial cuts, and the outside rail profile is the last cut so the long part cannot bow before final sizing.
PPSU burr, whitening and heat controls
PPSU is tough and heat resistant, but machining heat can create stress marks. Large flute space, air blast, vacuum support and polished edges are used instead of aggressive coated metal cutters. Burr control is a cutting decision, not a scraping step after the part has relaxed.
Sterilization tray rail inspection
Inspection checks slot width, hook flex feel with a reference pin, countersink seating, transparent-edge whitening under light, and rail straightness after unclamping. A part with clean dimensions but visible stress crazing near a hook is not accepted.
PPSU machining FAQ
Why use single-flute tools on PPSU?
They provide chip space and a sharp shearing edge with less heat.
What is the main reject sign?
White stress marks or crazing near snap hooks, even if dimensions are correct.
Can burrs be scraped after machining?
Only minimally; the main burr control must come from tool geometry and support.
中文: PPSU灭菌托盘锁扣导轨卡钩与排水槽配刀
这个PPSU灭菌托盘锁扣导轨案例针对医用夹具塑料加工:如何在不让透明琥珀色PPSU白化的前提下,为卡钩、排水槽和沉头柱配刀。正确方向是大前角抛光刀具和释放前充分支撑的夹具。
PPSU锁扣导轨特征到刀具
| 塑料特征 | 刀具选择 | 如何保护零件 |
|---|---|---|
| 弹性卡钩 | 4 mm抛光单刃大前角硬质合金刀 | 干净剪切PPSU;金属粗刀会发热并造成应力白化。 |
| 长排水槽 | 3 mm O刃硬质合金槽刀和PCD修边 | 开口槽及时排出热屑,避免重新粘回透明边。 |
| 沉头安装柱 | 硬质合金钻、导向沉头刀、低摩擦PCD倒角刀 | 分刀控制螺钉座面,不挤压柱壁。 |
| 锁扣窗口 | 2 mm抛光硬质合金精刀,动平衡刀柄 | 保护窗口圆角;冲切或重插铣会使边缘开裂。 |
| 薄筋和外导轨 | 6 mm抛光精铣刀,真空支撑夹具 | 开槽后精修外形,软支撑防止翘曲。 |
薄壁聚合物结构的稳定顺序
先加工基准垫和螺钉柱,再在外形仍有支撑时打开排水槽。卡钩和锁扣窗口用小径向切深精修,外导轨轮廓最后切断,避免长零件在最终定尺寸前翘曲。
PPSU毛刺、白化和热量控制
PPSU韧性高且耐热,但加工热仍会产生应力痕。大排屑槽、气冷、真空支撑和抛光刃口优先于金属用重切涂层刀。毛刺控制是切削选择,不是零件释放后的刮修步骤。
灭菌托盘导轨检测
检测排水槽宽、用参考销感受卡钩弹性、沉头座面、灯光下透明边白化,以及松夹后的导轨直线度。尺寸合格但卡钩附近有应力裂纹迹象的零件不接受。
PPSU加工问答
PPSU为什么用单刃刀?
单刃有排屑空间和锋利剪切刃,热量更少。
主要拒收信号是什么?
卡钩附近出现白化或细裂,即使尺寸合格也拒收。
毛刺能加工后刮掉吗?
只能少量修整;主要毛刺控制必须来自刀具几何和支撑。
Español: Herramientas para riel PPSU con ganchos
El riel PPSU busca ganchos y drenajes limpios sin blanqueo. La respuesta es carburo pulido, PCD donde conviene y soporte antes de liberar.
Riel PPSU y selección de herramienta
| Elemento plástico | Herramienta | Protección |
|---|---|---|
| Ganchos | Fresa pulida mono-labio 4 mm | Corta sin blanquear. |
| Ranuras drenaje | O-flute 3 mm y PCD | Evacua viruta caliente. |
| Jefes avellanados | Broca, avellanador piloto y PCD | No comprime pared. |
| Ventana | Fresa pulida 2 mm | Protege radio. |
| Riel exterior | Fresa pulida 6 mm con apoyo | Evita arqueo. |
Secuencia para geometría fina
Bosses primero, ranuras con soporte exterior, ganchos con corte ligero y perfil exterior al final.
Rebaba, blanqueo y calor
PPSU marca por calor; se usa gran evacuación, aire, vacío y filo muy pulido.
Inspección del riel
Se revisa ancho, flexión de gancho, asiento de tornillo, blanqueo bajo luz y rectitud.
FAQ PPSU
¿Por qué mono-labio?
Más espacio de viruta y menos calor.
¿Principal rechazo?
Blanqueo o grieta en gancho.
¿Raspar rebaba?
Solo mínimo; debe cortarse bien.
Français: Outils pour rail PPSU à crochets
Le rail PPSU demande crochets et fentes propres sans blanchiment. Il faut carbure poli, PCD si utile et support avant libération.
Rail PPSU et choix d’outil
| Élément plastique | Outil | Protection |
|---|---|---|
| Crochets | Fraise polie mono-dent 4 mm | Coupe sans blanchir. |
| Fentes drainage | O-flute 3 mm et PCD | Évacue copeau chaud. |
| Bossages fraisés | Foret, fraisoir guidé et PCD | Ne comprime pas. |
| Fenêtre | Fraise polie 2 mm | Protège le rayon. |
| Rail extérieur | Fraise polie 6 mm avec support | Évite le cintrage. |
Séquence pour géométrie fine
Bossages d’abord, fentes avec appui extérieur, crochets en coupe légère puis profil final.
Bavure, blanchiment et chaleur
Le PPSU marque à chaud; grandes goujures, air, vide et arête polie sont prioritaires.
Contrôle du rail
Contrôle largeur, flexion du crochet, siège vis, blanchiment à la lumière et rectitude.
FAQ PPSU
Pourquoi mono-dent ?
Plus de place copeau et moins de chaleur.
Rejet principal ?
Blanchiment ou crique au crochet.
Gratter la bavure ?
Très peu; il faut bien couper.
Русский: Инструмент для рейки PPSU
Рейка PPSU требует чистых защелок и пазов без побеления. Нужны полированный карбид, PCD по месту и опора до освобождения.
Рейка PPSU и инструмент
| Пластиковый элемент | Инструмент | Защита детали |
|---|---|---|
| Защелки | Полированная однозубая 4 мм | Режет без побеления. |
| Дренажные пазы | O-flute 3 мм и PCD | Выводит горячую стружку. |
| Зенкованные бобышки | Сверло, зенковка и PCD | Не сжимает стенку. |
| Окно | Полированная 2 мм | Защищает радиус. |
| Наружная рейка | Полированная 6 мм с опорой | Предотвращает изгиб. |
Порядок для тонкой геометрии
Сначала бобышки, затем пазы при внешней опоре, защелки малым резом и наружный профиль в конце.
Заусенец, побеление и тепло
PPSU белеет от тепла; важны большие канавки, воздух, вакуумная опора и полированная кромка.
Контроль рейки
Проверяют ширину, гибкость защелки, посадку винта, побеление на свету и прямолинейность.
Вопросы PPSU
Почему один зуб?
Больше место стружке и меньше тепло.
Главный брак?
Побеление или трещина у защелки.
Можно скоблить?
Минимально; заусенец надо срезать инструментом.