Related tooling references: Hardened D2 Trim Die Stripper Plate CNC Tool Selection for Slug Windows and Guided Punch Bores and Aluminum Nitride Power Module Carrier CNC Tool Selection for Isolation Pockets and Fragile Ribs.
English: Delrin AF Star Wheel Tooling for Ratchet Teeth and Detent Pockets
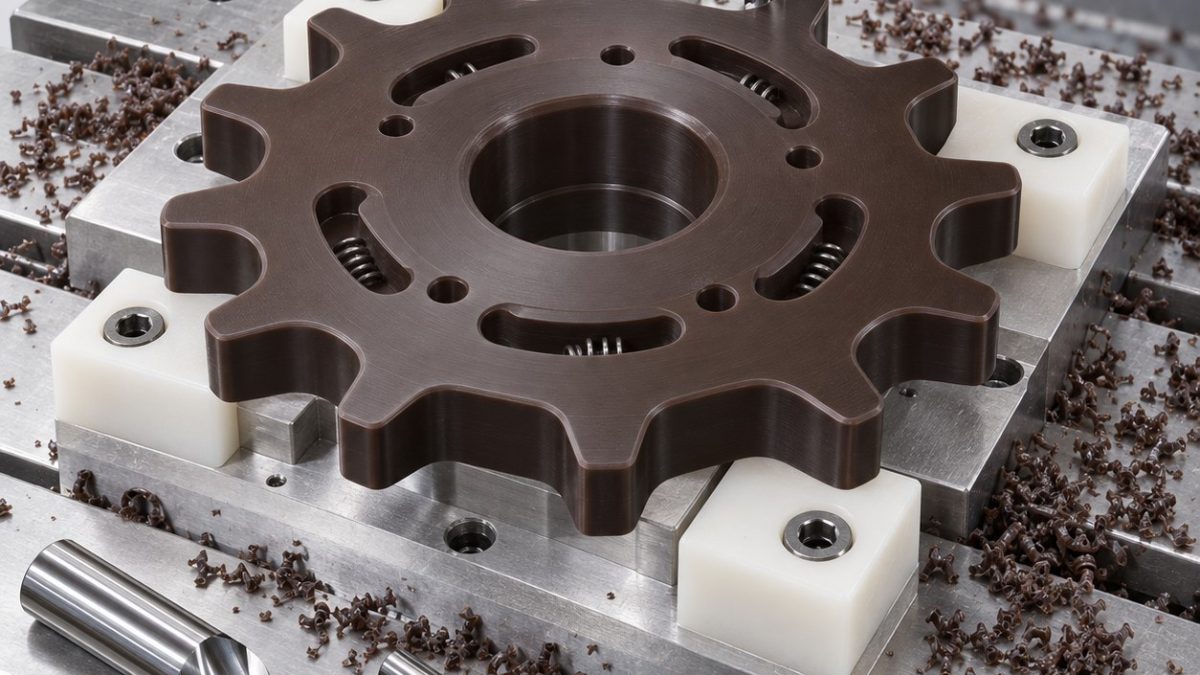
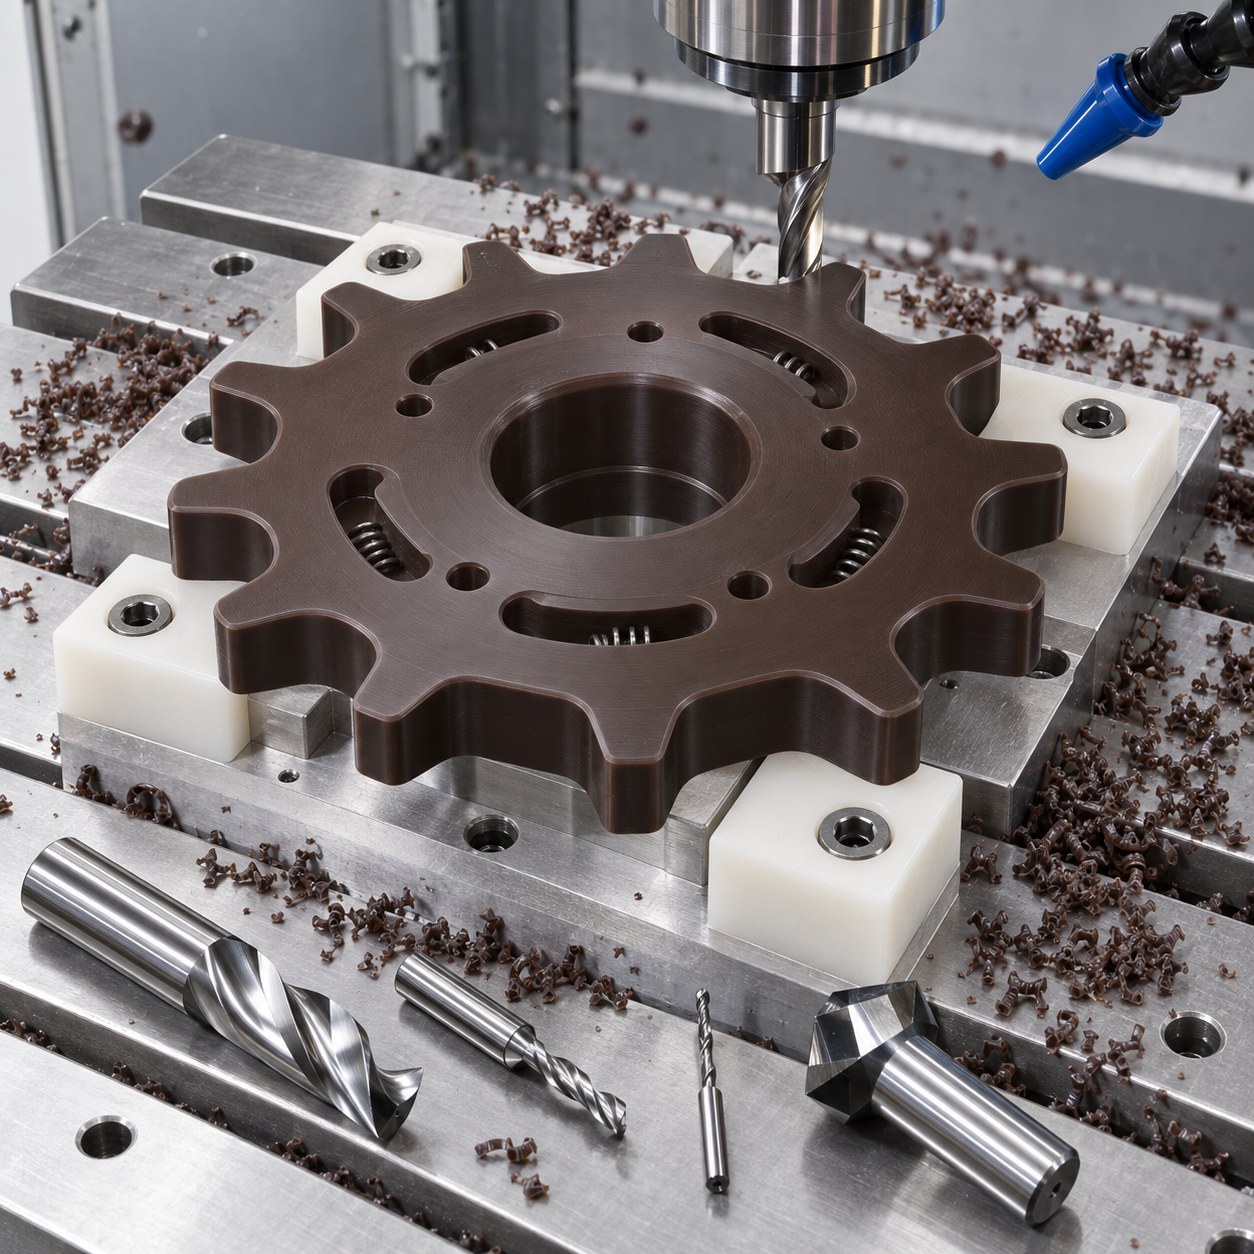
This Delrin AF star wheel case focuses on drawing-based tool choice for ratchet teeth, detent pockets and a hub bore in PTFE-filled acetal. The search intent is not simply plastic milling; it is how to keep indexing edges sharp without whitening, fuzz or pitch error.
Star wheel features converted into polymer tooling
| Drawing feature | Chosen polished tool | Reason for the choice |
|---|---|---|
| Ratchet teeth | 3 mm single-flute polished carbide, sharp uncoated edge, air blast | Coated metal cutters are rejected because edge radius smears PTFE-filled acetal. |
| Spring detent pockets | 2 mm PCD ball nose, shallow raster | A drill-point pocket would create a notch that traps the spring tip. |
| Central hub bore | 8 mm polished carbide boring bar after helical roughing | A reamer can bell-mouth soft polymer if chips pack. |
| Dowel holes | Carbide brad-point drill and light hand-free chamfer toolpath | Twist drill breakout is rejected for exit fuzz. |
| Outer indexing relief | 4 mm O-flute finisher | Protects tooth pitch while removing support tabs. |
Process order that prevents tooth deflection
Machine the hub and dowel pattern first while the blank is round and well supported, leave tooth stock until the bore is stable, then finish ratchet teeth in light climb passes. Detent pockets are finished before final outside release so spring force will land on a clean radius instead of a drilled notch.
Delrin AF chip, burr and heat control
Delrin AF tolerates speed but dislikes heat trapped by dull edges. Polished carbide and PCD are chosen for shearing, while coated steel-style cutters are rejected when their edge prep pushes material. Chip control uses air blast and open flutes, not flood coolant that hides fuzz.
Indexing and edge inspection
Inspection measures tooth pitch, hub runout, dowel relationship and pocket depth; visual checks look for white stress marks at tooth roots. A test pin indexes across several teeth to prove burr removal did not change functional timing.
Star wheel tooling FAQ
Why use uncoated polished carbide on Delrin AF teeth?
The sharp polished edge shears PTFE-filled acetal instead of smearing it.
Can the hub bore be reamed?
Only if chips are fully cleared; fine boring gives better control in a soft polymer hub.
What inspection catches tooth burr problems?
A test pin indexing through several teeth plus magnified root inspection.
中文: Delrin AF分度星轮棘齿与弹簧定位槽配刀
这个Delrin AF星轮案例聚焦PTFE填充缩醛的图纸配刀:棘齿、定位槽和中心轮毂孔必须同时保证。搜索意图不是泛泛塑料加工,而是如何在不发白、不起毛、不丢齿距的情况下保留清晰分度边。
星轮图纸特征到塑料配刀
| 图纸特征 | 选定抛光刀具 | 选择理由 |
|---|---|---|
| 棘齿 | 3 mm单刃抛光无涂层硬质合金刀,吹气排屑 | 金属用涂层刀刃口钝,会抹压PTFE填充缩醛。 |
| 弹簧定位槽 | 2 mm PCD球刀,小步距扫描 | 钻尖形槽会形成卡住弹簧头的缺口。 |
| 中心轮毂孔 | 螺旋粗加工后用8 mm抛光硬质合金镗杆 | 铰刀在软聚合物内积屑会形成喇叭口。 |
| 销孔 | 硬质合金尖钻配轻量倒角路径 | 普通麻花钻出口易起毛。 |
| 外缘分度释放 | 4 mm O刃精刀 | 去除连接点时保护齿距。 |
防止齿形让刀的工艺顺序
毛坯仍为圆形且支撑好时先加工中心孔和销孔关系,齿形保留余量到孔稳定后再处理,然后用轻切顺铣完成棘齿。弹簧定位槽在外缘最终释放前精修,使弹簧落在干净圆角上,而不是钻尖缺口里。
Delrin AF切屑、毛刺和热量控制
Delrin AF能承受较高速度,但怕钝刀造成局部热量。选择抛光硬质合金和PCD是为了剪切;若金属用涂层刀的刃口处理会推料,就要淘汰。排屑靠吹气和大容屑槽,不靠会遮住毛边的冷却液。
分度与边缘检测
检测齿距、中心孔跳动、销孔关系和定位槽深度;外观检查齿根是否有白化应力痕。用测试销连续跨齿分度,确认去毛刺没有改变功能节拍。
星轮配刀问答
Delrin AF棘齿为什么用无涂层抛光硬质合金?
锋利抛光刃口能剪切PTFE填充缩醛,而不是把材料抹压过去。
中心轮毂孔可以铰吗?
只有完全排屑时才可考虑;精镗对软聚合物孔更可控。
什么检测能发现齿形毛刺问题?
用测试销连续分度多齿,并放大检查齿根。
Español: Herramientas para estrella Delrin AF con dientes
La estrella Delrin AF trata dientes, bolsillos de retén y agujero central sin blanqueo ni pelusa.
Estrella indexadora a herramientas
| Elemento | Herramienta pulida | Motivo |
|---|---|---|
| Dientes | Carburo pulido 3 mm un labio | El recubrimiento smearing el acetal. |
| Bolsillos retén | PCD bola 2 mm | La punta de broca hace muesca. |
| Agujero central | Mandrinado pulido 8 mm | El escariador abre boca. |
| Pasadores | Broca brad-point carburo | Menos pelusa de salida. |
| Alivio exterior | O-flute 4 mm | Protege paso. |
Orden contra deflexión de dientes
Primero se hacen hub y pasadores, luego los dientes con pasadas ligeras y las cavidades de resorte antes de soltar el exterior.
Viruta, rebaba y calor en Delrin AF
El material necesita filo pulido, aire y flautas abiertas; el recubrimiento metálico que empuja plástico se descarta.
Inspección de indexado
Se miden paso, concentricidad, relación de pasadores y profundidad de bolsillo; un pin prueba el indexado.
FAQ
¿Por qué carburo pulido?
Corta el acetal sin untarlo.
¿Escariado del hub?
Solo con viruta limpia; mandrinado controla mejor.
¿Qué prueba la rebaba?
Pin de indexado y lupa.
Français: Outils pour roue étoile Delrin AF à dents
La roue Delrin AF impose des dents nettes, poches de détente et alésage sans blanchiment.
Roue étoile vers outils polymère
| Élément | Outil poli | Raison |
|---|---|---|
| Dents | Carbure poli 3 mm une dent | Un outil revêtu écrase l’acétal. |
| Poches détente | Boule PCD 2 mm | La pointe crée une encoche. |
| Alésage central | Barre polie 8 mm | L’alésoir évase. |
| Pions | Foret carbure brad-point | Moins de barbe. |
| Dégagement | O-flute 4 mm | Tient le pas. |
Ordre contre flexion des dents
Hub et pions d’abord, dents en passes légères, puis poches ressort avant libération extérieure.
Copeau, bavure et chaleur Delrin AF
Arête polie, air et grandes goujures; les outils métal revêtus qui poussent la matière sont écartés.
Contrôle indexage
Pas des dents, concentricité, pions et profondeur sont mesurés; une pige teste l’indexage.
FAQ
Pourquoi carbure poli ?
Il cisaille l’acétal sans l’écraser.
Aléser au alésoir ?
Seulement copeau dégagé; l’alésage fin contrôle mieux.
Contrôle bavure ?
Pige d’indexage et loupe.
Русский: Инструмент для звезды Delrin AF
Звезда Delrin AF требует острых зубьев, карманов фиксатора и ступицы без побеления и ворса.
Звезда и инструмент для пластика
| Элемент | Полированный инструмент | Причина |
|---|---|---|
| Храповые зубья | Полированный карбид 3 мм один зуб | Покрытый инструмент мажет ацеталь. |
| Карманы фиксатора | PCD шар 2 мм | Сверло дает надрез. |
| Ступица | Полированная расточка 8 мм | Развертка может раструбить. |
| Штифты | Карбид brad-point | Меньше ворса. |
| Наружное снятие | O-flute 4 мм | Держит шаг. |
Порядок против прогиба зубьев
Сначала ступица и штифты, затем зубья малыми проходами и карманы пружины до снятия наружной опоры.
Стружка, заусенец и тепло Delrin AF
Нужны полированная кромка, воздух и открытые канавки; покрытые металлические фрезы отклонены.
Контроль индексации
Измеряют шаг, биение, штифты и глубину; контрольный штифт проверяет индексацию.
Вопросы
Почему полированный карбид?
Он срезает ацеталь без размазывания.
Можно разверткой?
Только при чистой стружке; расточка лучше.
Как проверить заусенец?
Индексный штифт и увеличение.