English: Part Requirements and Material Behavior
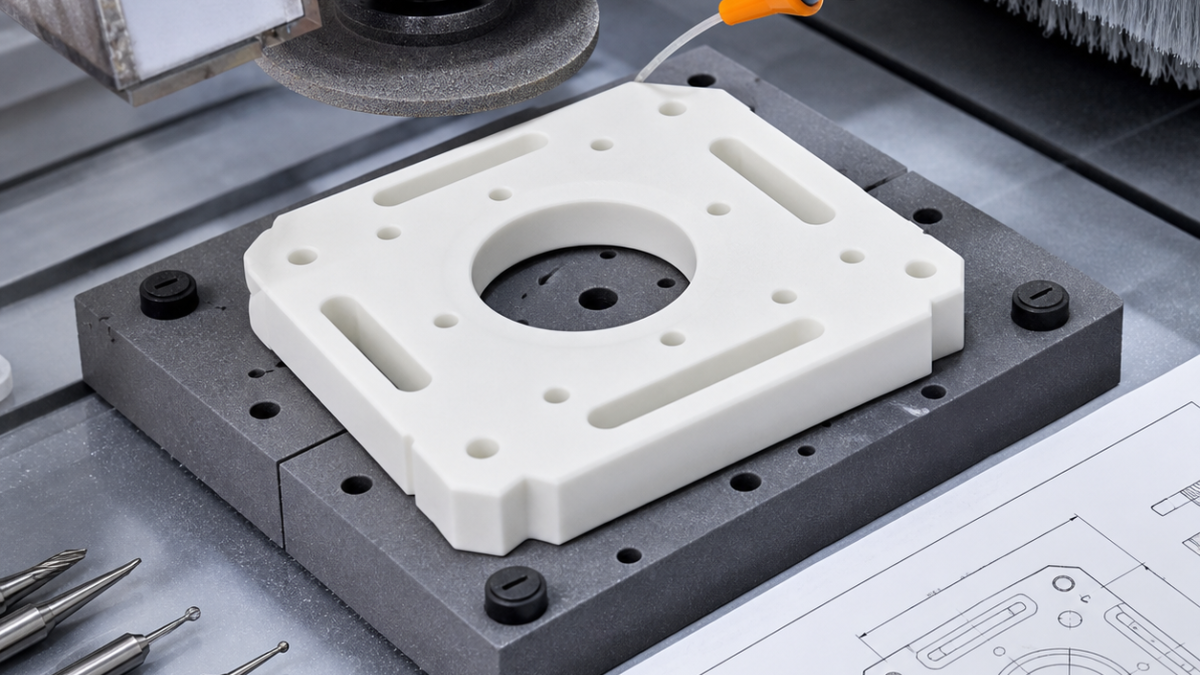
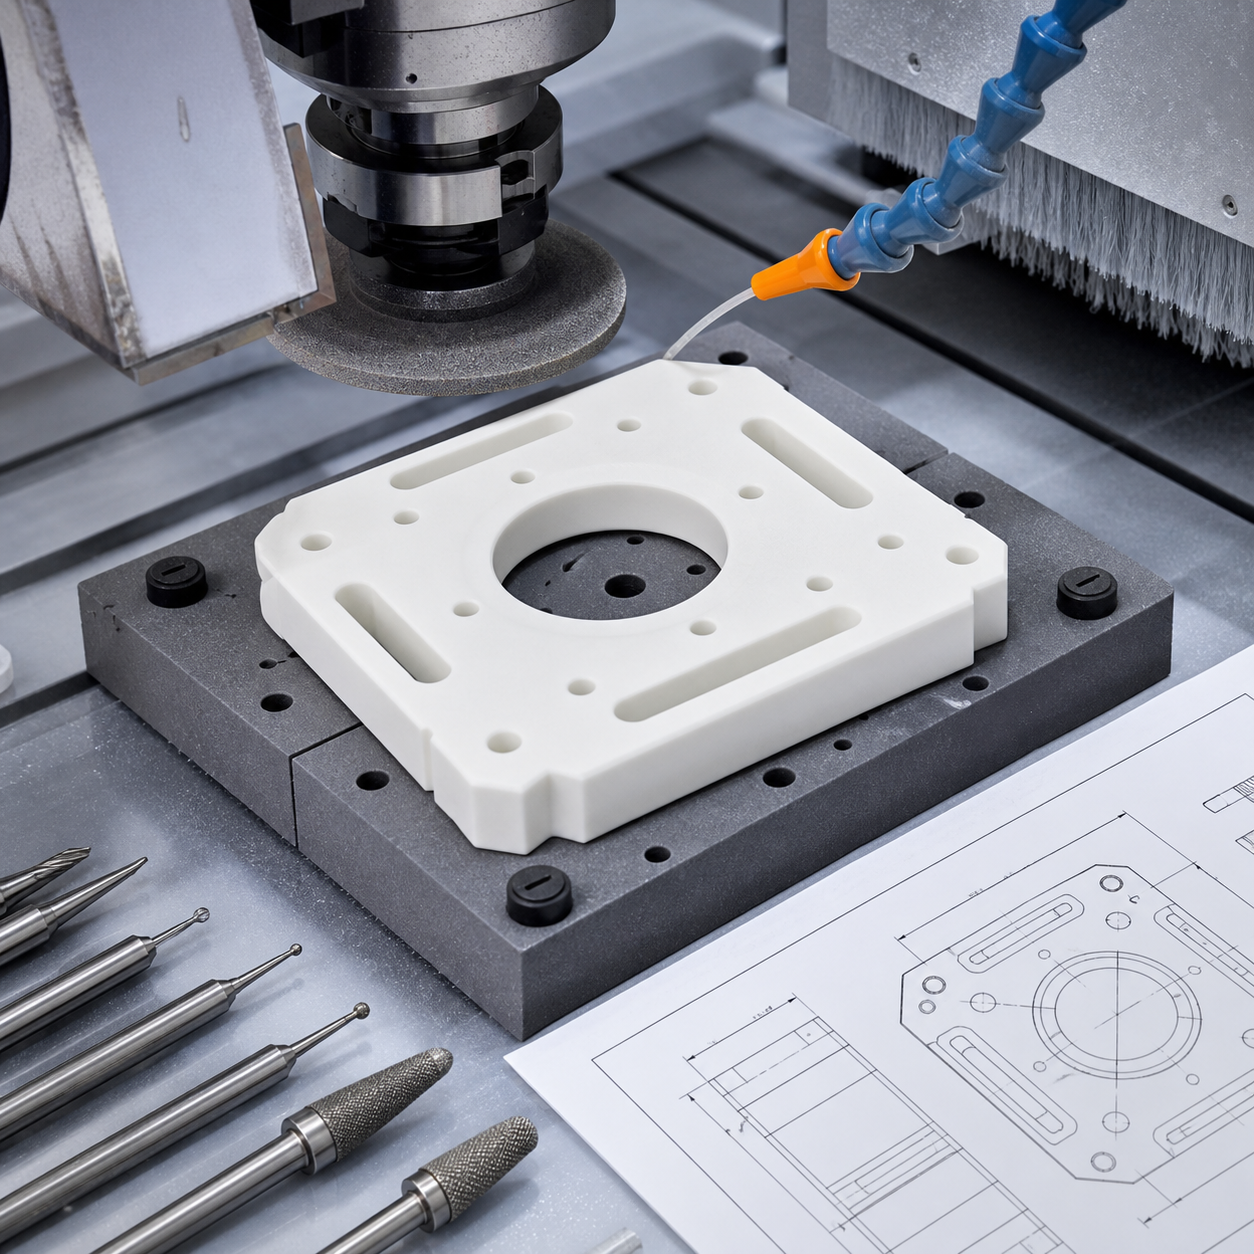
This case study covers a zirconia ceramic insulating base with a central clearance bore, four long slots, small mounting holes and chamfered edges. The example drawing calls for 0.02 mm flatness on the mounting face, controlled slot width, clean hole exits and no visible edge chipping on functional surfaces. Zirconia is hard and wear-resistant, but it does not behave like metal under a cutting edge.
The main process risk is brittle fracture. Excess force, poor support, tool runout or aggressive exit conditions can create microcracks that are not obvious during machining. For this reason, the plan emphasizes diamond tooling, gentle engagement, constant support and inspection that looks beyond simple dimensions.
Holding and Support
A flat vacuum fixture with a soft sacrificial interface is suitable when the underside is already ground. The fixture should support the part close to slots and holes, not only around the perimeter. If vacuum is not reliable because of through features, use a mechanical frame clamp with compliant pads and a controlled torque procedure.
Never clamp directly on a sharp ceramic corner. Local stress concentration can start cracks before the spindle turns. Keep the part clean, remove abrasive slurry frequently and verify that no hard chips are trapped between the ceramic and the support face.
Diamond Tooling Plan
| Operation | Suggested tool | Process reason |
|---|---|---|
| Face finishing | Fine diamond grinding wheel or cup wheel | Controls flatness with low thermal load |
| Slot roughing | Diamond electroplated or resin-bonded grinding pin | Avoids metal-style chip formation and reduces cracking |
| Small holes | Diamond core drill or ultrasonic-assisted diamond drill where available | Improves exit quality and reduces thrust |
| Edge chamfer | Small diamond chamfer wheel or diamond burr | Removes fragile sharp edges consistently |
| Final touch | Fine-grit diamond lap or polishing tool | Improves sealing or insulation contact surfaces |
Starting Parameters and Coolant
Parameter selection should begin with the diamond tool supplier’s data, because bond type and grit size change the process strongly. As a commissioning reference, use shallow infeed, high spindle speed, low axial force and steady coolant flow. For small diamond tools, reduce depth before reducing feed so the tool continues to cut or grind cleanly instead of rubbing and heating the ceramic.
Coolant must remove heat and abrasive debris. A clogged contact zone raises temperature, loads the diamond tool and increases edge chipping. Filter the coolant and clean the fixture between parts so abrasive particles do not damage reference surfaces.
Operation Sequence and Inspection
- Inspect incoming ceramic blanks for chips, warpage and surface defects.
- Grind or verify the primary mounting face before precision features.
- Support the part on a soft vacuum or compliant mechanical fixture.
- Machine holes with exit support or a sacrificial backing plate.
- Grind slots using multiple shallow passes and controlled entry/exit paths.
- Add chamfers before final cleaning to remove fragile edges.
- Clean ultrasonically or with an approved process to remove abrasive residue.
- Inspect flatness, slot width, hole diameter, edge condition and visible cracks under magnification.
The SEO focus is zirconia ceramic CNC grinding with diamond tooling, edge chipping control and inspection. These phrases belong naturally in the technical explanation because they describe the real manufacturing problem.