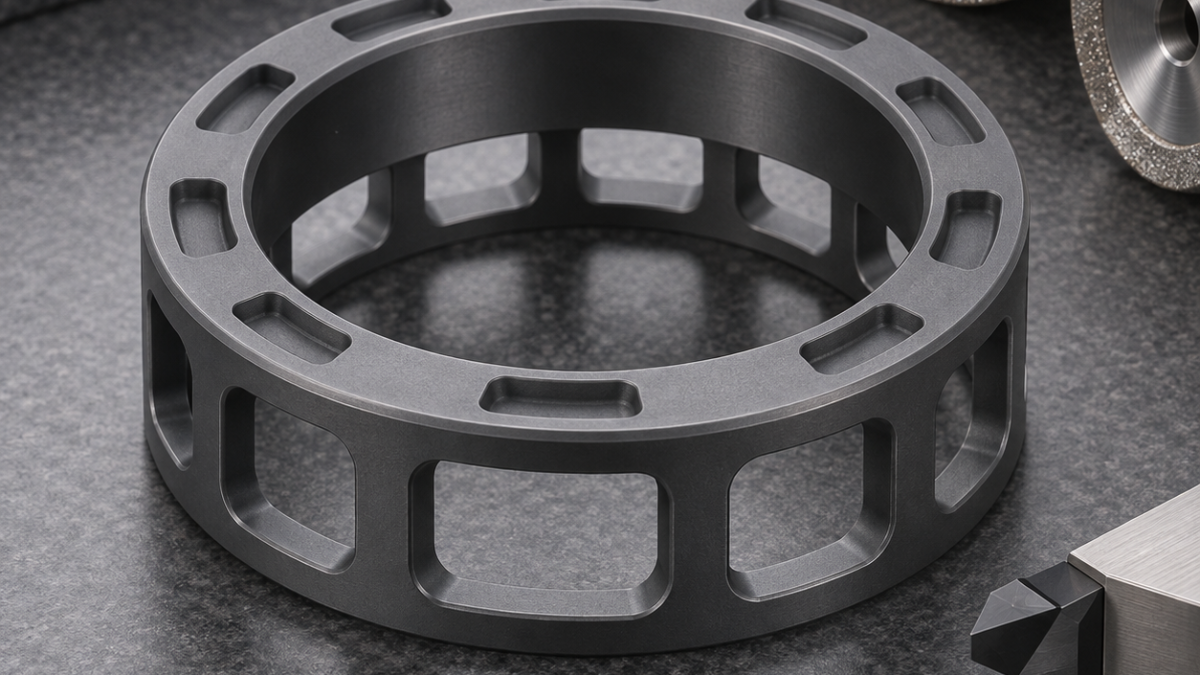
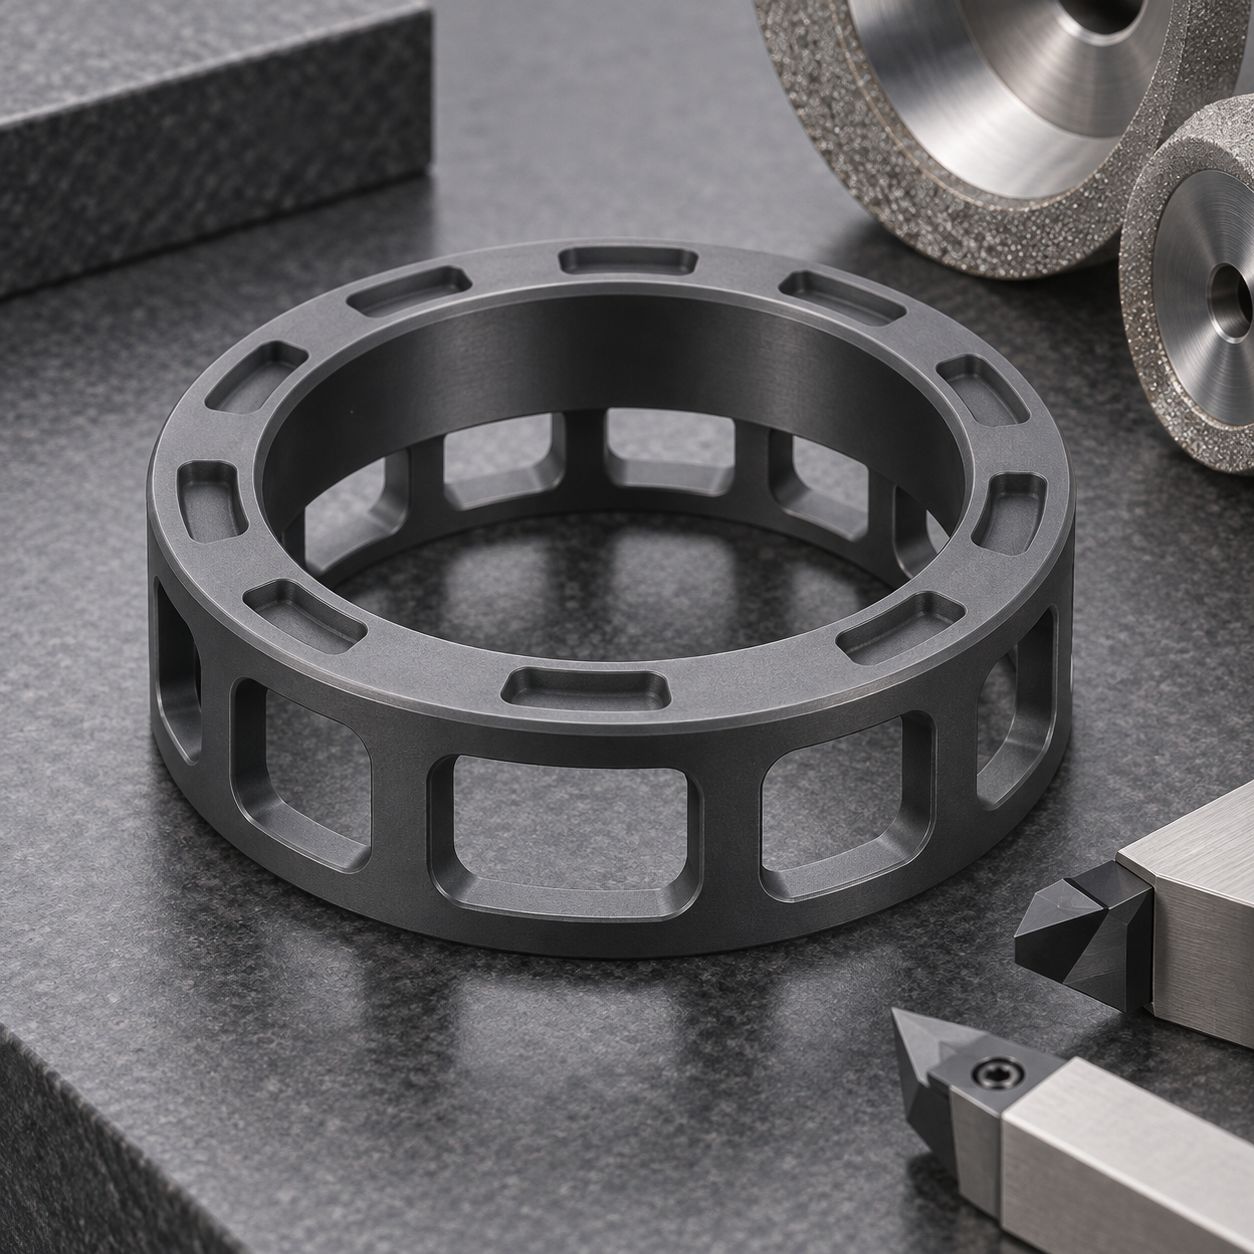
English: Silicon Nitride Bearing Cage Diamond Tooling for Thin Windows and Chip-Free Edges
This case starts from fracture risk rather than cycle time. The drawing allows only tiny edge chips around thin cage windows, while bore roundness and rail parallelism must survive the release of each web. Every tool is therefore judged by force direction, grit exposure and how the exit edge is supported.
Draw a fracture map around every window corner
Bond the sintered blank to a precision sacrificial mandrel with a removable low-shrink adhesive. Diamond-grind the bore using a vitrified 800-grit wheel and finish the two rails by opposed cup wheels while the ring is continuous. A probing pass records runout before any window interrupts the hoop.
Diamond-tool map for the ceramic cage
| Drawing feature | Carbide tool and holder | Selection logic / rejected alternative |
|---|---|---|
| Precision bore | Vitrified-bond diamond wheel, 800 grit, balanced internal spindle | Produces roundness with low subsurface damage; single-point PCD leaves directional stress. |
| Rail faces | Opposed 400/800-grit resin-bond diamond cup wheels | Balances axial force; one-sided grinding dishes the ring. |
| Window end radii | 6 mm metal-bond diamond core tool, through-spindle coolant | Keeps radius compressive; plunging a router concentrates corner load. |
| Window connecting walls | 3 mm electroplated diamond router, short reach, climb cut | Open grit clears ceramic swarf; a fine wheel loads before rough stock is removed. |
| Oil pockets and edge blend | 2 mm resin-bond diamond wheel plus 1000-grit chamfer pin | Low-force finish; hand stones create uneven edge-chip depth. |
Establish the bore before weakening the ring
Rough each window by trepanning two end radii with a 6 mm metal-bond diamond core tool, then connect them using a 3 mm electroplated diamond router in climb direction. Leave a 0.15 mm membrane at the exit and remove it from the supported side with a fresh fine-grit tool. Direct full breakthrough would put tensile stress on an unsupported corner.
Open windows with supported exits
Finish shallow oil pockets with a 2 mm resin-bond diamond wheel at low radial engagement and continuous clean coolant. Inspect edges under controlled oblique light, but confirm suspicious indications with fluorescent penetrant or microscopy; a dark shadow is not automatically a crack. Bore roundness is measured after adhesive release and thermal soak, because the fixture can hide springback.
Related tooling comparisons: ceramic micro-orifice protection; post-sinter ceramic datum control.
Silicon-nitride cage FAQ
Why not use carbide? It rubs rapidly on silicon nitride and drives cracks. Can all windows be cut sequentially? Alternate opposite windows to balance hoop stiffness. When is a diamond tool dressed? When spindle power rises or grit loading changes before visible edge damage.


