Related tooling references: PPSU Sterilization Tray Latch Rail CNC Tool Selection for Snap Hooks and Drain Slots and H13 Hot Runner Nozzle Tip CNC Tool Selection for Conical Gate Seat and Spiral Heater Groove.
English: AZ31B Camera Housing Tooling for Cooling Fins and Lens Boss
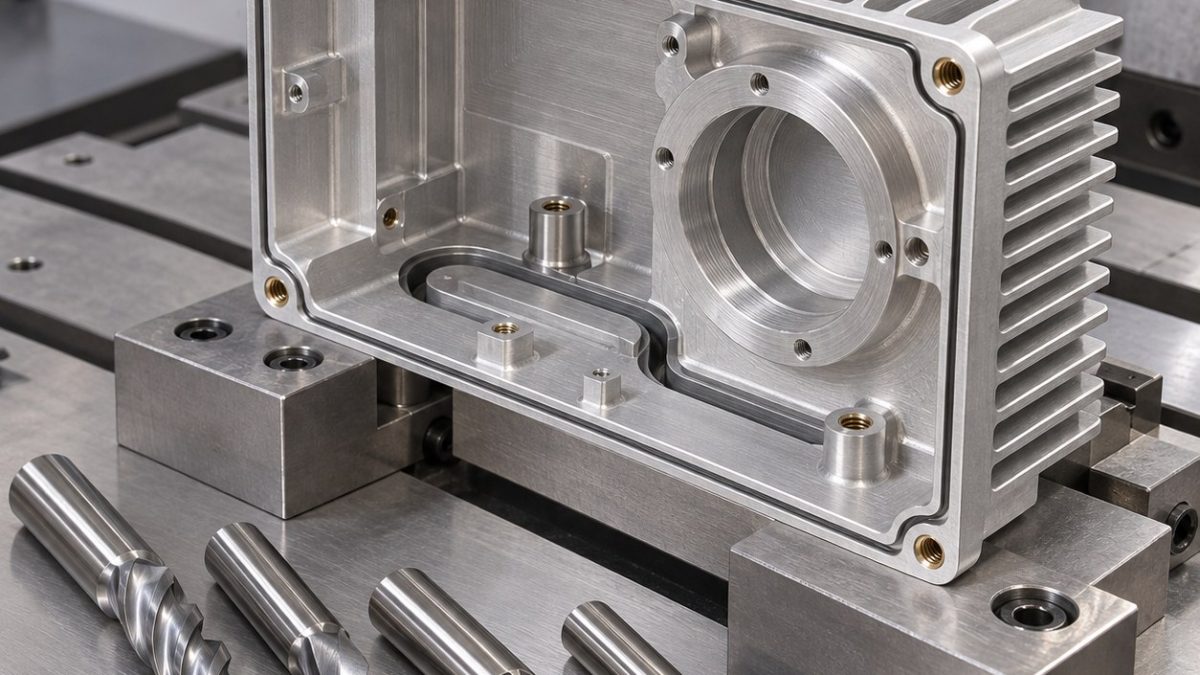
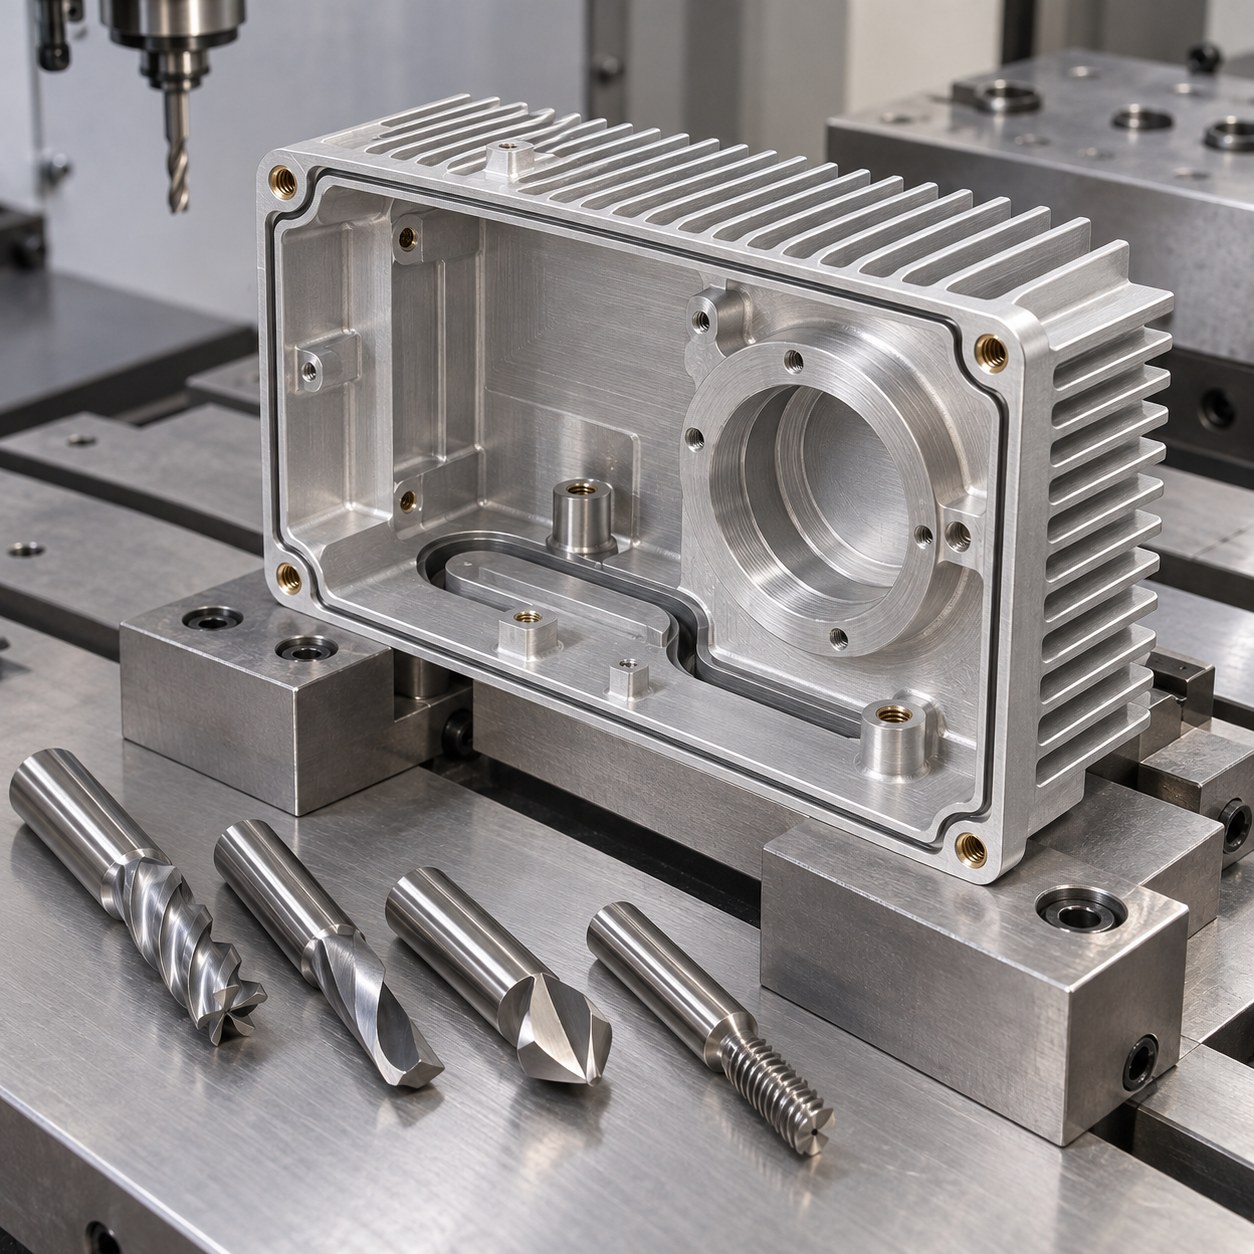
This AZ31B camera housing case answers how to tool thin magnesium fins, a lens boss pocket and internal cable trench without creating heat or unsafe chip packing. The selected tools favor sharp dry cutting and predictable evacuation.
Magnesium housing features and tool choice
| Feature | Tool and holder | Safety and quality reason |
|---|---|---|
| Thin cooling fins | 4 mm sharp uncoated carbide high-helix end mill | Sharp uncoated edge lowers heat; coated roughers can rub magnesium. |
| Lens boss pocket | 8 mm 3-flute carbide rougher, 6 mm ball/radius finisher | Keeps optical boss round while removing stock efficiently. |
| Cable trench | 3 mm single-flute carbide slot tool | Large flute clears dry chips before packing. |
| Gasket groove | 1.5 mm polished carbide grooving cutter | Keeps groove floor clean without tearing the soft alloy. |
| Threaded insert holes | Carbide drill and thread mill, dry air evacuation | Thread milling avoids chip jam and allows insert fit adjustment. |
Thin-fin process order
Machine the lens boss and internal pads first while the housing is rigid, then cut the cable trench and gasket groove. Cooling fins are roughed with support stock and finished in alternating passes before the outside wall is released.
AZ31B chip and heat control
Magnesium demands dry chip discipline. Use sharp uncoated carbide, air evacuation, chip collection and no dwell at fin roots. Built-up edge or dark chips stop the tool before surface finish fails.
Housing inspection plan
Inspect boss coaxiality, fin height, gasket groove depth, insert thread fit, burrs in the cable trench and final housing flatness after unclamping.
Magnesium tooling FAQ
Why use uncoated carbide on AZ31B?
A sharp uncoated edge cuts cooler and avoids rubbing in magnesium.
What is the safety trigger to stop?
Packed chips, dark chips or built-up edge near fin roots.
Why finish fins before releasing the wall?
Support stock keeps thin fins and the housing wall from bowing.


