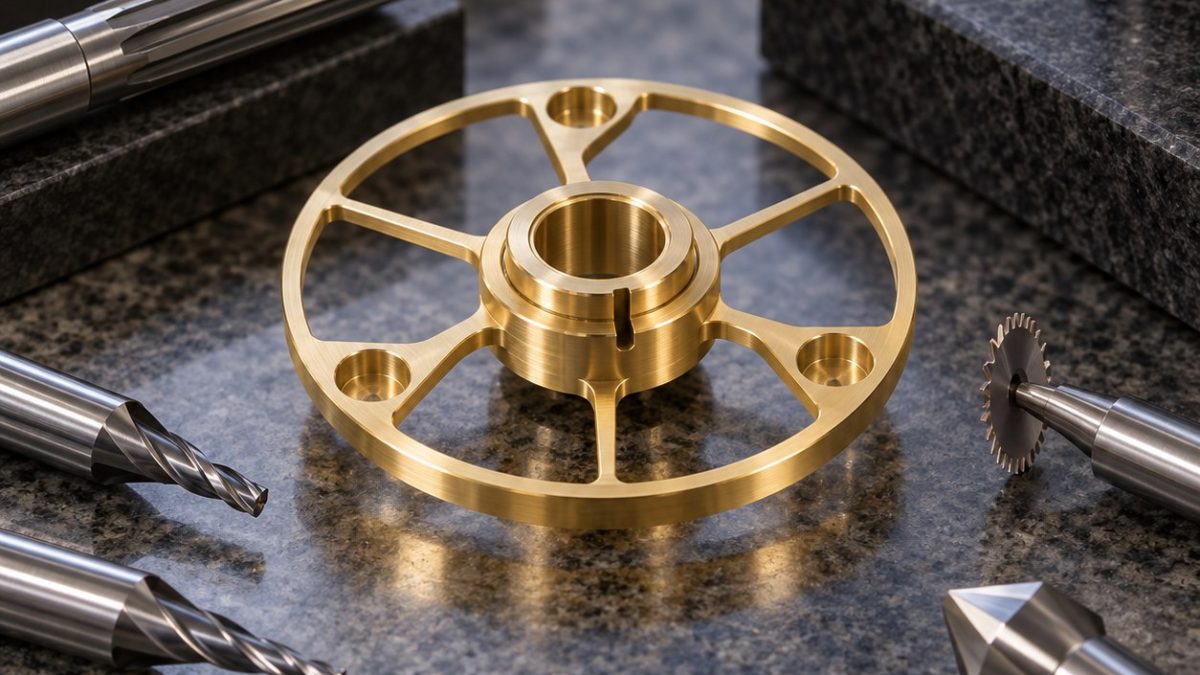
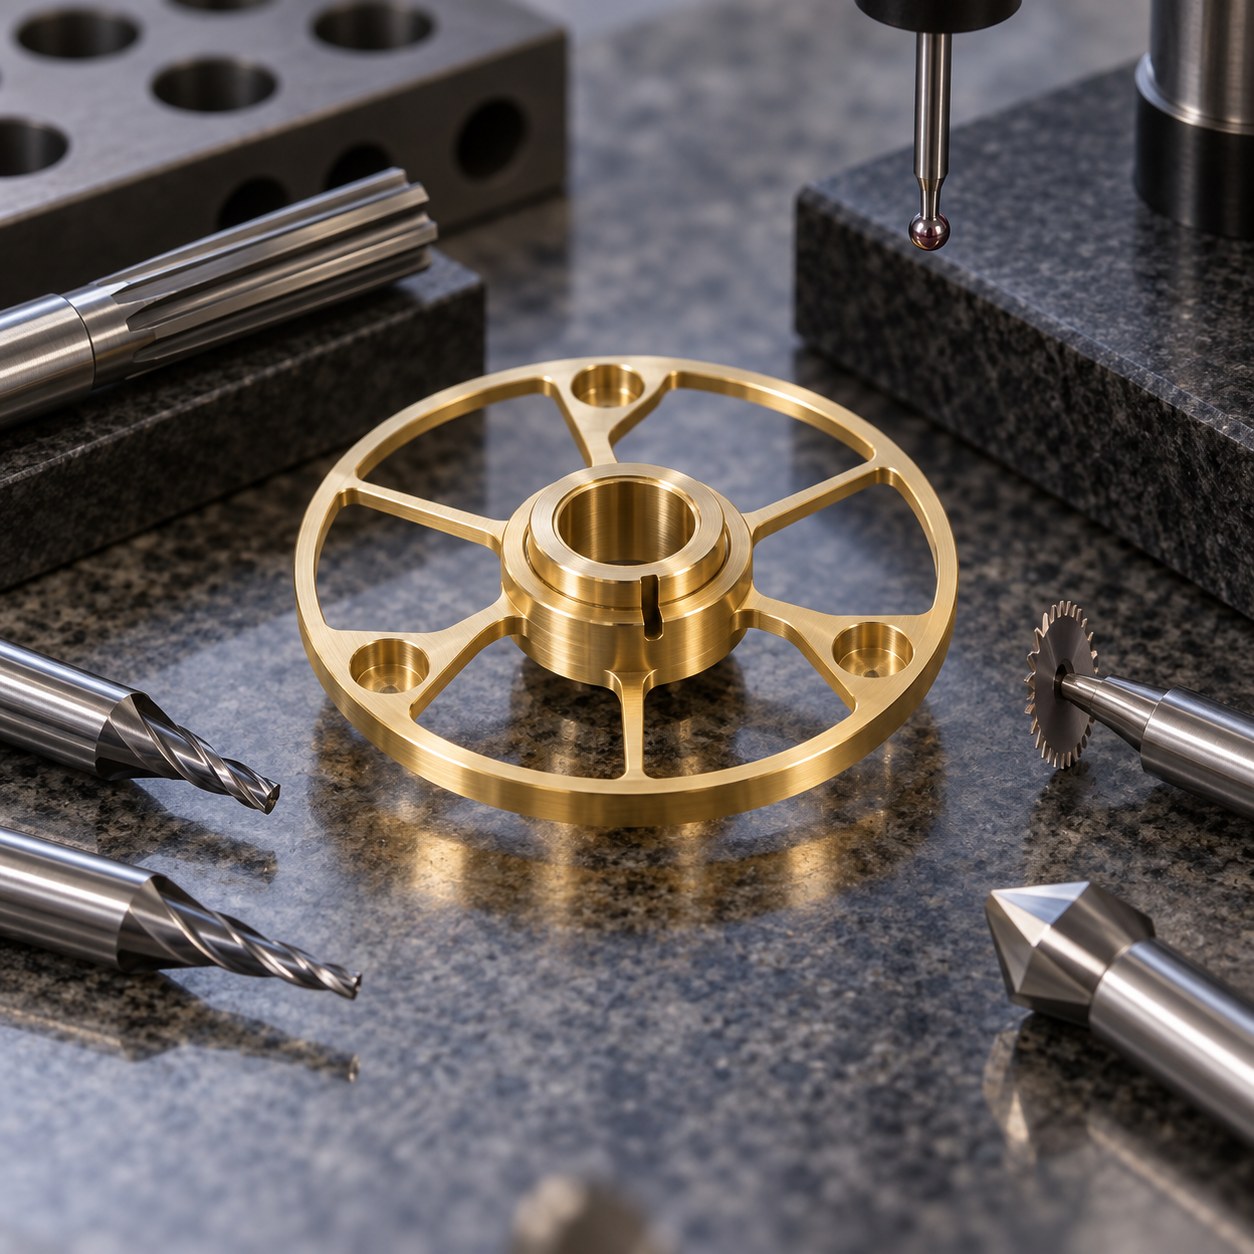
English: C26000 Shutter Hub Tooling for Thin Spokes and Timing Slot
The key is to preserve shaft-bore concentricity and equal spoke stiffness while opening six large windows. The hypothetical drawing dimensions spoke thickness from the reamed bore and clocks the timing slot from one counterweight pocket; the outer rim remains connected until late.
Fix bore and angular reference first
| Drawing feature | Carbide tool and holder | Why selected / alternative rejected |
|---|---|---|
| Hub face and shaft bore | Carbide drill, fine boring pass and 6 mm carbide reamer in precision collet | Boring corrects location before sizing; drill-to-ream follows drift. |
| Six spoke windows | 4 mm 3-flute polished uncoated carbide end mill, 8 mm reach, hydraulic holder | Alternate windows balance force; full-depth consecutive slots pull the rim. |
| Timing flag slot | 0.8 mm 2-flute polished carbide slot mill, minimum overhang | Sharp edges limit burr; a slitting saw leaves an inaccessible inner lip. |
| Counterweight pockets | 2 mm 2-flute polished carbide end mill with circular interpolation | Pocket depth remains adjustable; drilling removes mass too abruptly. |
| Retaining-ring groove | 1 mm positive carbide groover with 0.02 mm hone, rigid short holder | Dedicated width holds floor; hand-cut groove varies concentricity. |
Open windows without pulling spokes
Finish the bore and angular datum while the blank is a solid disc. Rough opposite windows in pairs, leaving radial bridges at the rim; semifinish all spoke sides before cutting the timing slot and counterweight pockets. Remove bridges in a star sequence on a broad vacuum nest, then finish the retaining groove from the bore datum.
Choose sharp tools for brass burr control
C26000 cuts freely but long chips and a dull edge create exit burrs on thin spokes. Keep polished flutes clean and use air or approved mist for evacuation. Replace the micro slot cutter if the slot closes, shines or develops a feather. Never correct one spoke by hand without checking mass symmetry.
Inspect free-state runout and balance features
After release, measure bore-to-rim runout, spoke thickness at two radii and axial flatness. Inspect the timing-slot edges under magnification and record pocket volumes rather than only depths. Dynamic balance and shutter response require separate assembly tests.
Practical tooling FAQ
Why rough opposite windows together?
Symmetric material removal reduces rim movement and keeps spoke load comparable.
Why measure pocket volume?
Balance correction depends on removed mass; depth alone ignores actual pocket area and corner radii.
thin-disc window and datum-bore tooling · copper-alloy precision feature selection


