English: Nickel 200 Electrolyzer Clamp Tooling for Flexure Slots and Cooling Passage
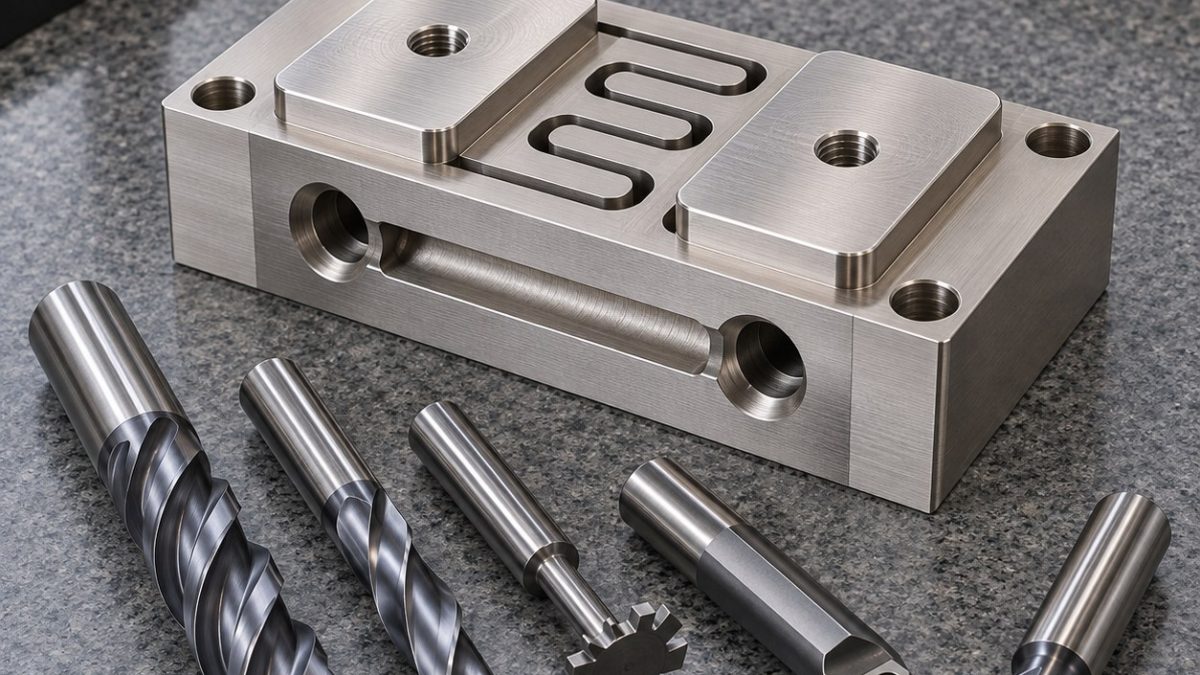
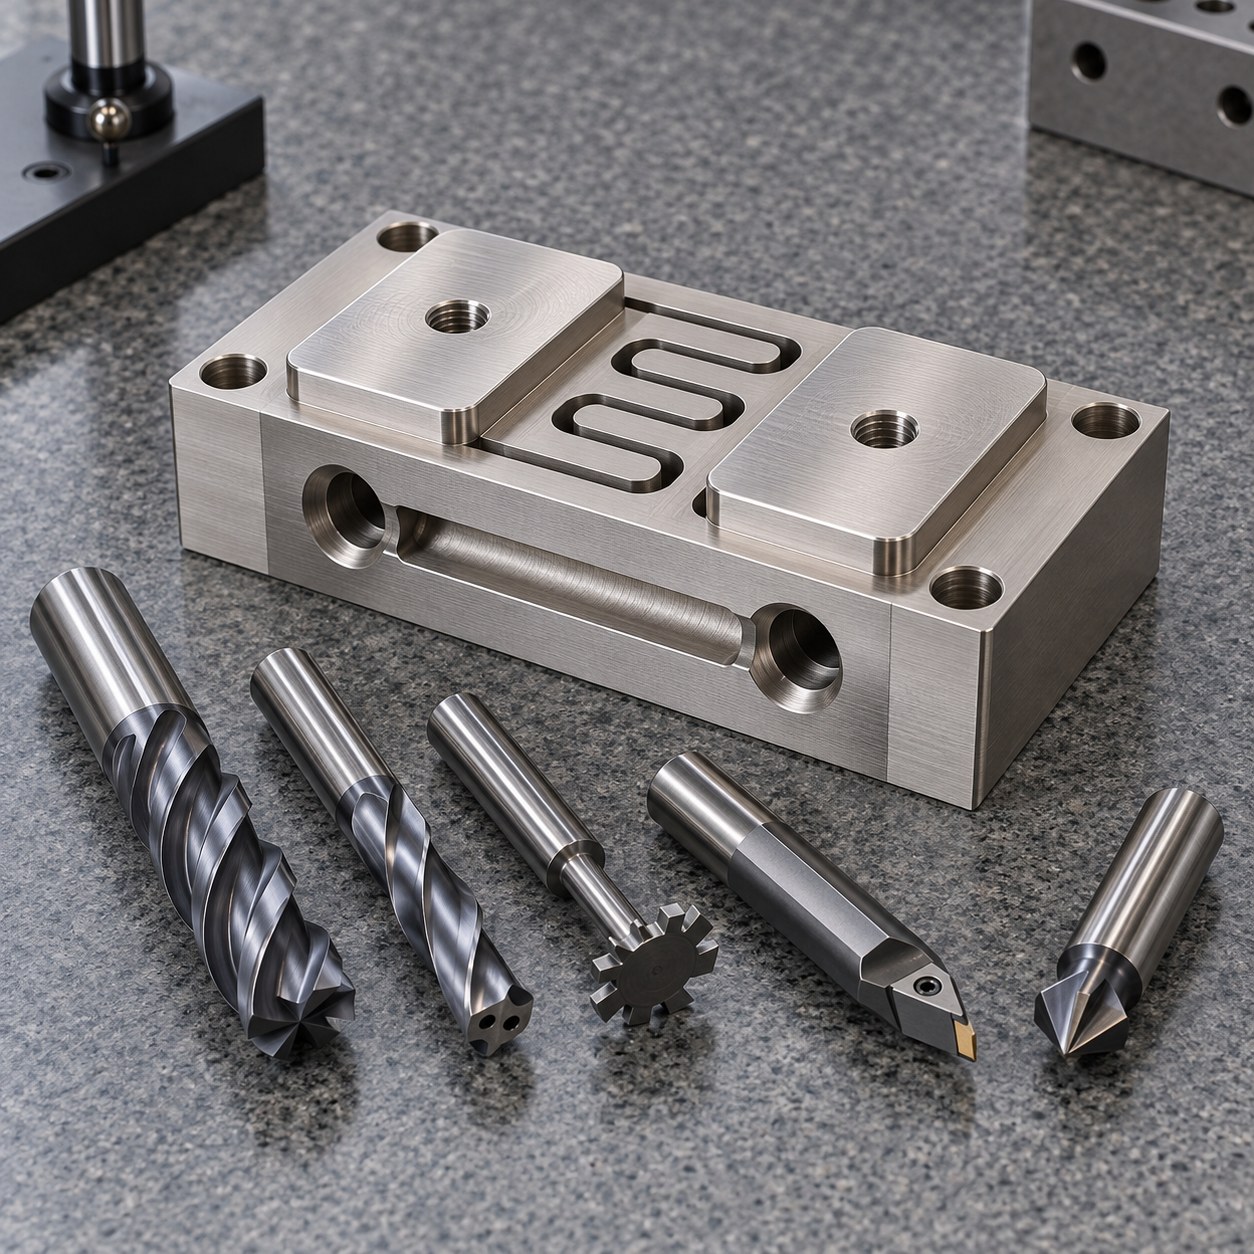
The search intent is how to machine a Nickel 200 current-collector clamp without smearing the electrical pads or closing its thin serpentine flexures. The hypothetical drawing makes the lower mounting face datum A, a reamed hole datum B and a side face datum C; pad coplanarity and cooling-passage position both originate from A-B-C.
Establish the electrical datum chain
Finish datum A and ream B before the clamp becomes compliant. Drill the cooling passage from both ends to a controlled overlap, semifinish the contact pads, then rough each flexure by alternating short axial levels while leaving temporary bridges. Finish pads in one low-force raster pass, finish the flexures from the center outward, remove bridges last and use a full-face vacuum nest for final inspection cuts.
Assign tools to the compliant features
| Drawing feature | Carbide tool and holder | Why selected / alternative rejected |
|---|---|---|
| Datum face and raised contact pads | 10 mm 3-flute polished uncoated carbide end mill, hydraulic holder, sharp 5 µm edge | Positive polished geometry limits built-up edge; a honed steel-grade cutter smears nickel. |
| Serpentine flexure slots | 1.5 mm 2-flute polished carbide slot mill, reduced neck, high-accuracy collet | Two flutes leave chip space and low radial force; a slitting saw cannot follow the closed serpentine path. |
| Cross cooling passage | 5 mm through-coolant carbide drill followed by short single-edge boring tool | Pilot drilling establishes direction and boring corrects size; a long HSS drill can bell the exits. |
| Mounting and location holes | Carbide drill plus PCD-tipped reamer in floating holder | Reaming preserves A-B-C location and finish; helical interpolation alone leaves lobing in ductile nickel. |
| Pad-edge break and port chamfer | 60-degree single-flute polished carbide chamfer mill, minimal projection | A single sharp edge cuts rather than rolls a burr; hand deburring changes pad height. |
Prevent nickel pickup and slot closure
Nickel 200 work-hardens when a cutter rubs and it readily forms a built-up edge. Maintain chip thickness, avoid dwell at pad corners and clear stringy chips before they cross a flexure. Retire the micro slotter when slot width trends narrow, the edge shows nickel pickup or exit burr height rises; do not compensate a worn cutter by forcing deeper radial engagement.
Inspect before and after bridge release
Inspect A-to-pad height and pad coplanarity before releasing the bridges, then map free-state flexure gap optically. Gauge the reamed holes, borescope the cooling-passage overlap and use a low-force CMM routine for passage position. Electrical resistance, coolant pressure and electrolyzer compatibility are separate qualification tests, not machining claims.
Practical tooling FAQ
Why finish the pads before removing every bridge?
The temporary stiffness keeps both electrical pads in the same cutting plane during the final raster pass.
Why drill the cooling passage from two ends?
The controlled overlap reduces drill length while boring and borescope inspection manage the meeting zone.
PCTFE cryogenic seal-cone tooling · CuCrZr cooling-channel tooling