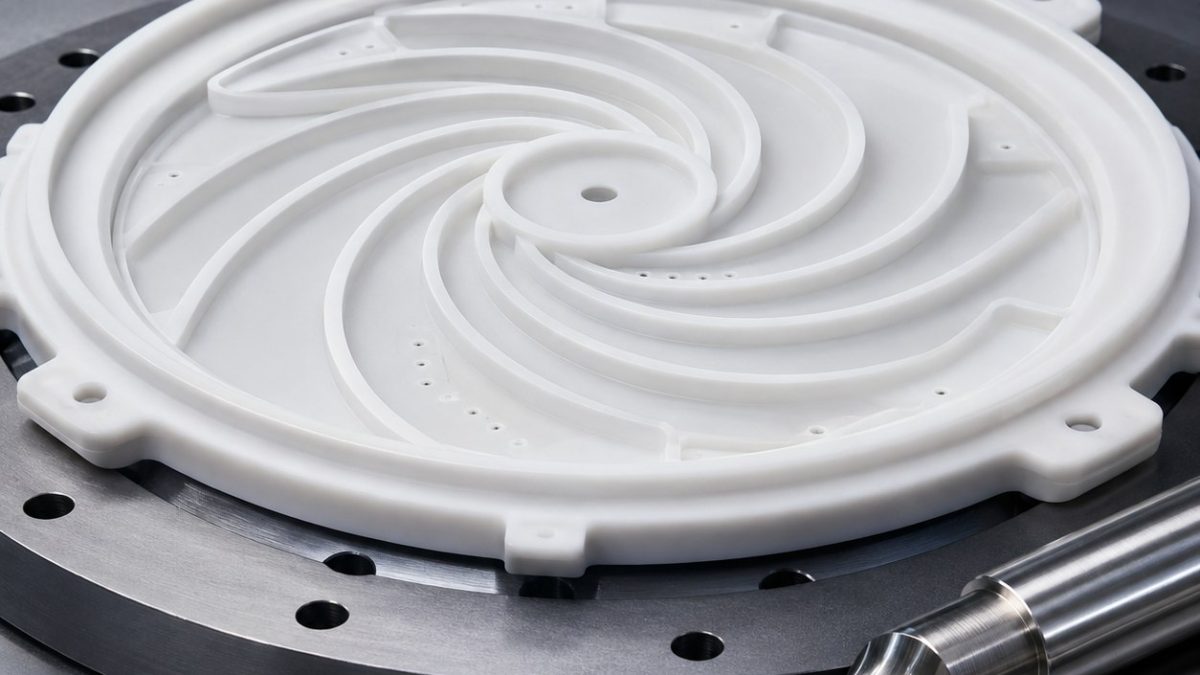
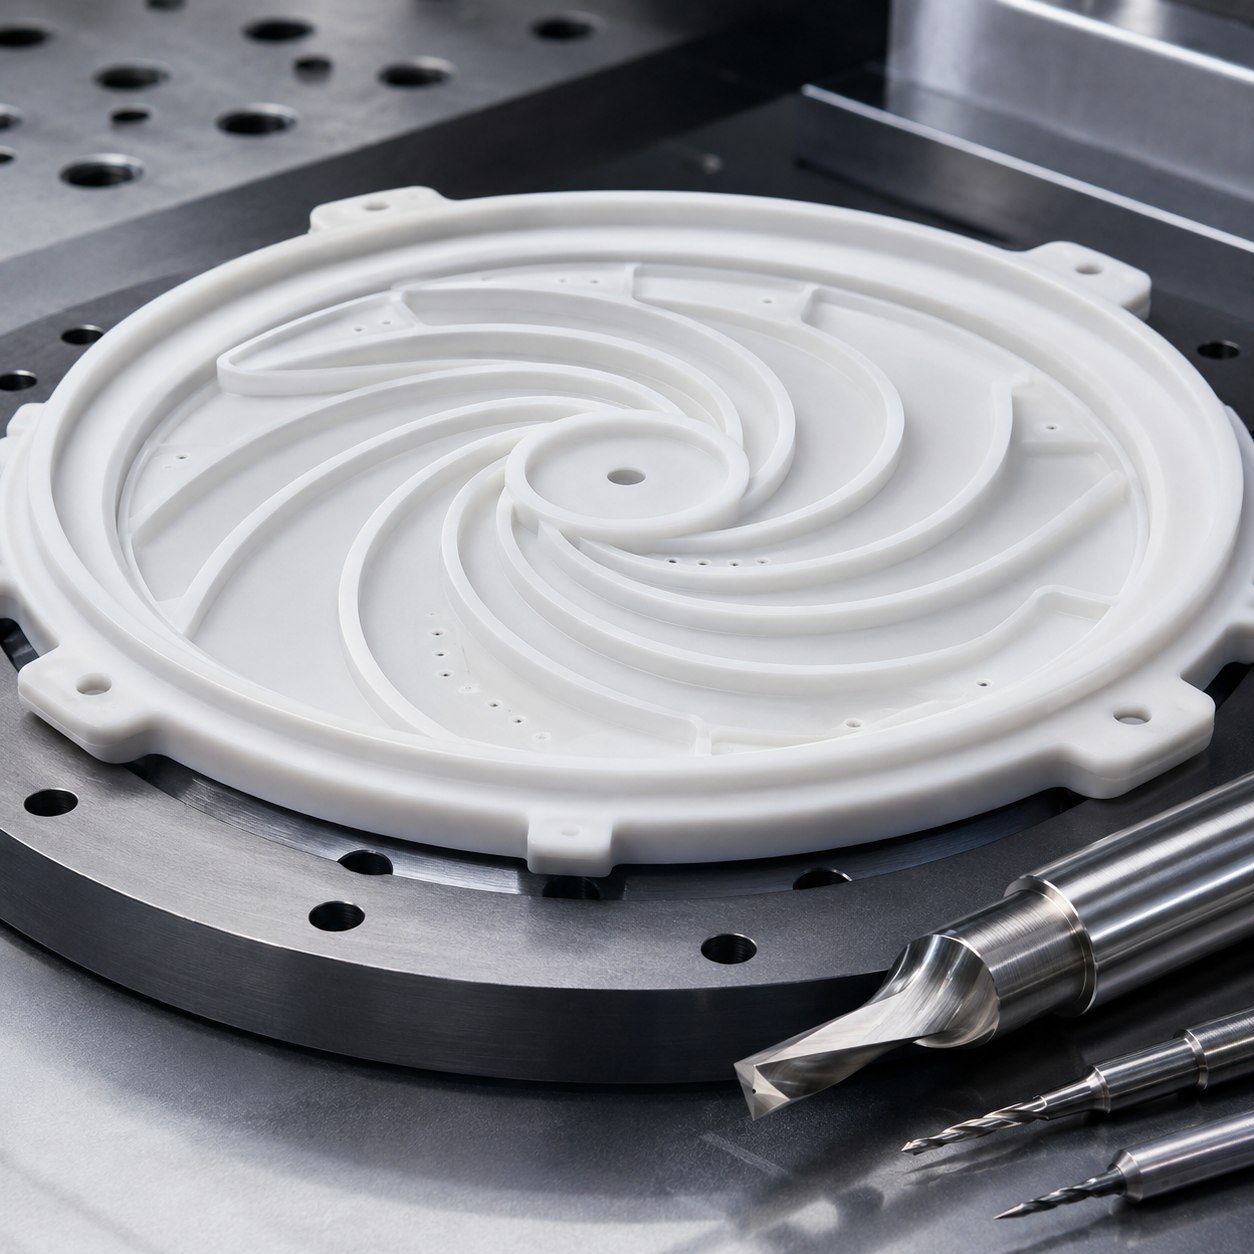
English: ETFE Diaphragm Support Tooling for Spiral Flexure and Sealing Bead
The functional risk is elastic release: the spiral flexure can move after unclamping, while heat or a dull edge can roll the ETFE sealing bead. Sharpness and fixture pressure are therefore drawing controls.
Drawing feature-to-tool decisions
| Drawing feature | Tool, geometry and holder | Decision and rejected alternative |
|---|---|---|
| Blank profile | Ø8 single-flute polished uncoated carbide, high rake, short reach | Creates a clean chip with low heat; coated multi-flute roughers are rejected for rubbing. |
| Spiral flexure slot | Ø2 two-flute polished carbide with necked reach in a high-accuracy collet | Keeps chip space and access while limiting wall push. |
| Raised sealing bead | Ø3 ball-nose polished carbide, measured runout below bead tolerance | Blends bead flanks without hand sanding the functional crest. |
| Shallow flow recesses | Ø4 single-flute end mill with ramp entry | Avoids plunge marks and evacuates stringy ETFE chips. |
| Purge holes and edge break | Carbide micro drill with sacrificial backing plus 90° single-flute chamfer tool | Prevents exit rollover and blocked flow paths. |
Fixture and cutting sequence
Vacuum support acts on the solid rim only. Rough both sides of the spiral symmetrically, leave 0.10 mm on the slot walls, thermally stabilize, then finish the sealing bead and drill purge holes over a sacrificial PEEK backing plate.
Material, chip and tool-life controls
Use air plus controlled mist, never aggressive flood pressure on the flexure. Vacuum chips between passes, limit spindle heat soak, and replace the slot tool at the first edge-radius growth rather than compensating a rolled wall.
Tolerance and surface verification
Inspect spiral width at supported and free state, bead height with a non-contact profiler, hole openness by flow test and outer flatness after 20 minutes released. Functional surfaces target Ra 0.8 µm with no white rolled burr.
Search questions answered
Why choose uncoated polished carbide for ETFE?
Edge sharpness and low friction matter more than a heat-resistant coating, whose edge radius can rub the polymer.
When is the bead finished?
After slotting heat has dissipated and while the solid rim remains supported.
How is rollover detected?
Use oblique optical inspection plus a low-pressure flow test through every purge hole.


