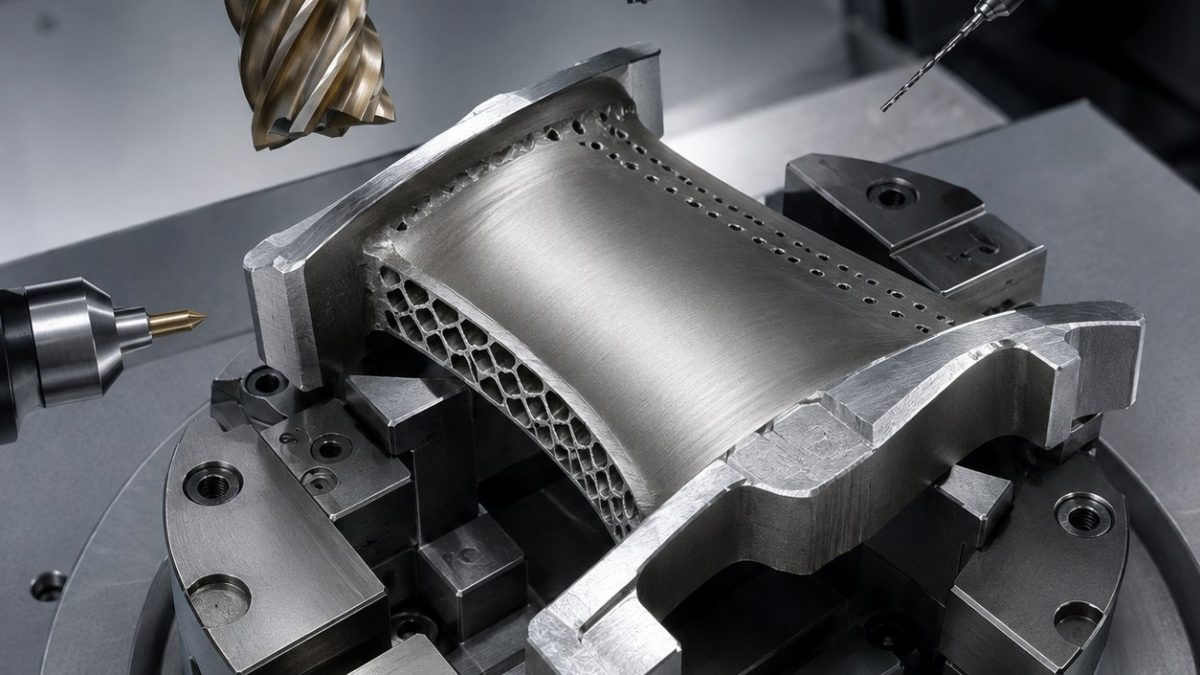
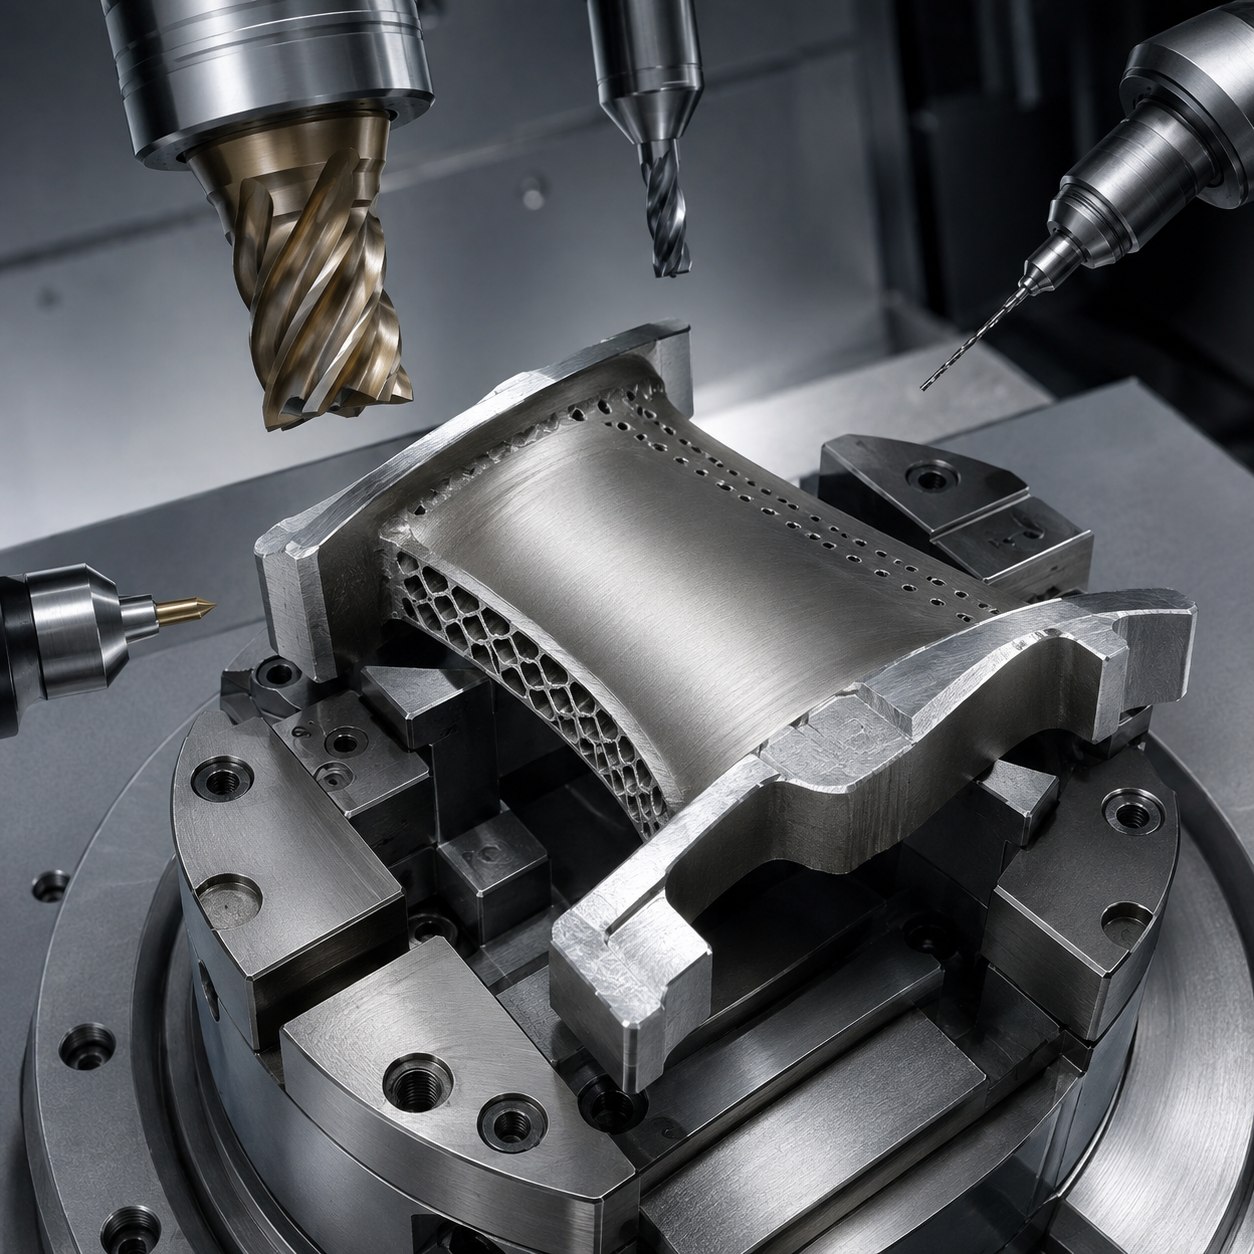
English: Rene 41 Seal Segment Tooling for Honeycomb Pocket and Feather Edges
This case begins at the thin feather edge, because a toolpath that is safe in the pocket can still pull the edge or consume braze stock. Five-axis access and wear trends drive each cutter decision.
Drawing feature-to-tool decisions
| Drawing feature | Tool, geometry and holder | Decision and rejected alternative |
|---|---|---|
| Forging skin and datum pads | Ø32 high-positive PVD carbide shoulder mill, strong micro-hone | Survives interrupted skin while avoiding a heavily negative heat-generating edge. |
| Honeycomb braze pocket | Ø10 5-flute AlTiN variable-helix rougher, then Ø6 reduced-neck finisher | Separates metal removal from corner access and protects braze-wall stock. |
| Curved gas-path surface | Ø12 carbide barrel cutter, AlTiN, shrink-fit holder | Large effective radius reduces passes; a long small ball mill is rejected for deflection. |
| Feather edges | Ø4 sharp corner-radius carbide, light alternating passes | Balances cutting force across the thin edge and leaves controlled braze allowance. |
| Angled cooling holes | Carbide spot drill plus Ø1.2 coated micro drill, short pilot and guided 5-axis entry | Prevents skating and work-hardened entry; peck dwell is rejected. |
Fixture and cutting sequence
Use a 3+2 roughing orientation for the pocket, leave 0.30 mm braze stock, then use continuous five-axis barrel finishing on the gas path. Support the feather edge with a removable nest and alternate sides before microdrilling.
Material, chip and tool-life controls
Rene 41 work-hardens after rubbing. Keep radial engagement constant, use high-pressure coolant aimed below the edge, index tool life by cutting minutes and stop when scallop height or spindle load trends upward.
Tolerance and surface verification
Blue-light scan compares the gas-path profile, CMM verifies datum-pad relation and feather-edge stock, and borescope inspection checks cooling-hole breakout. Braze-pocket walls retain 0.30 ±0.03 mm and the finished surface targets Ra 1.6 µm before coating.
Search questions answered
Why use a barrel cutter on the gas path?
Its large effective radius reduces passes and deflection while preserving five-axis contact control.
When is a micro drill changed?
Change it on thrust or breakout trend, not only after breakage; a worn edge creates a hardened entrance.
Why support the feather edge?
The nest converts a bending problem into a light cutting problem and makes alternating passes repeatable.


