Related tooling references: AZ31B Magnesium Camera Heat Sink Housing CNC Tool Selection for Thin Cooling Fins and Lens Boss Pocket and Tungsten Heavy Alloy Collimator Insert CNC Tool Selection for Stepped Slit Aperture and Dovetail Rail.
English: 6061-T6 Dovetail Stage Tooling for Slide Rail and Adjustment Slots
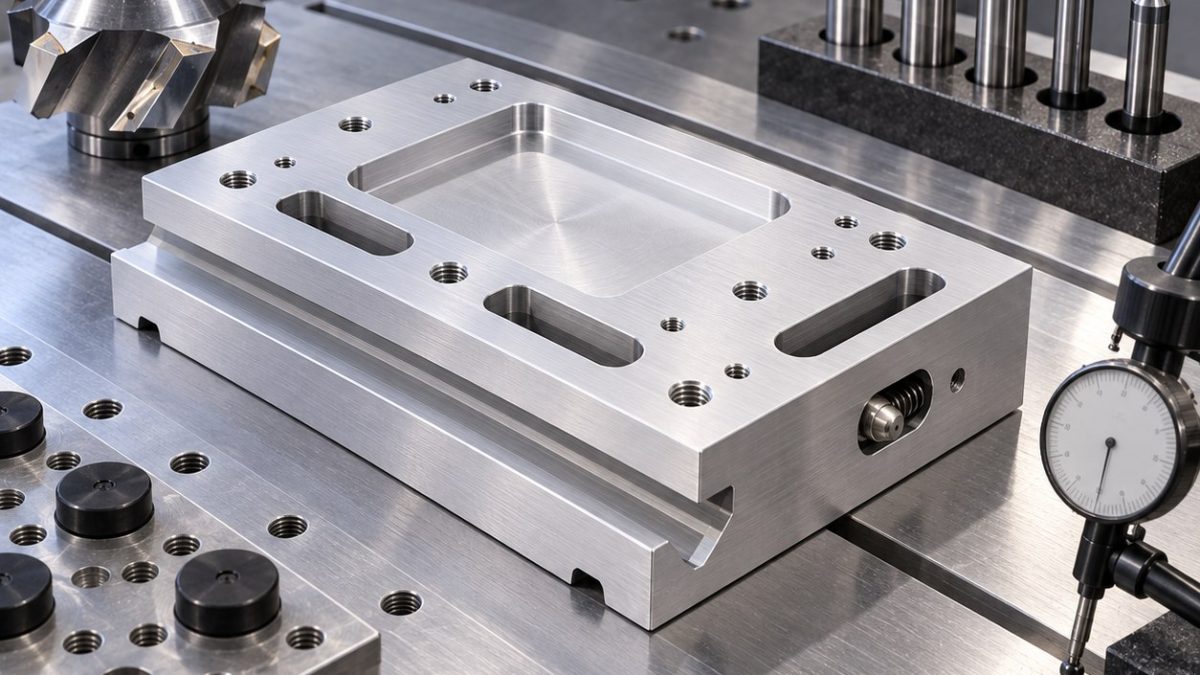
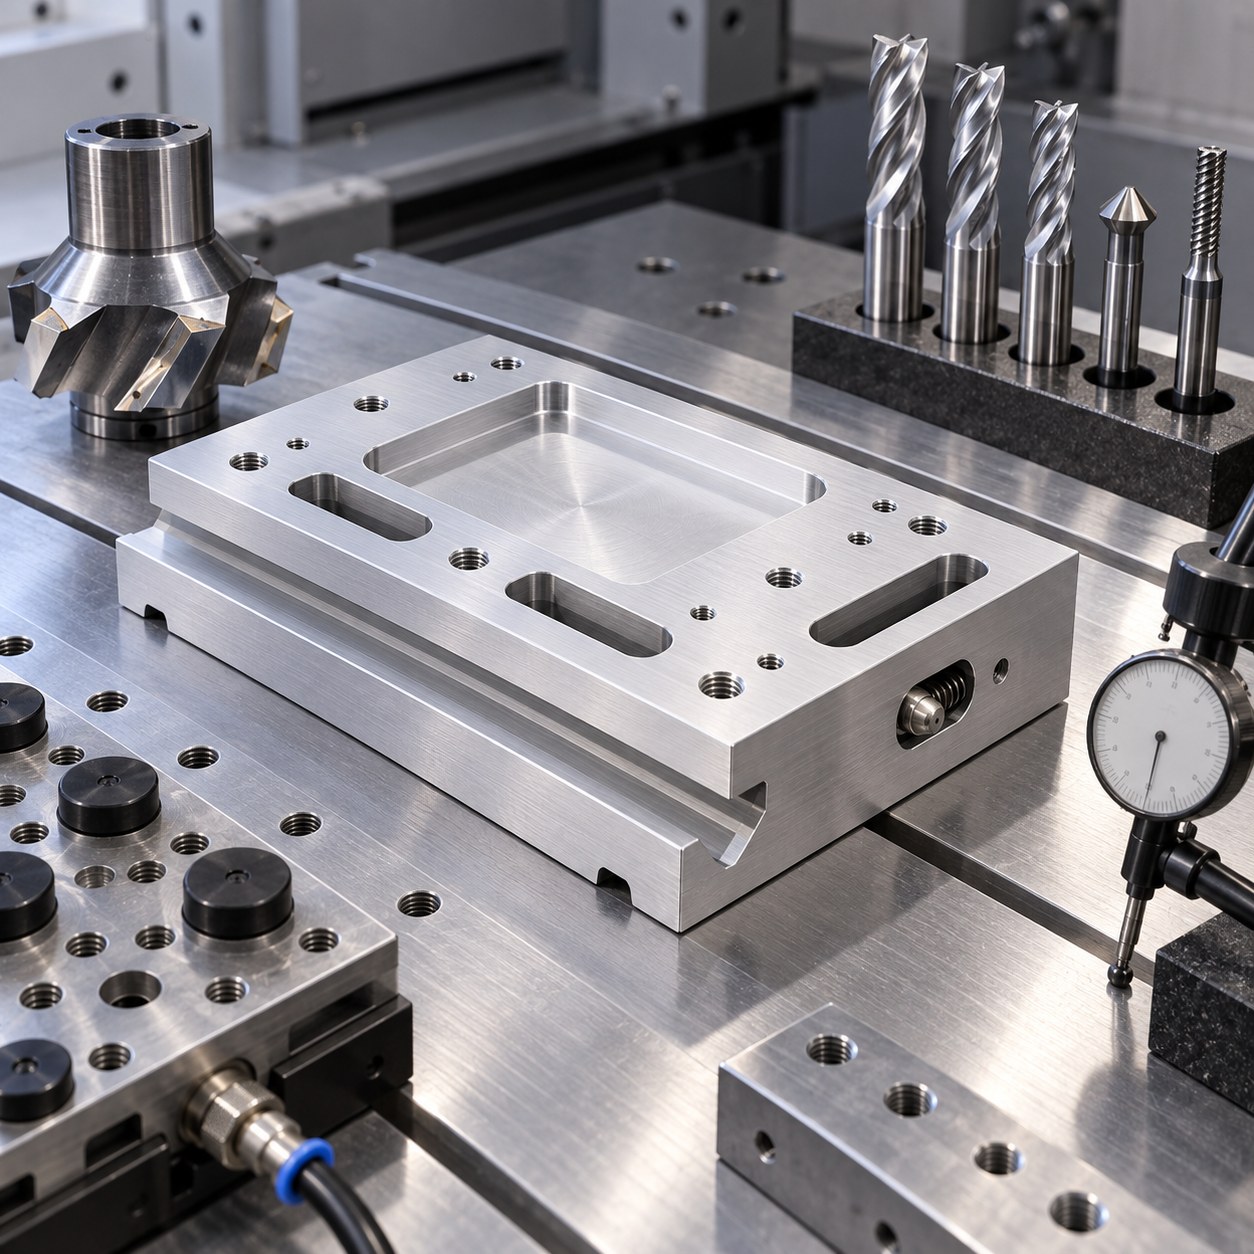
This 6061-T6 optical stage case answers how to tool a dovetail translation base where slide feel, adjustment slots and anodize-prep finish matter together. The dovetail cutter is selected after roughing strategy, not as an isolated form tool.
Optical stage features and aluminum tooling
| Stage feature | Tool and holder | Tolerance reason |
|---|---|---|
| Dovetail slide rail | Carbide dovetail form cutter in shrink holder after 6 mm rough slot | Controls slide angle; a ball tool interpolation path is rejected. |
| Adjustment slots | 5 mm 3-flute polished aluminum end mill | Maintains wall finish before anodizing. |
| Anti-reflection pocket | 10 mm high-helix rougher and 6 mm finishing end mill | Leaves a flat matte-prep floor without chatter. |
| M3 threaded holes | Carbide drill and thread mill | Thread milling prevents broken taps in thin bosses. |
| Spring plunger bore | Boring bar after pilot drilling | Holds plunger alignment better than drill-only sizing. |
Dovetail-first process plan
The datum underside is faced, rough slots are opened, and the dovetail rail is formed before adjustment slots remove stiffness. The anti-reflection pocket is finished with a shallow raster pass, then M3 holes and plunger bore are cut from the same datum.
6061 finish and anodize-prep controls
6061-T6 cuts easily, but optical hardware rejects chatter, burrs and anodize streaks. Polished 3-flute aluminum tools, mist or air chip clearing, and climb finishing keep edges consistent. A dull chamfer tool is replaced before it rolls the slot lip.
Slide rail inspection plan
Inspection measures dovetail angle, rail straightness, slot location, threaded-hole fit, plunger bore alignment and visual finish before anodizing.
6061 stage FAQ
Why form the dovetail before adjustment slots?
Slots reduce stiffness, so the precision rail is finished while the base is stronger.
Can a ball mill make the dovetail?
It can approximate, but a form cutter gives a cleaner slide angle.
What matters before anodizing?
Uniform tool marks, burr-free slots and clean chamfers.


