Related tooling references: AZ31B Magnesium Camera Heat Sink Housing CNC Tool Selection for Thin Cooling Fins and Lens Boss Pocket and Tungsten Heavy Alloy Collimator Insert CNC Tool Selection for Stepped Slit Aperture and Dovetail Rail.
English: UHMWPE Guide Rail Tooling for Curved Pocket and T-Slot Groove
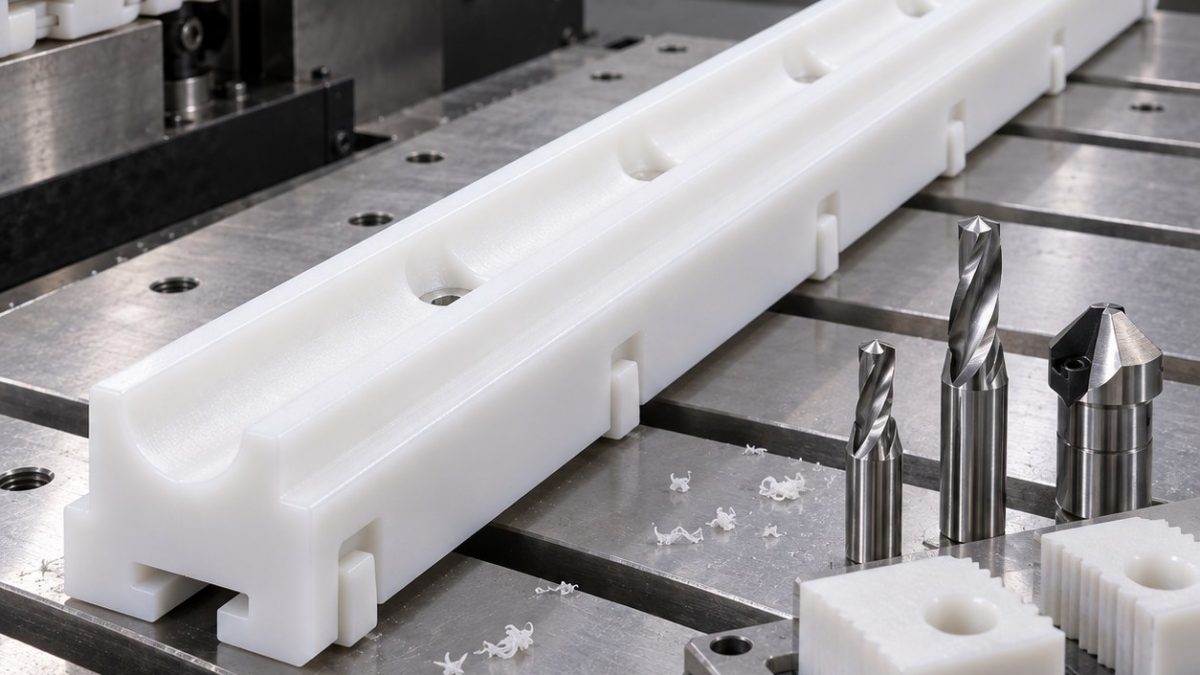
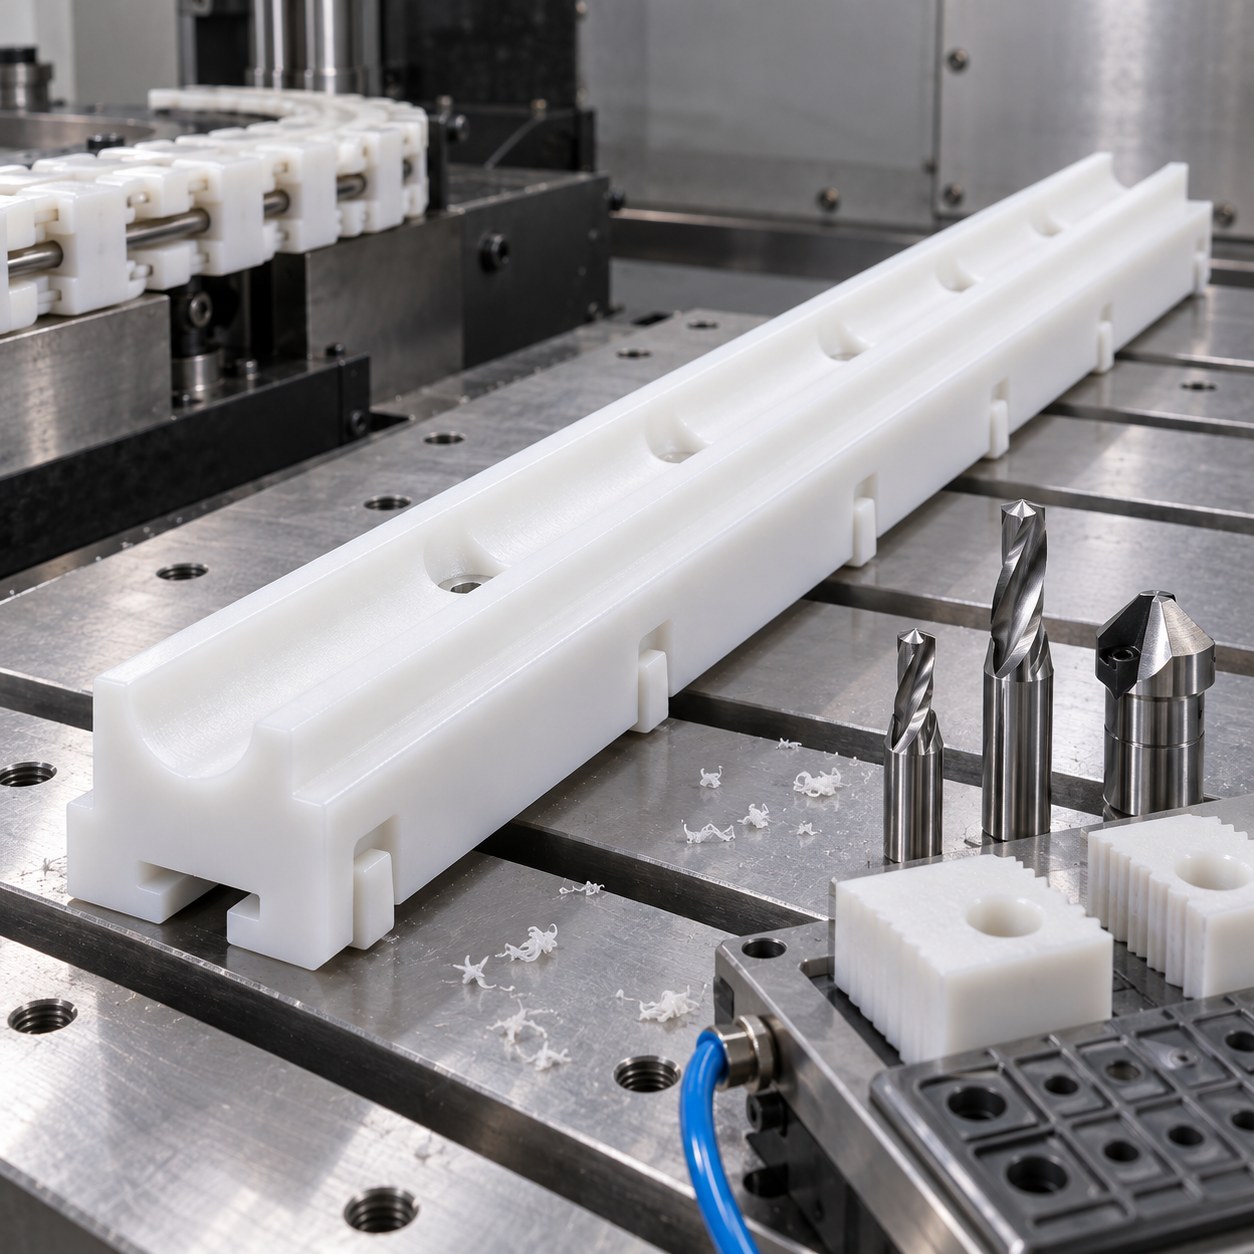
This UHMWPE guide rail case focuses on a long plastic wear part where a curved chain pocket, T-slot groove and flexible tabs must stay straight after machining. Tooling is chosen to shear soft polymer and support the rail before release.
Guide rail features and plastic cutters
| Rail feature | Tool and support | Why it works |
|---|---|---|
| Curved chain pocket | 8 mm polished single-flute carbide router in vacuum support | Large flute clears soft chips and follows the chain radius cleanly. |
| T-slot mounting groove | T-slot carbide cutter after rough slotting with 5 mm O-flute mill | Separates chip evacuation from final undercut geometry. |
| Countersunk long slots | Carbide drill, slot mill and PCD chamfer tool | Controls screw travel and removes feather burrs. |
| Oil relief notches | 3 mm polished carbide end mill | Cuts notches without smearing the rail edge. |
| Snap tabs | 2 mm polished finisher with low radial engagement | Protects flexible tabs from whitening or bending. |
Long rail machining sequence
Mounting slots and rough chain pockets are opened while the blank still has side stock. The T-slot is cut only after chips can escape, snap tabs are finished with the rail supported, and the final outside pass is light.
UHMWPE chip and burr control
UHMWPE makes stringy chips and feather burrs. Polished single-flute tools, air, vacuum support and sharp PCD chamfers prevent smearing. A metal rougher is rejected because it heats and pushes the plastic instead of cutting it.
Fit and straightness inspection
Inspection checks rail straightness after unclamping, slot travel, chain-pocket radius, snap-tab flexibility and burrs along the T-slot under angled light.
UHMWPE tooling FAQ
Why not use a normal metal rougher on UHMWPE?
It pushes and heats soft plastic, causing feather burrs and waviness.
When is the T-slot cut?
After rough slotting creates chip space, before the rail is released.
How is straightness checked?
After unclamping, against a straightedge or CMM line along the chain path.


