Related tooling references: AZ31B Magnesium Camera Heat Sink Housing CNC Tool Selection for Thin Cooling Fins and Lens Boss Pocket and Tungsten Heavy Alloy Collimator Insert CNC Tool Selection for Stepped Slit Aperture and Dovetail Rail.
English: Inconel 718 Nozzle Ring Tooling for Angled Jet Holes and Pockets
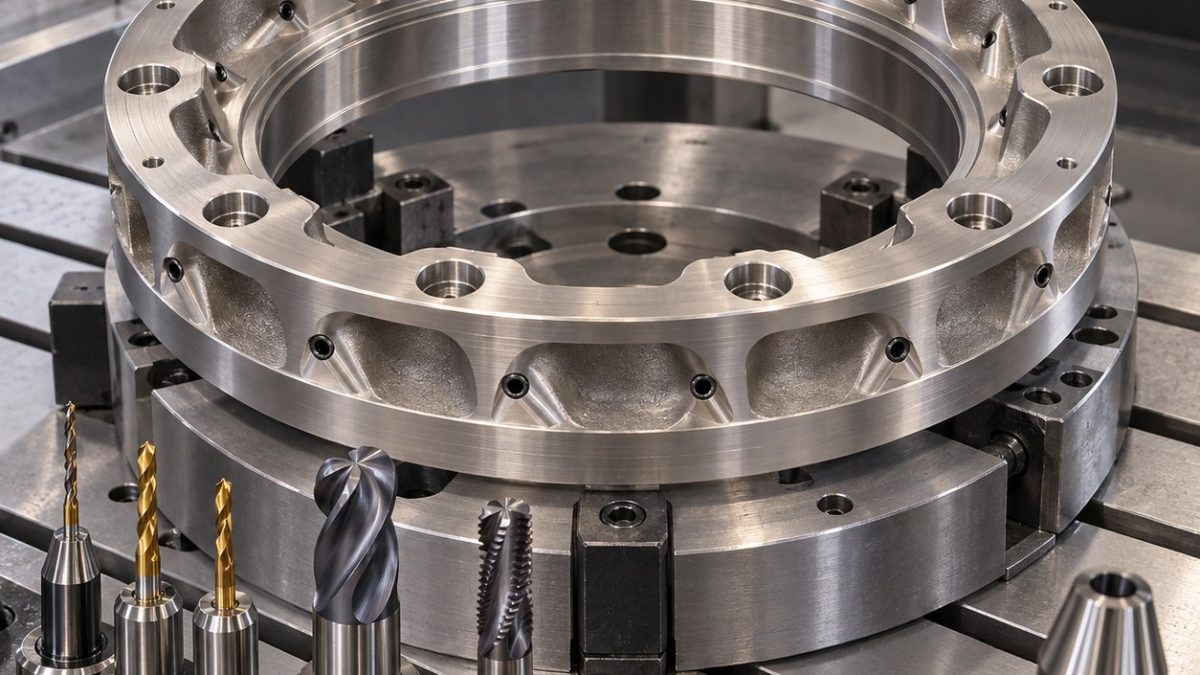
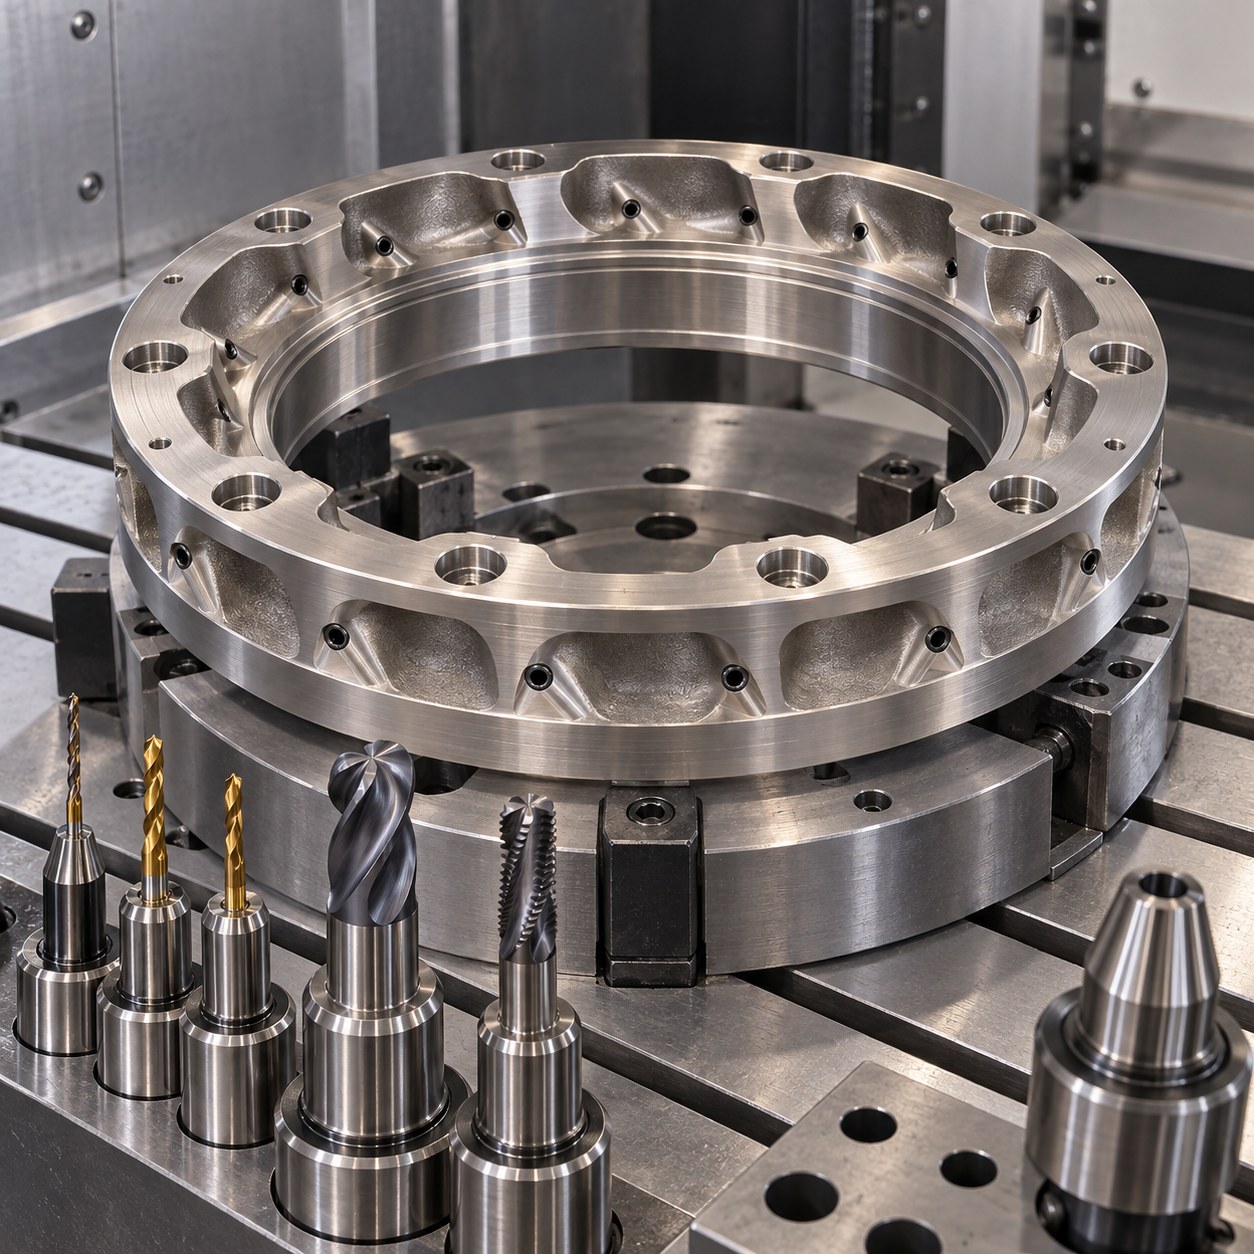
This Inconel 718 nozzle ring case answers how to choose tools when an annular drawing combines angled oil jets, scalloped pockets and a seal land. The key is not only hole size; it is preventing work-hardened burrs from blocking oil flow.
Ring drawing features translated into tools
| Drawing feature | Tool and holder | Decision reason |
|---|---|---|
| Angled micro oil holes | 0.7 mm TiAlN carbide drill with guide bushing and peck cycle | Prevents walking on the curved ring face; EDM is rejected for recast in oil jets. |
| Scalloped pockets | 6 mm variable-helix coated carbide rougher and 4 mm ball finisher | Balances stock removal and blends pocket roots without rubbing. |
| Inner seal land | 12 mm wiper end mill in hydraulic holder | Finishes the sealing band after heat-generating roughing is complete. |
| Bolt counterbores | Carbide drill, piloted counterbore and 90° chamfer mill | Keeps seating faces separate from jet-hole burr control. |
| Threaded ports | Single-point carbide thread mill | Avoids tap chip packing in nickel alloy. |
Rotary process sequence
The ring is clamped on a rotary fixture, datum faces are skimmed, pockets are rough-milled symmetrically, and the seal land is left for a cool finishing pass. Angled holes are drilled after pocket stress is released but before final deburring access is lost.
Nickel alloy burr and tool-life control
Inconel 718 punishes rubbing. Coated carbide, short pecks, high-pressure coolant, shrink holders and conservative tool-life limits keep the edge cutting. Exit burr color and hole pin drag trigger tool replacement.
Oil-flow inspection plan
Inspection covers oil-hole pin entry, borescope review, seal-land roundness, counterbore seating and a simple flow balance check around the ring.
Inconel nozzle FAQ
Why drill angled oil holes after pocket roughing?
Pocketing releases local stress, but drilling still needs access for burr control.
What wears first in Inconel 718?
The micro drill edge at hole exit and the pocket finisher at rubbed roots.
Why use a rotary fixture?
It keeps jet-hole angles and ring datums consistent without repeated reclamping.


