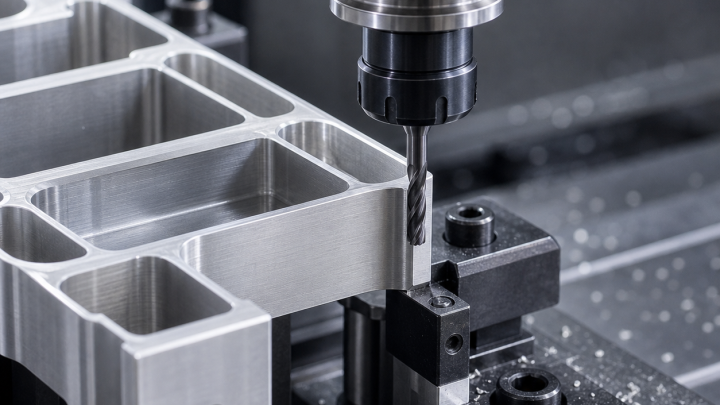
薄壁 CNC 铣削毛刺控制:刀具、支撑与精加工顺序
Thin-Wall CNC Milling Burr Control: Tool Selection, Support and Finishing Sequence
通过锋利硬质合金铣刀、工艺支撑和分阶段精铣,控制薄壁零件翻边与出口毛刺而不推弯壁面。
Thin-Wall CNC Milling Burr Control: Tool Selection, Support and Finishing Sequence
通过锋利硬质合金铣刀、工艺支撑和分阶段精铣,控制薄壁零件翻边与出口毛刺而不推弯壁面。
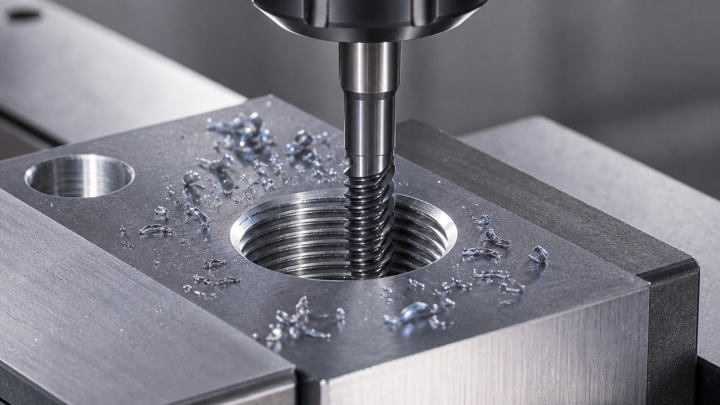
CNC Thread Milling: When to Use Carbide Thread Mills Instead of Taps
CNC 螺纹铣削通过硬质合金螺纹铣刀和圆弧插补加工内螺纹或外螺纹。
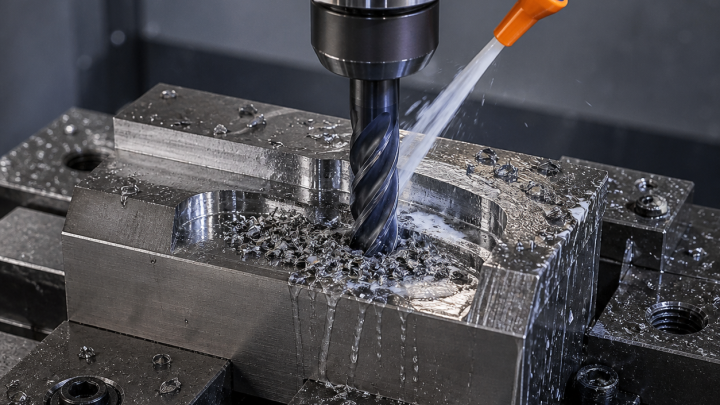
Nickel Alloy CNC Tooling Hub: Select Carbide Tools by Alloy, Feature and Failure Mode
按Inconel、Hastelloy、Monel和Incoloy的图纸特征、可达性、热量、沟槽磨损与检测风险选择铣、钻、镗、切槽和精加工刀具。
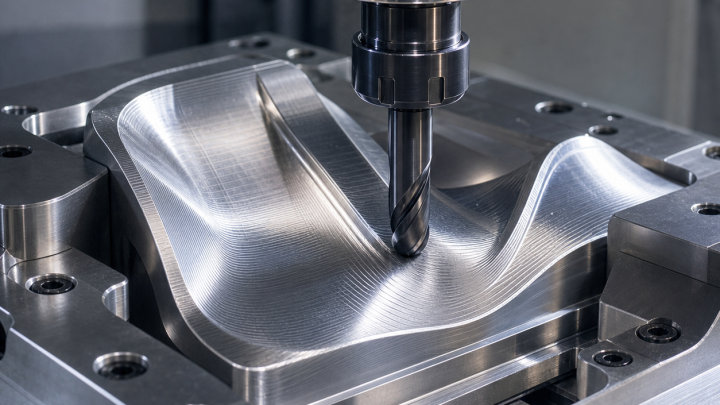
3D Contour CNC Machining: Ball Nose End Mill Step-Over and Surface Finish Control
3D 曲面 CNC 加工的表面效果,很大程度取决于球头铣刀半径、横向步距和目标粗糙度之间的关系。
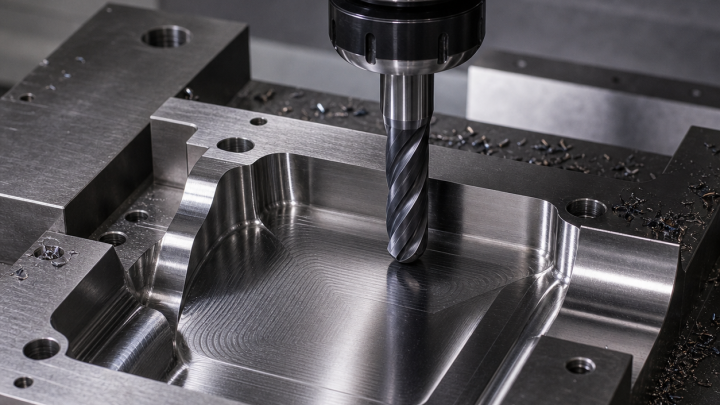
Hard Milling Hardened Steel: Finishing Strategies for Carbide Ball Nose End Mills
硬化钢硬铣常用于模具制造,对加工稳定性要求很高。
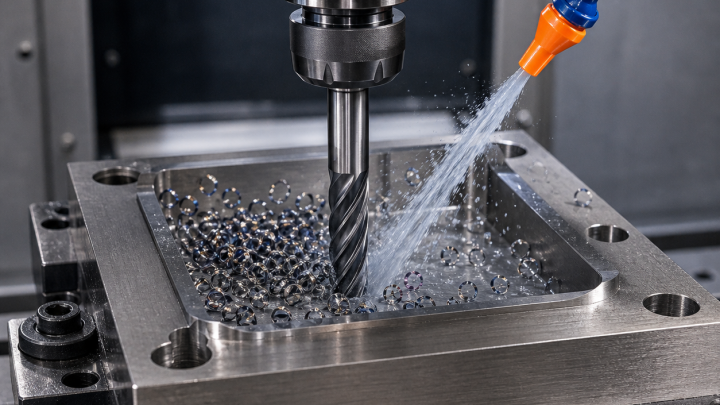
Titanium Alloy CNC Milling Tool Selection for Heat Control and Carbide End Mill Life
针对Ti-6Al-4V深型腔、薄筋、内圆角与精密孔选择粗精铣刀和内冷钻,用接触时间、径向吃刀和排屑管理热量。
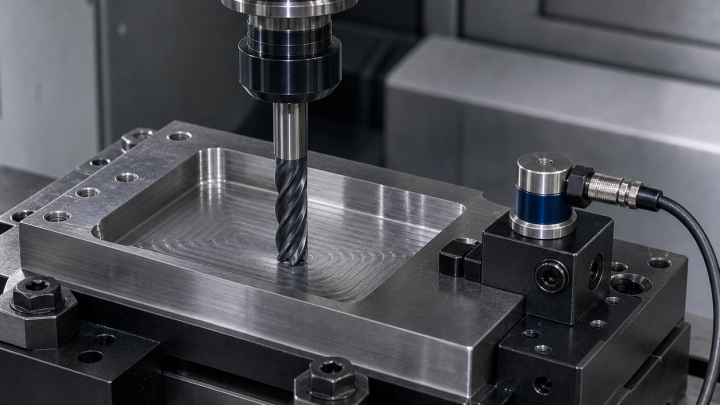
CNC Milling Chatter Control: Fixture Rigidity, Toolpath Choices and Stable Surface Finish
CNC 铣削颤振不仅是声音问题,而是刀具、工件、刀柄或机床结构在切削中发生振动的表现。
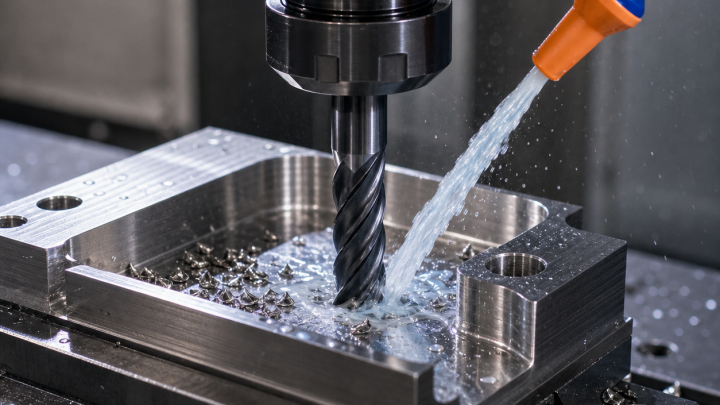
Stainless Steel CNC Milling Tool Selection to Prevent Work Hardening and Extend Tool Life
按型腔、满槽、薄壁、交叉孔和螺纹选择硬质合金刀具,避免停顿擦削,同时控制排屑、毛刺与寿命。
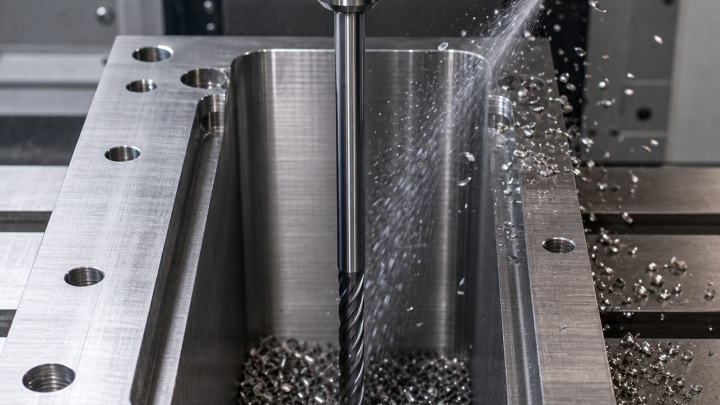
Deep Pocket Milling Tooling Hub: Reach, Chip Evacuation and Stock Control
按深宽比、最小圆角、刀柄通道、材料和精加工余量,选择分段硬质合金刀具、刀柄、冷却与检测方法。
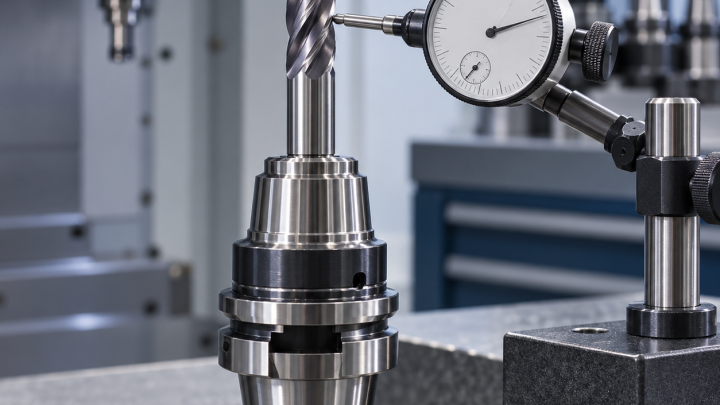
Low-Runout Tool Holders for Carbide End Mills: Measure, Diagnose and Correct TIR
在实际悬伸位置测量刀具总跳动,分离主轴、刀柄、夹头和刀具误差,并按粗铣、微小刀与精加工选择热缩、液压或精密夹头。
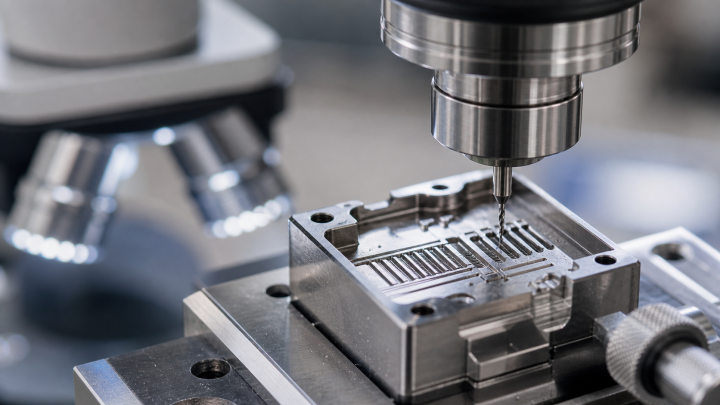
Micro End Mill Breakage Prevention: Runout, Reach, Chip Load and Toolpath
从图纸槽宽与深径比选择微径铣刀、刃数和刀柄,控制跳动、真实切屑厚度与排屑,并用尺寸和磨损趋势预防断刀。
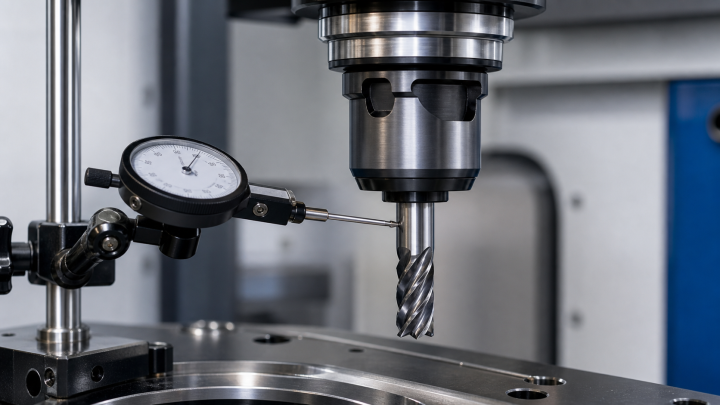
High-Speed Aluminum CNC Milling: Chip Evacuation and Surface Finish Strategies
铝合金高速 CNC 铣削的关键是让切屑快速离开切削区。