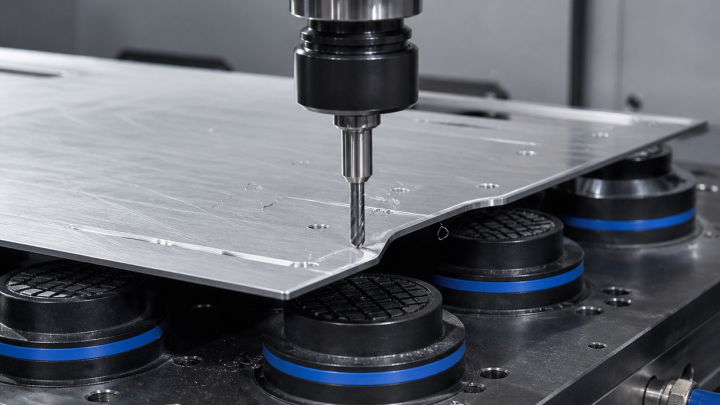
薄板 CNC 铣削为什么适合真空夹具
Vacuum Fixturing for Thin Sheet CNC Milling: Holding Parts Without Distortion
真空夹具适合薄板 CNC 铣削,因为它可以大面积支撑零件,而不需要在切削路径附近布置大量压板。
Vacuum Fixturing for Thin Sheet CNC Milling: Holding Parts Without Distortion
真空夹具适合薄板 CNC 铣削,因为它可以大面积支撑零件,而不需要在切削路径附近布置大量压板。
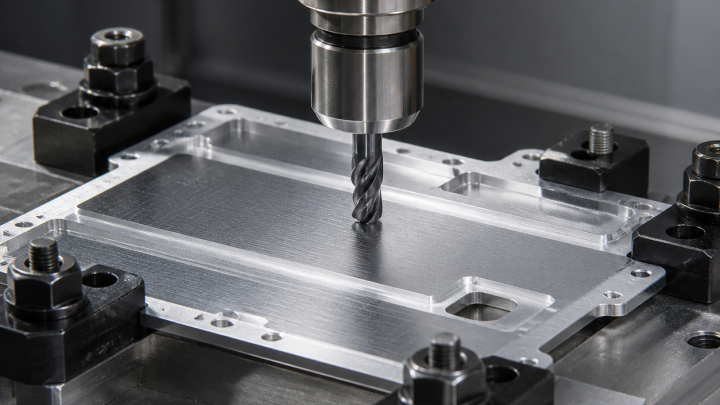
Residual Stress in CNC Milling: Reducing Distortion in Precision Metal Parts
CNC 铣削中的残余应力会在材料去除后释放,导致精密零件变形。
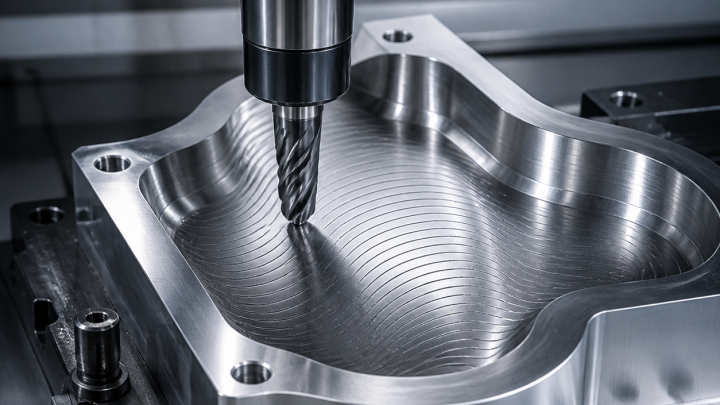
CNC Toolpath Smoothing: Reducing Machine Shock and Improving Surface Finish
CNC 刀路平滑可以减少突然加减速、尖角过载和刀具参与切削波动。
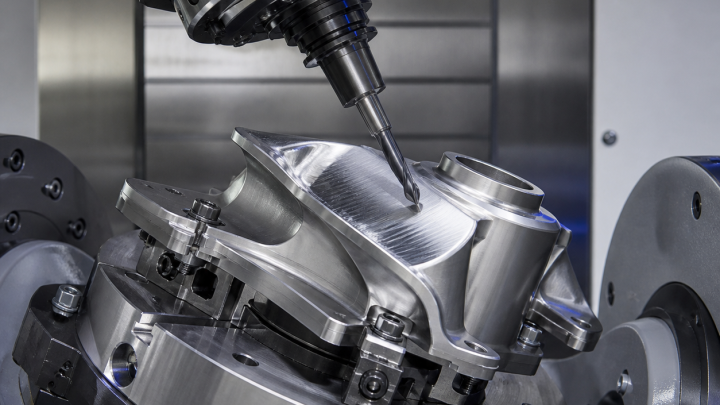
5-Axis CNC Milling Tool Orientation: Better Surface Finish on Complex Parts
5 轴 CNC 铣削允许刀轴相对零件表面倾斜。
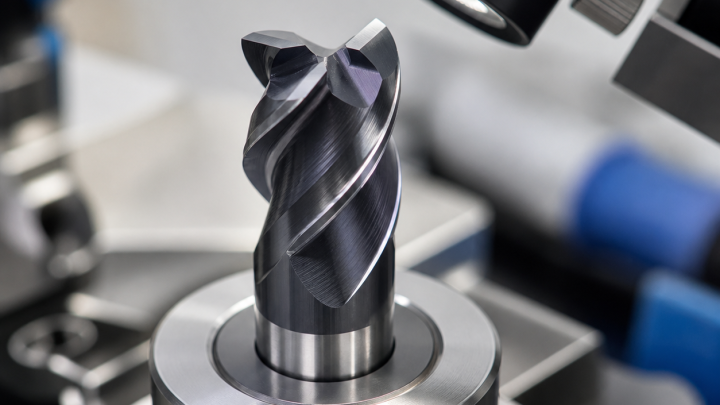
Carbide End Mill Edge Preparation: Micro Honing for Longer Tool Life
硬质合金铣刀刃口处理决定了涂层前或使用前的微观刃口形状。
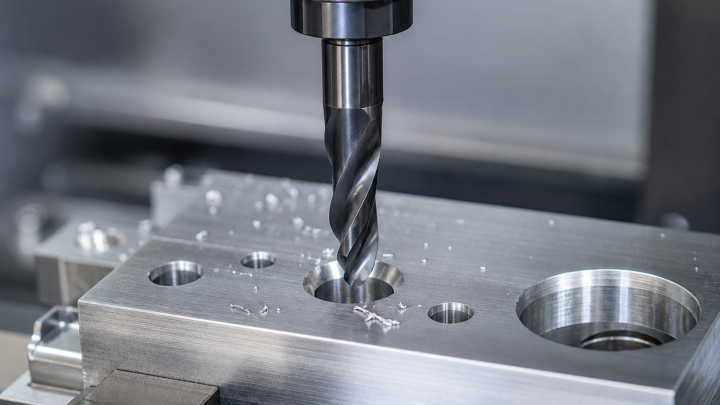
Drill Mill Selection for Spotting, Chamfering and Light Milling
根据定心、孔口倒角和短距离侧铣选择钻铣刀顶角、直径、刃形与悬伸,并明确何时必须改用专用刀具。
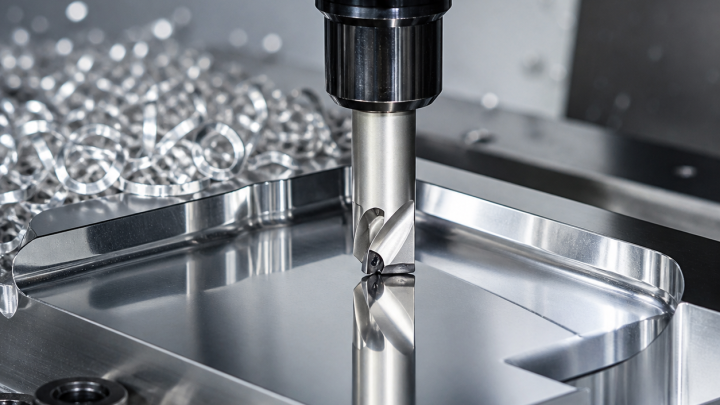
PCD Tool Selection for Aluminum Mirror Finishing and Abrasive Alloys
针对铝合金密封面、高硅铸铝和长寿命精加工,选择PCD刃形、前角、修光几何、冷却、刀柄和检测方法。
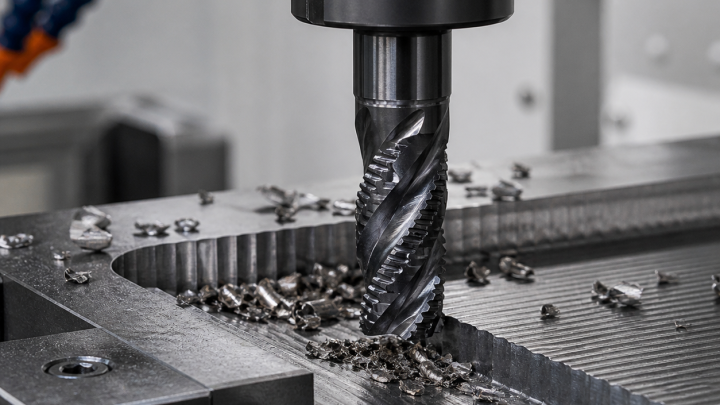
Roughing End Mills with Chipbreaker Geometry: Faster CNC Material Removal
粗皮铣刀通过波刃或断屑槽几何把切屑分成更小片段。
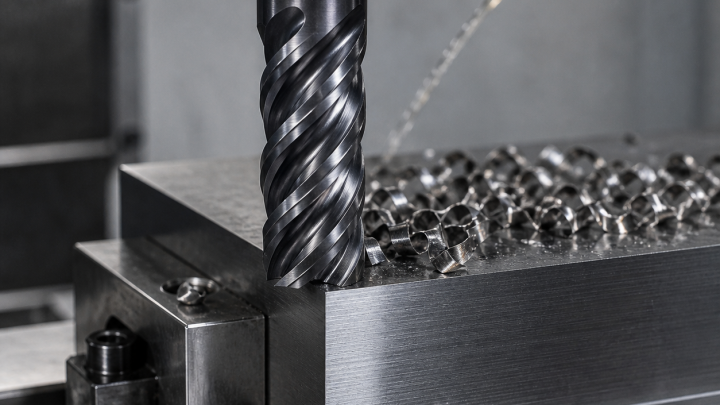
Variable Helix End Mills: Reducing Chatter in CNC Side Milling
变螺旋铣刀通过不同螺旋角设计来打散振动频率。在 CNC 侧铣中,这种几何可以减少谐振,提高切削稳定性。
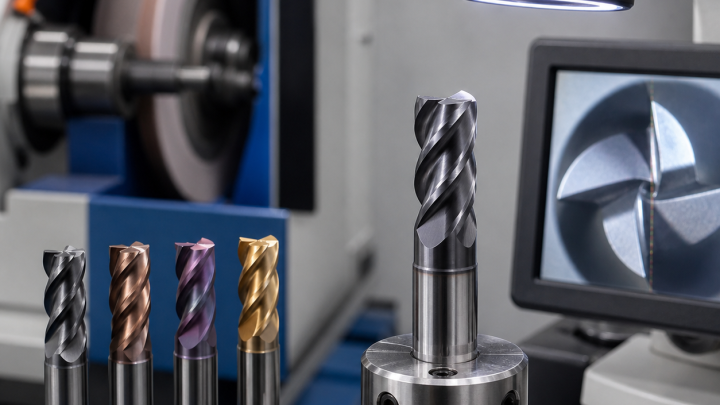
Carbide End Mill Regrinding and Recoating: When Tool Reconditioning Makes Sense
硬质合金铣刀修磨和重涂可以在刀具体状态良好时降低刀具成本。
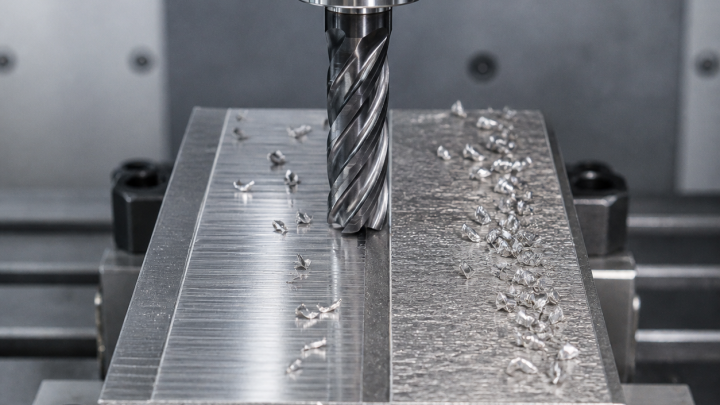
Climb vs Conventional Milling by Backlash, Burr Direction and Wall Deflection
根据机床反向间隙、材料硬皮、毛刺允许侧、薄壁支撑和公差选择铣削方向,而不是把顺铣当作固定答案。
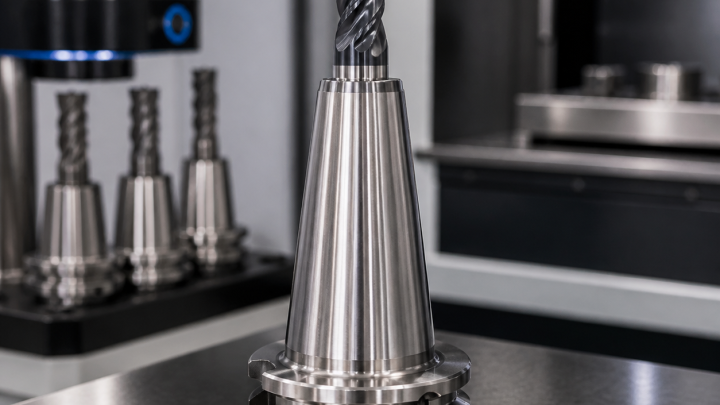
Shrink-Fit Tool Holders for CNC Milling: Runout Control and Carbide End Mill Stability
热缩刀柄通过热膨胀夹紧硬质合金铣刀,夹持力均匀且刚性好。